PROCESS AUTO-T
Automatic lathe turning
Small turned parts such as pins, bushings, nuts, inserts and fittings, made on automatic lathes.
- Ø20 × 100 mmLargest partSource: Max sizeMax sizeØ20 × 100 mmBasisDeclaredAs ofSourceSupplier information form (owner), 2026-11, automatic latheHow we label numbers
- 50Machines for this processSource: Machines for the processMachines for the process50BasisDocumentAs ofSourceSupplier information form: 50 machines listed for this processAsk for this recordHow we label numbers
HOW IT IS MADE
How a turned part is made
The bar spins while the tools turn each diameter, cut the chamfer, thread and groove, and part the shaft off.
Illustration
THE PART
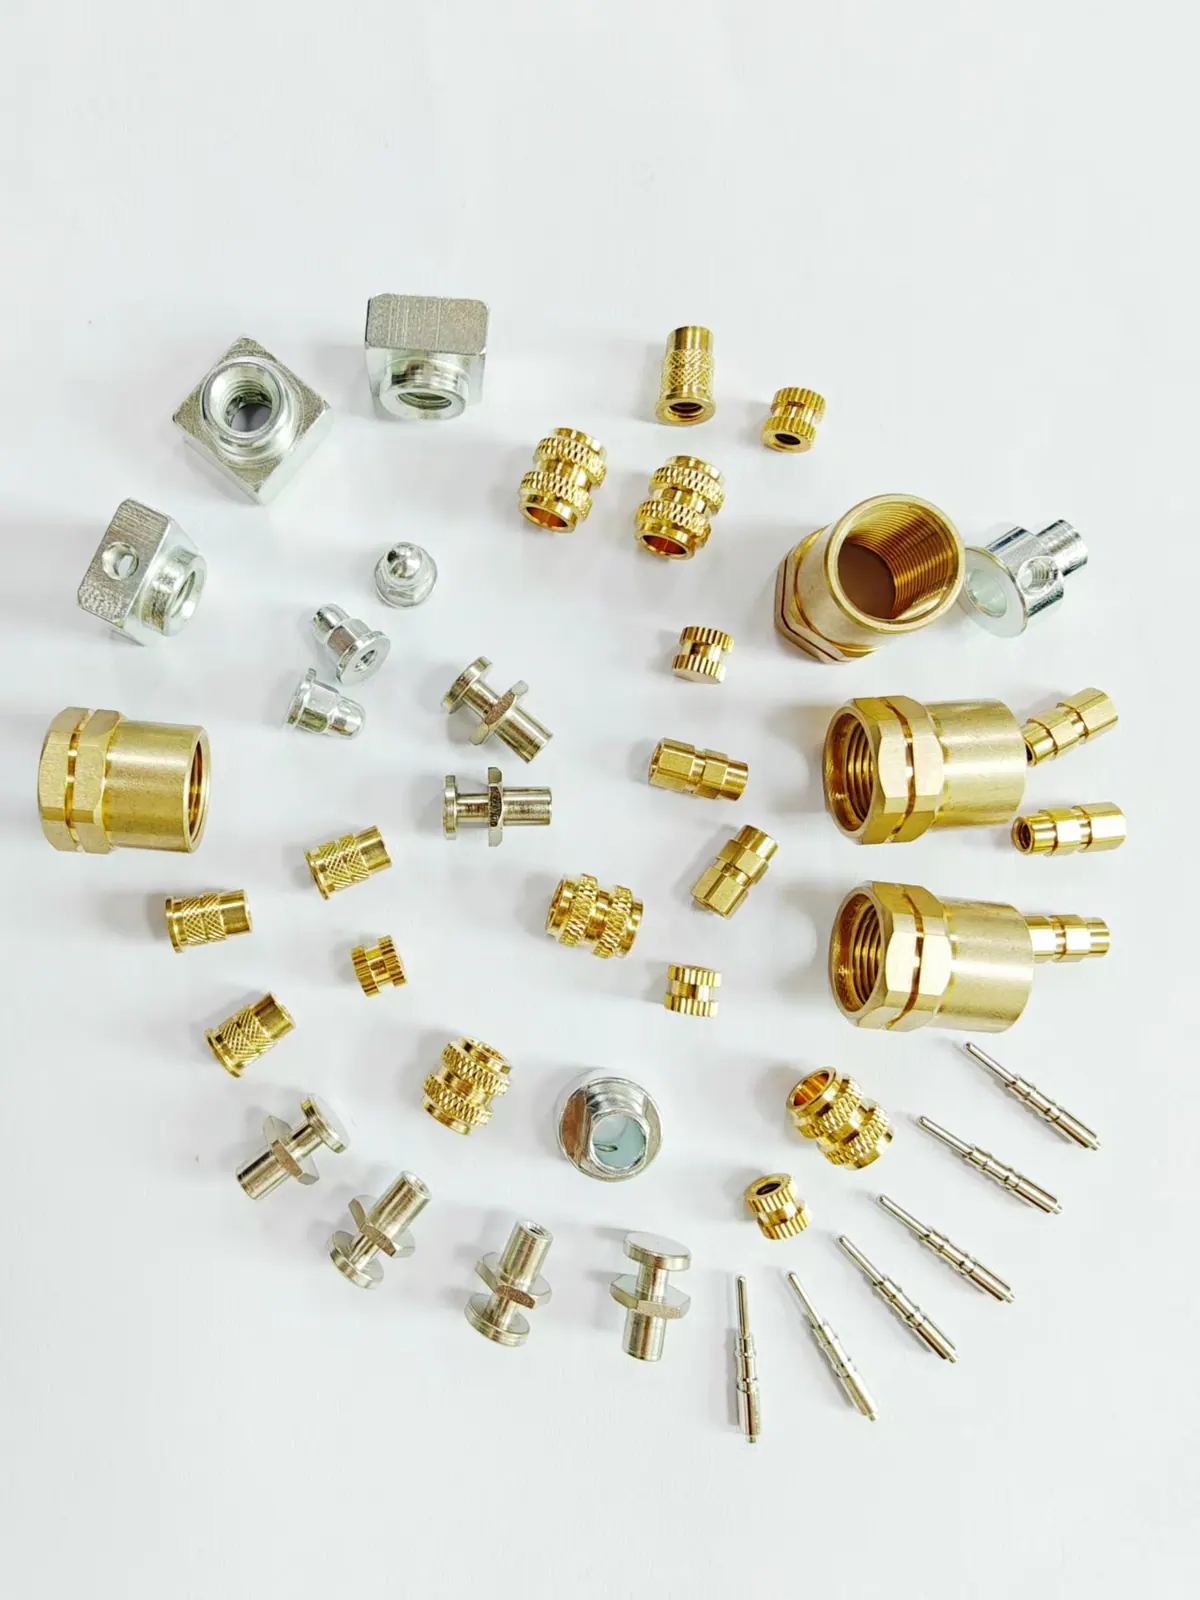
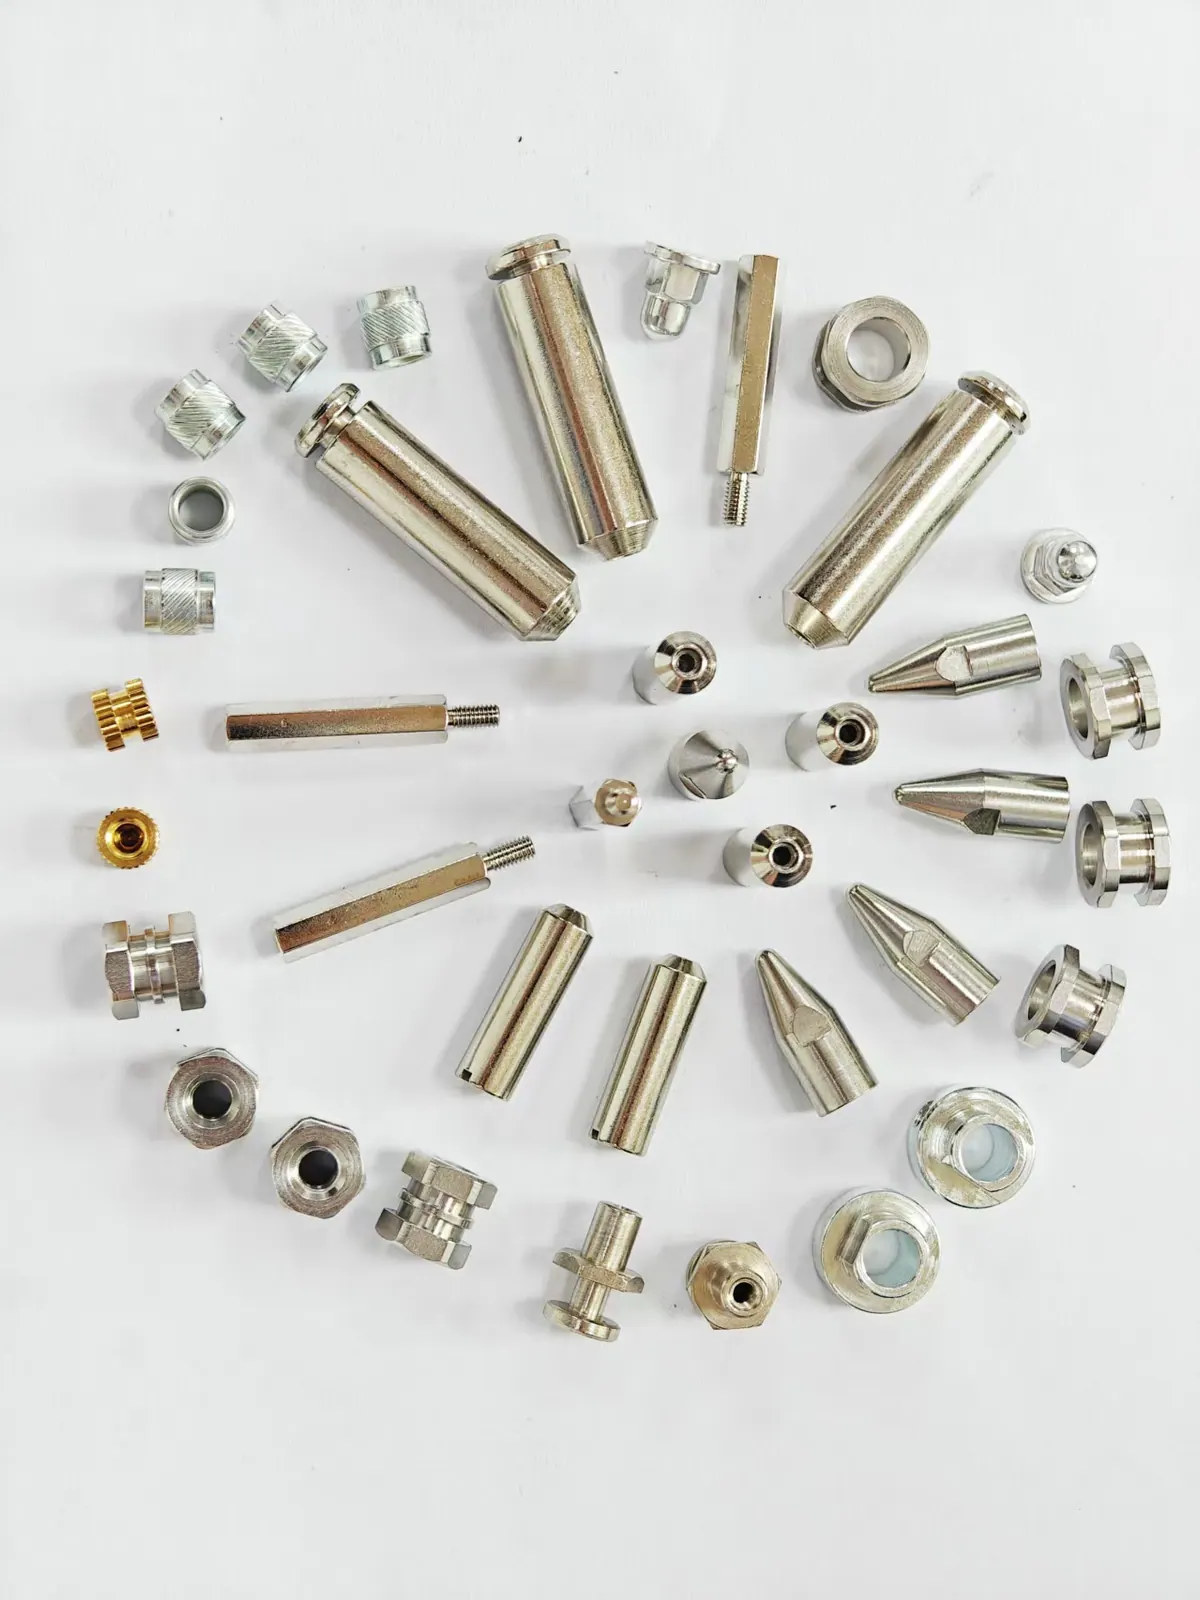
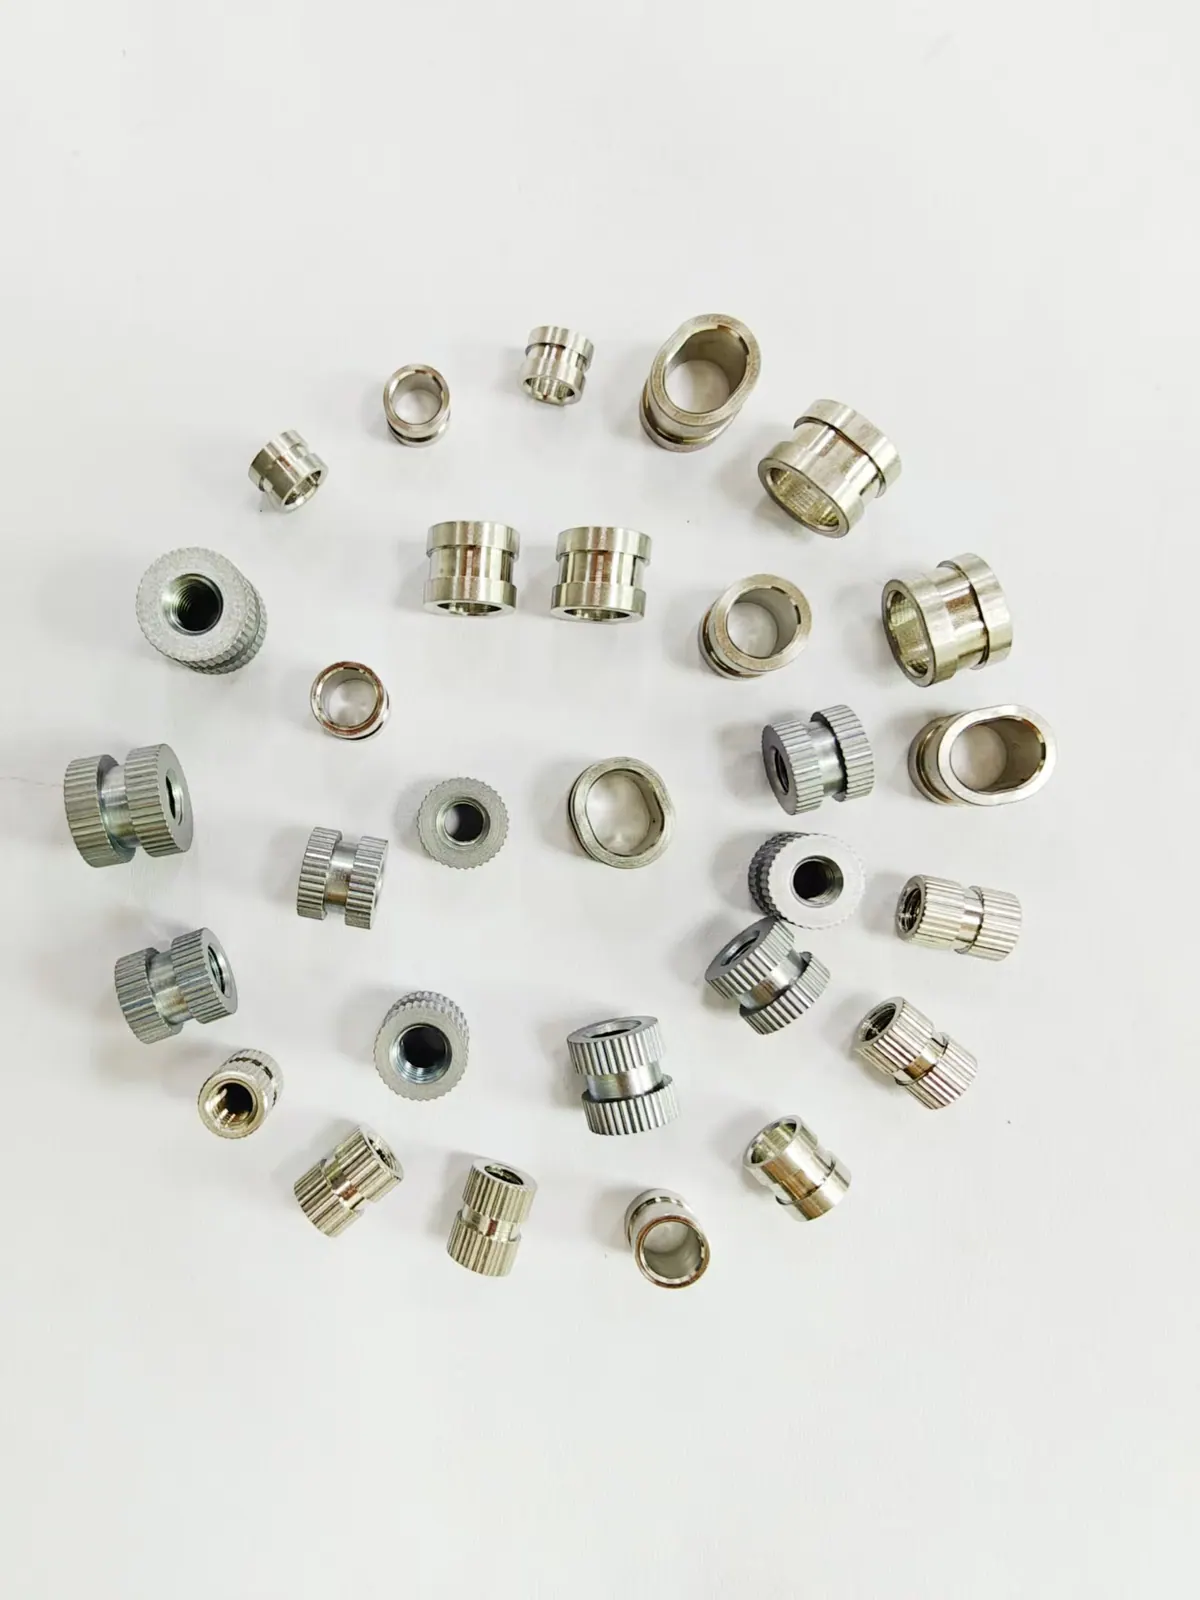
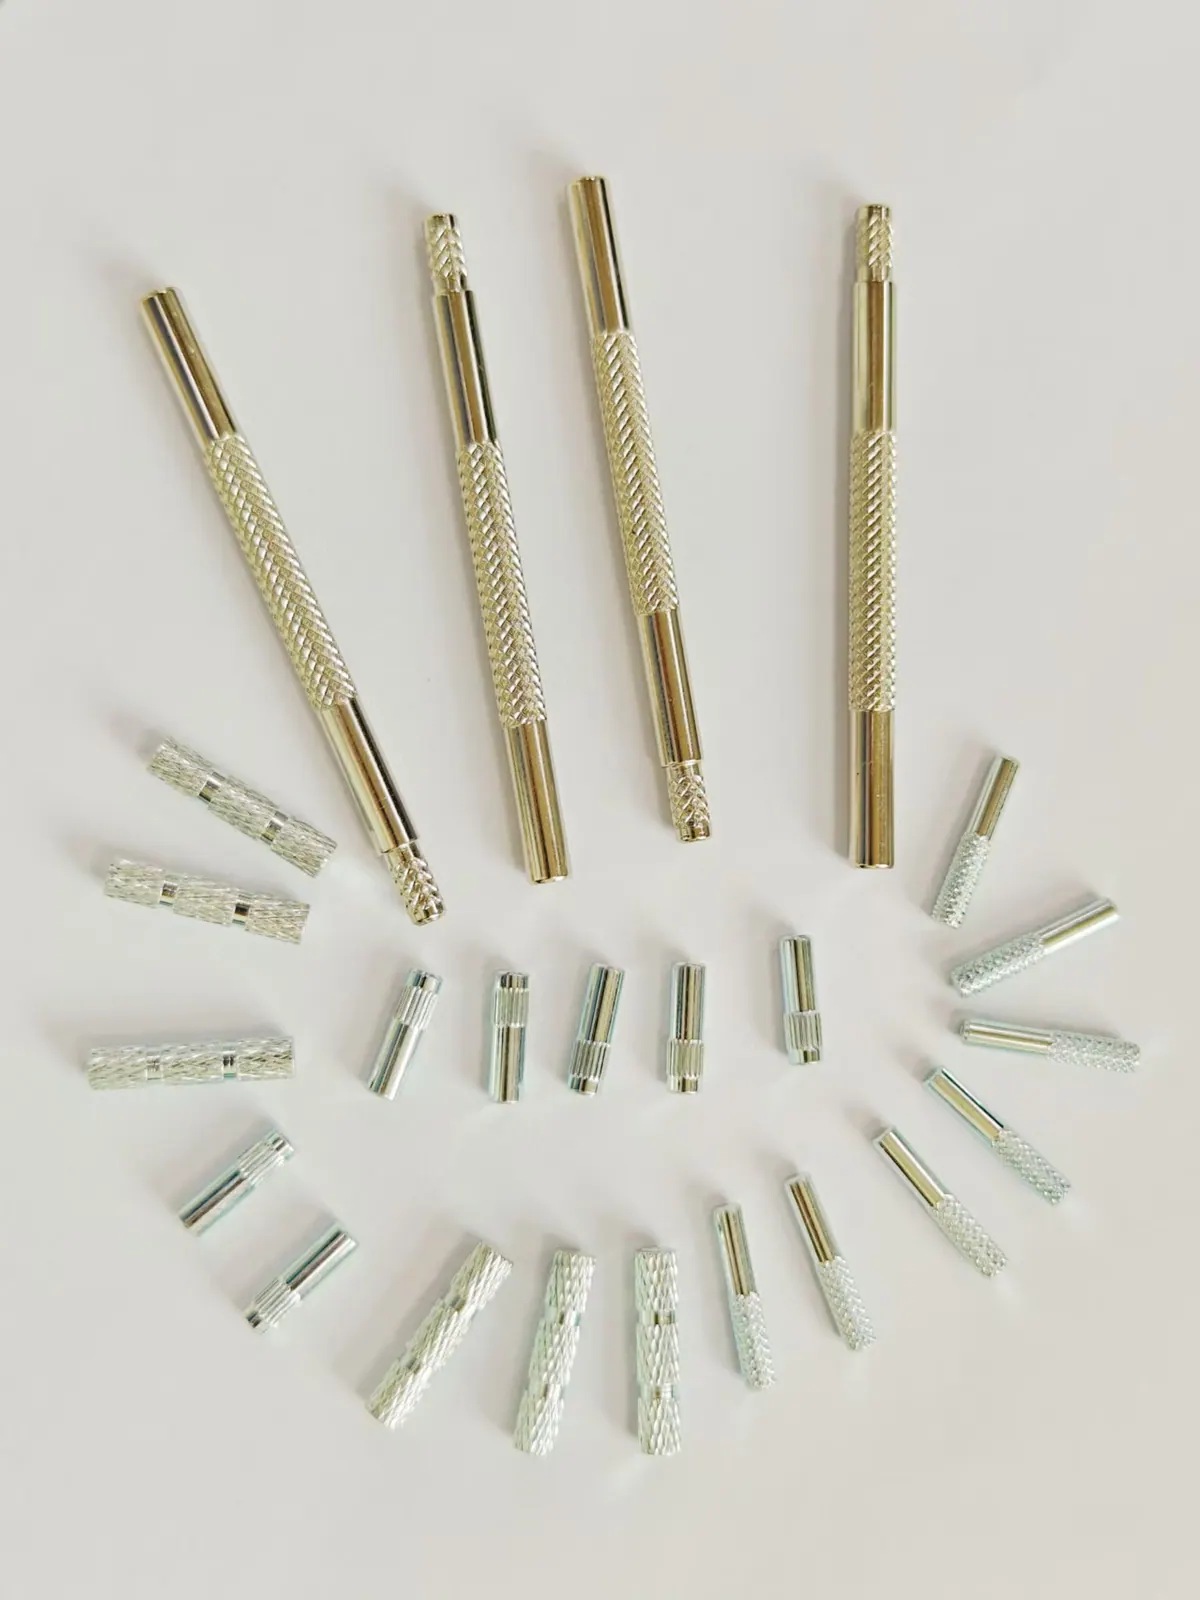
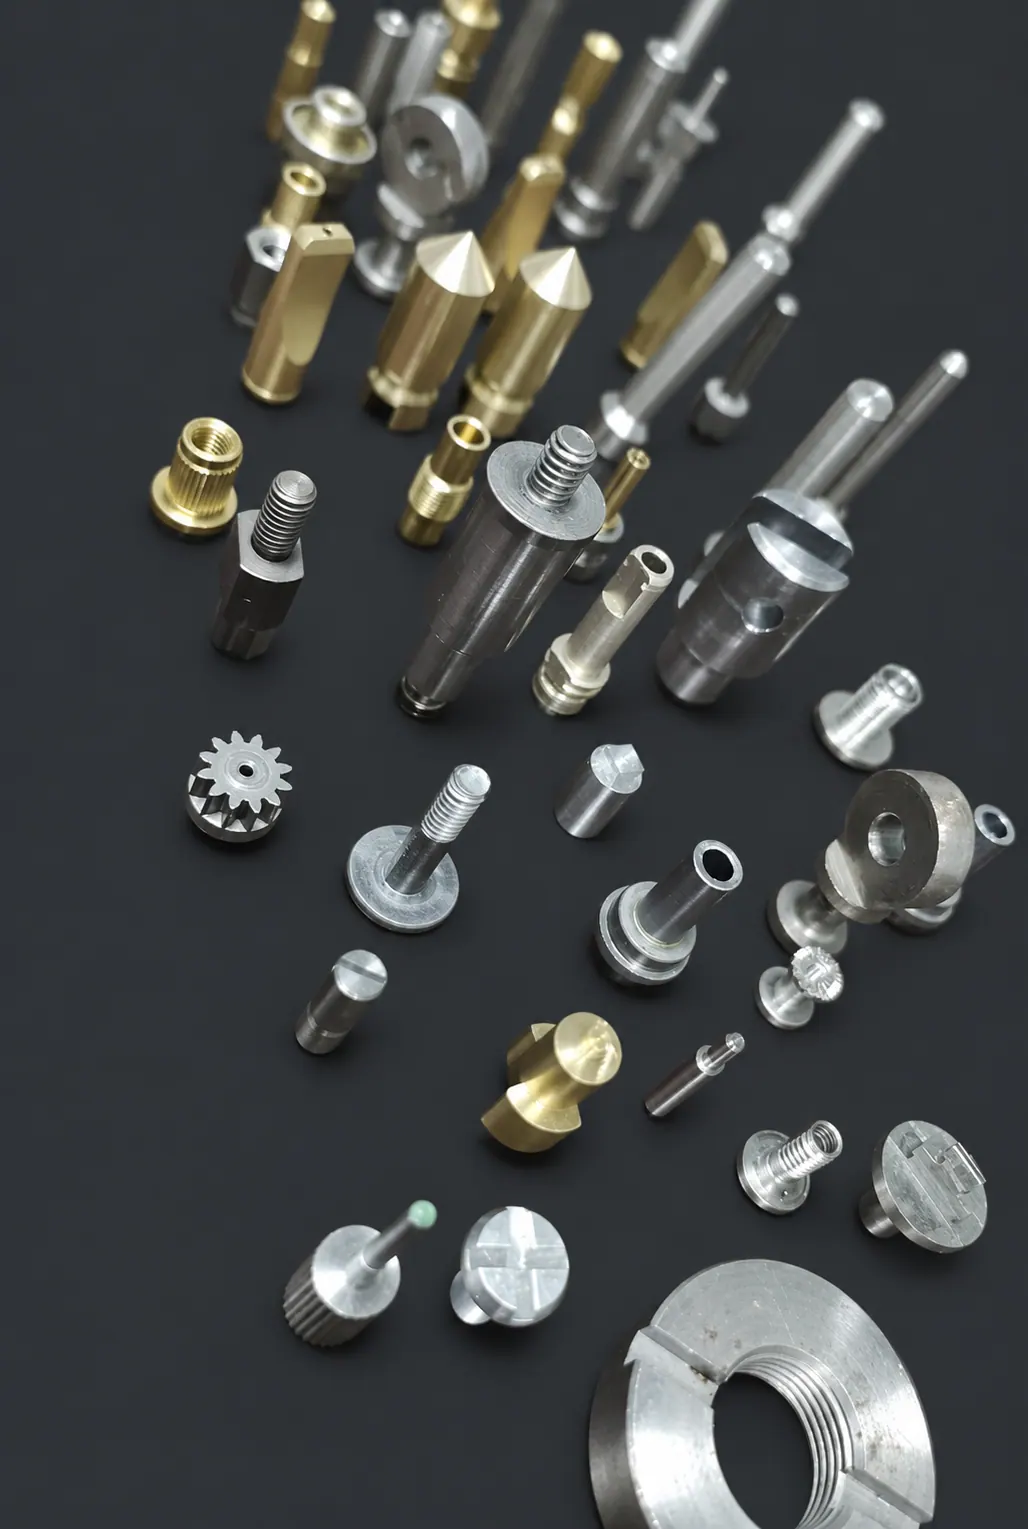
Sample parts
11 photographs
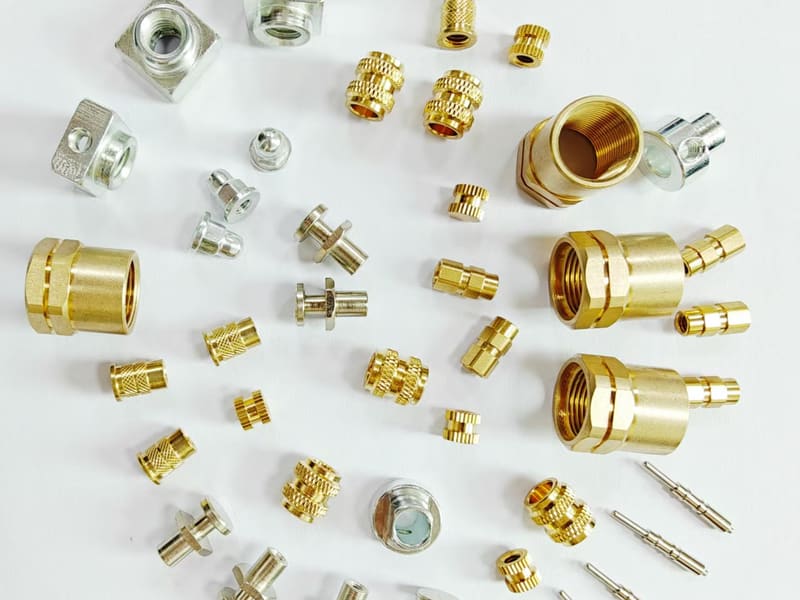
Knurled inserts, barbed hose fittings, nuts and pins 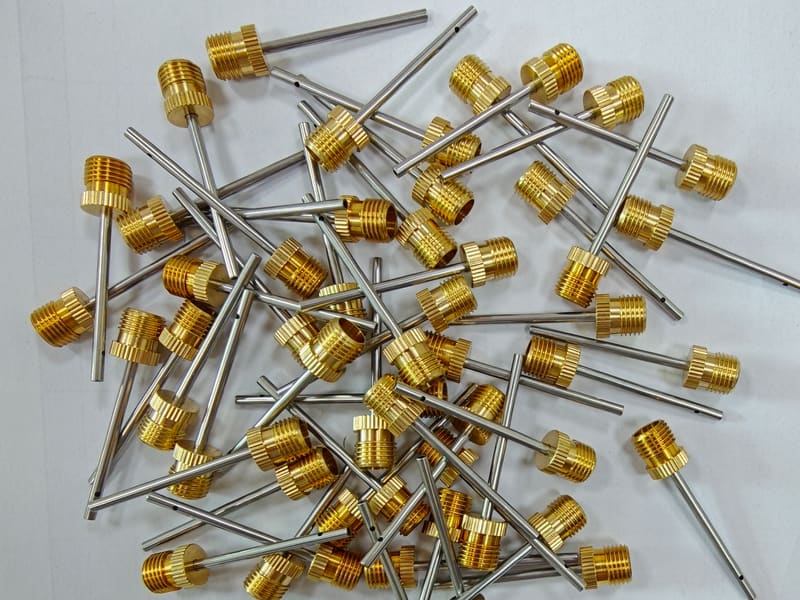
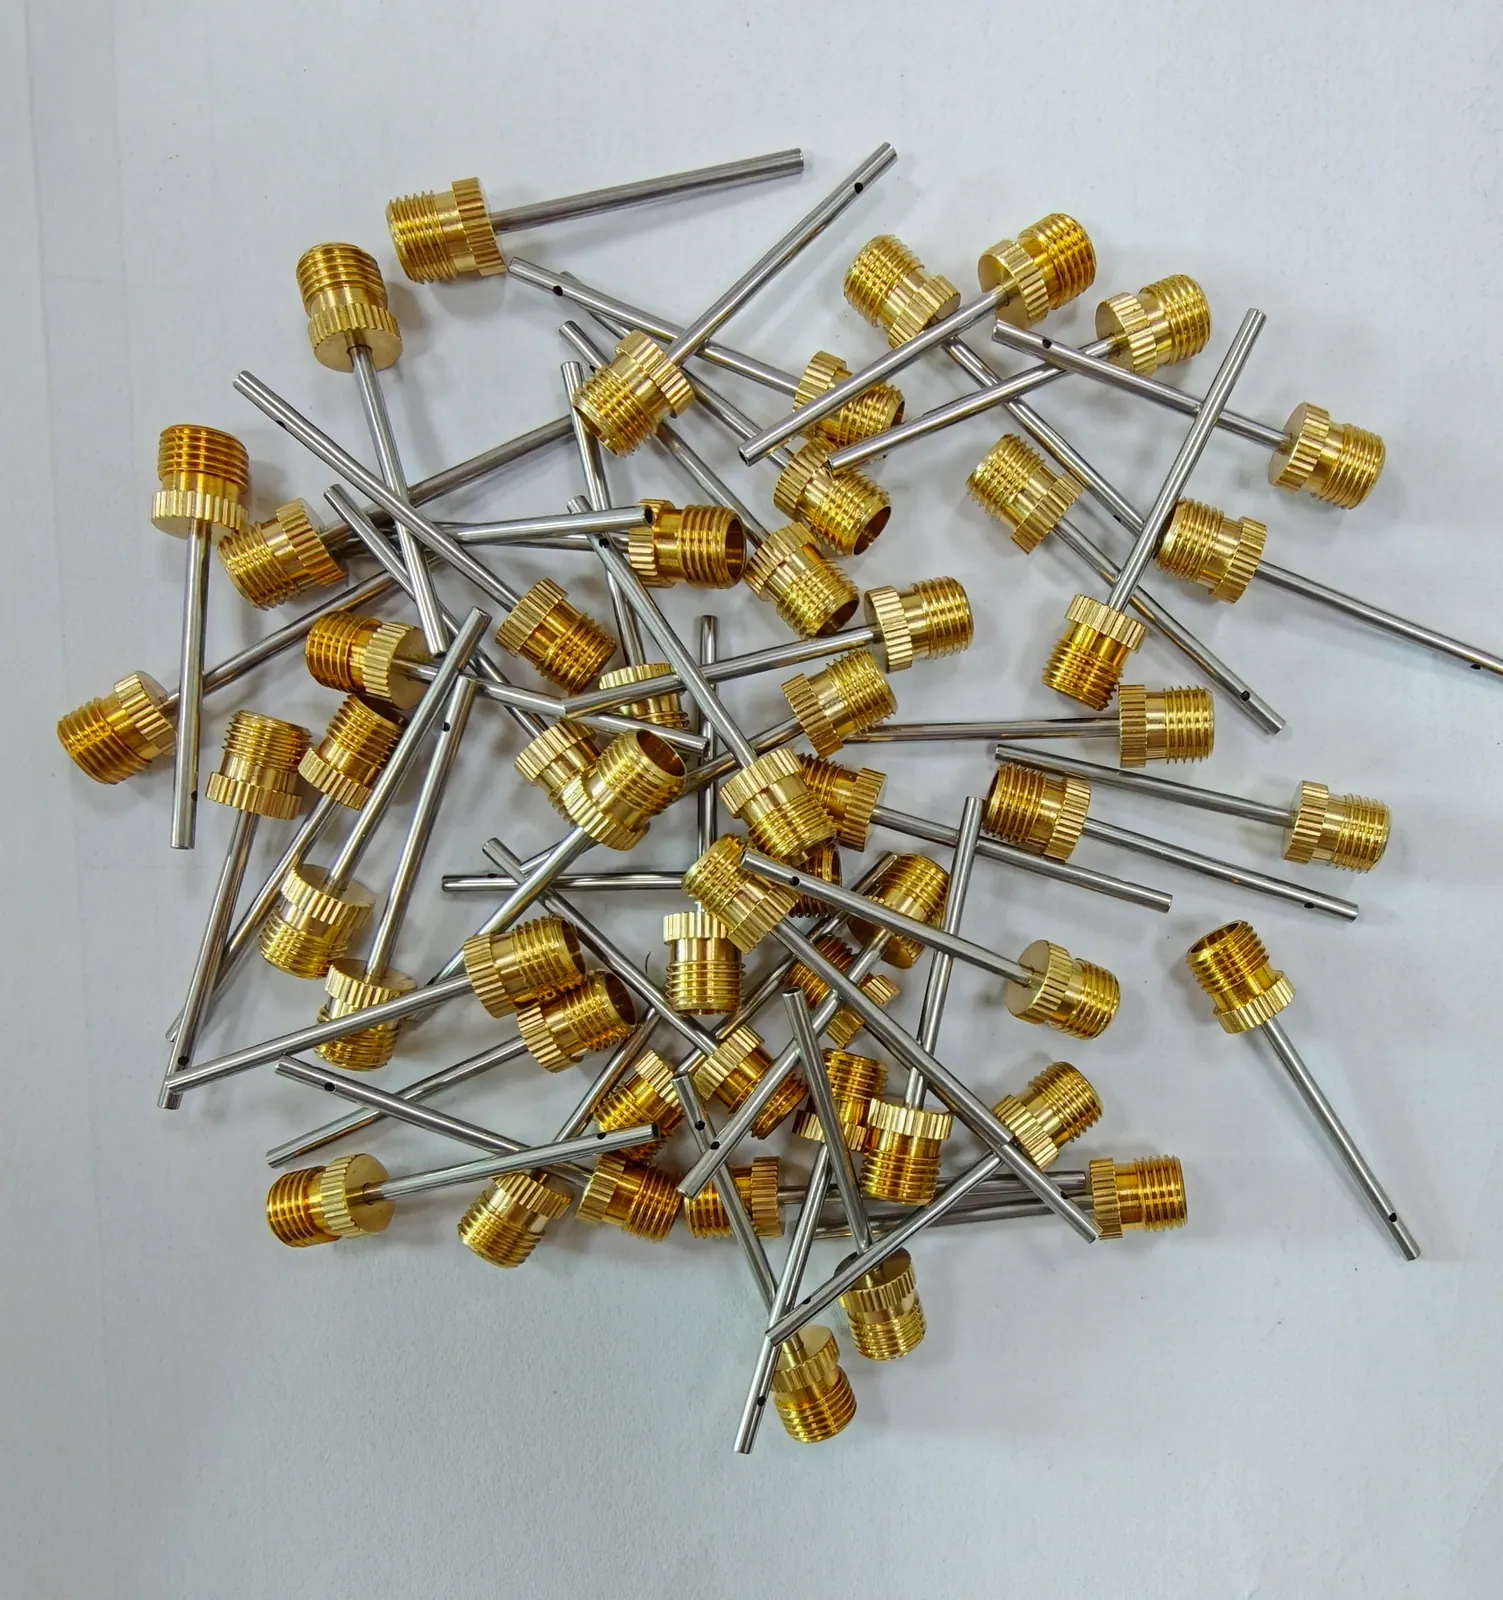
Bicycle and basketball inflation needles: knurled, threaded heads on thin tubes with a side hole 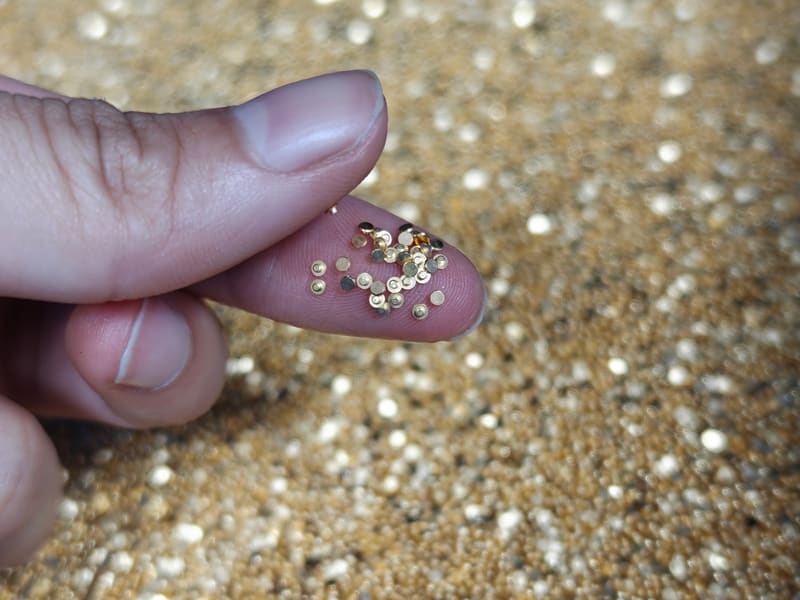
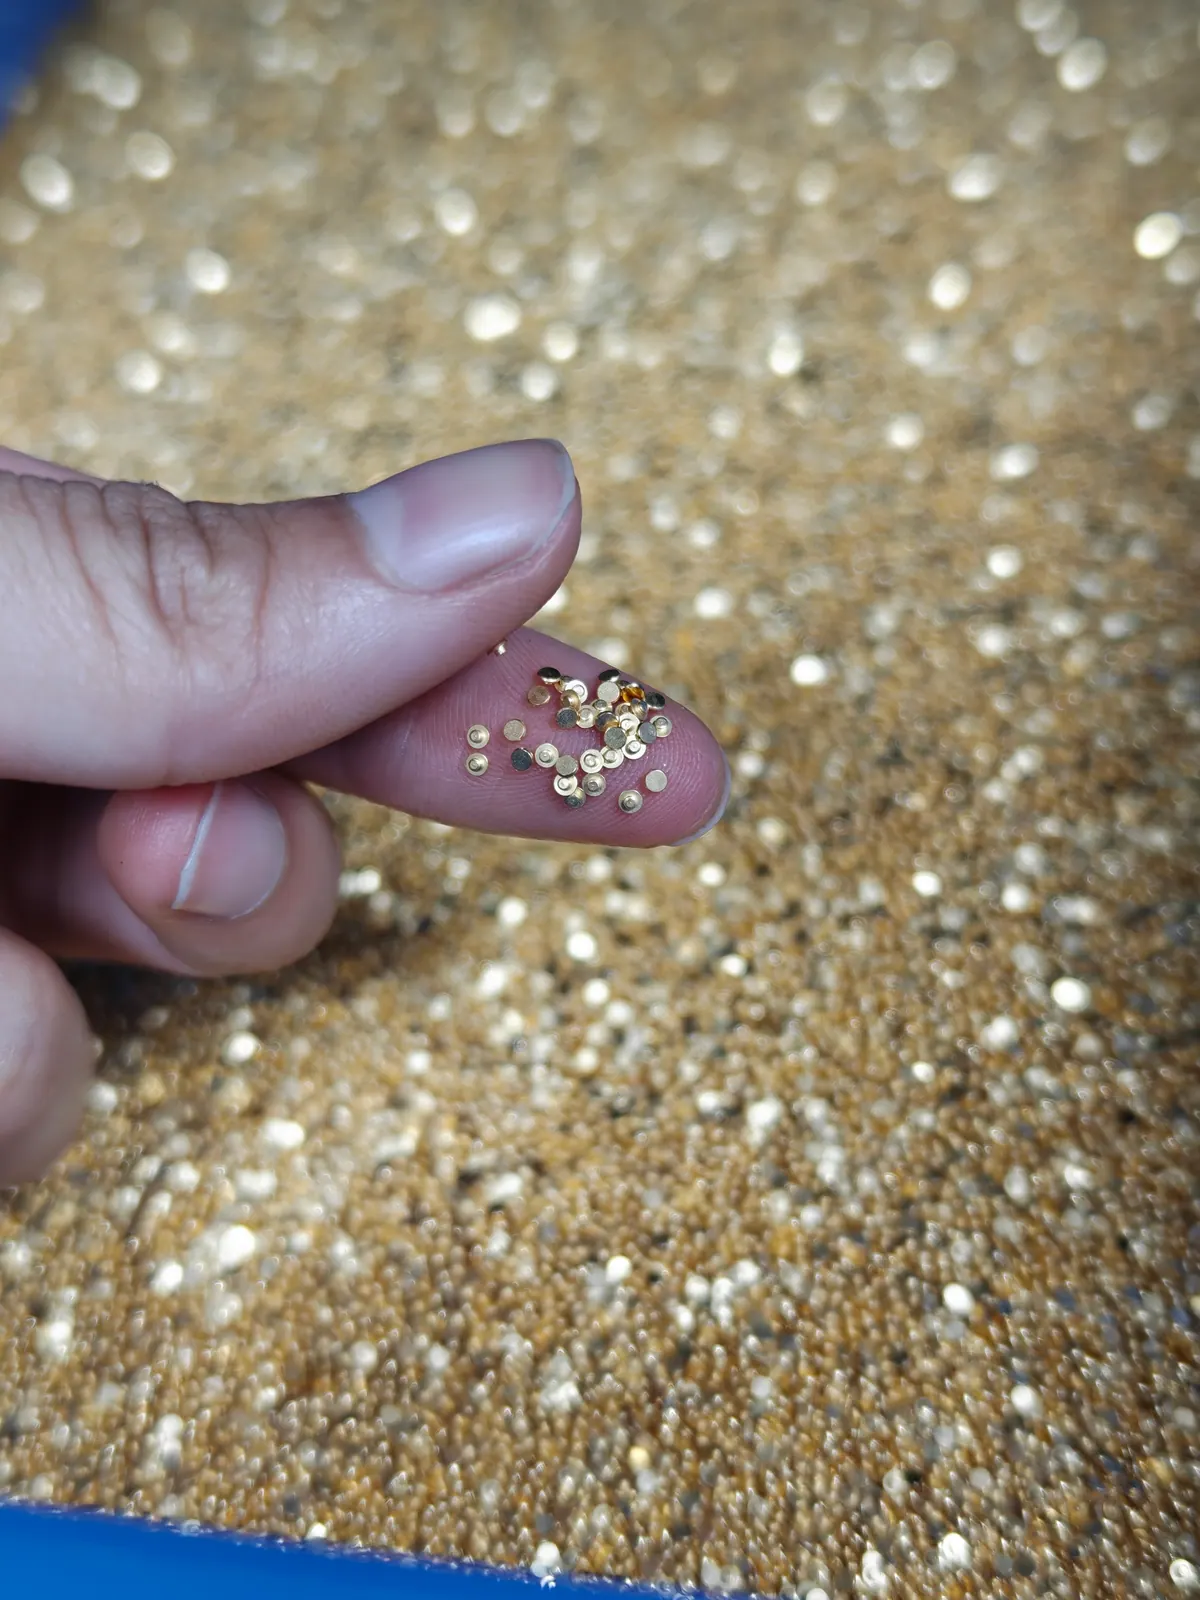
Miniature hollow stepped parts on a fingertip 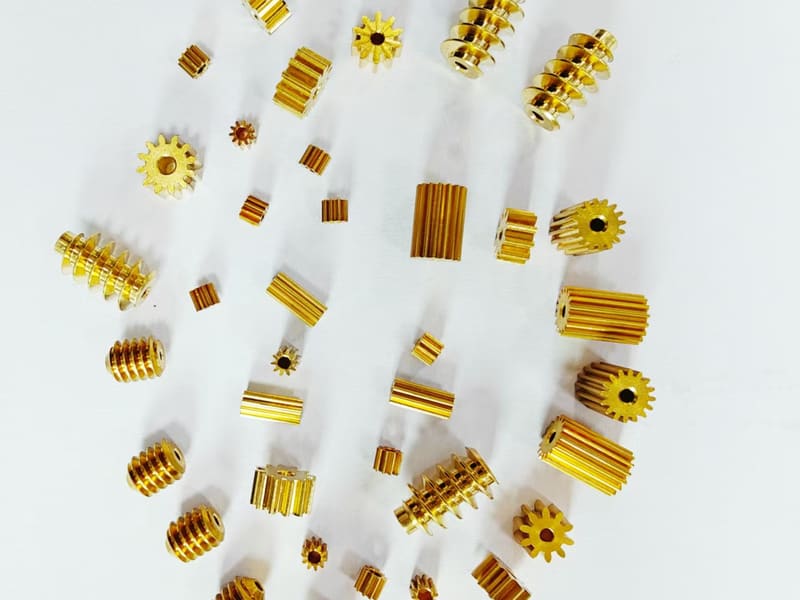
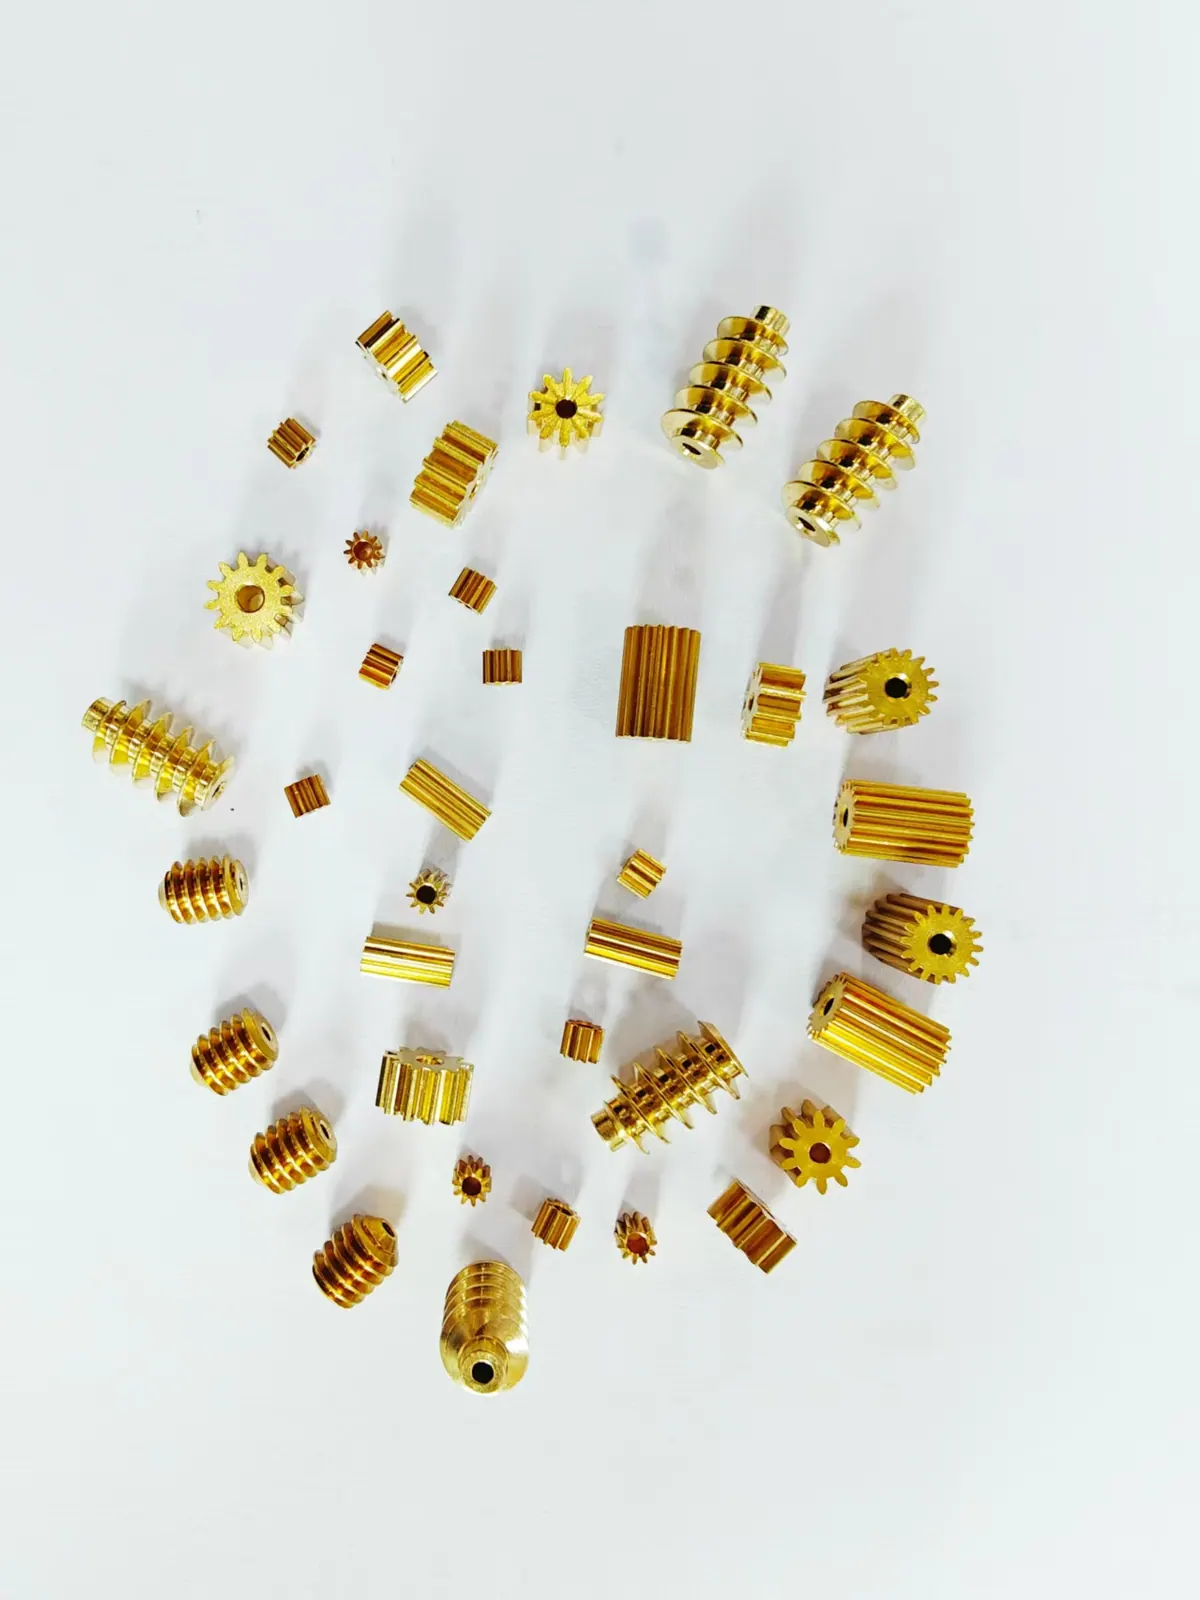
Miniature gears, worms and knurled bushings 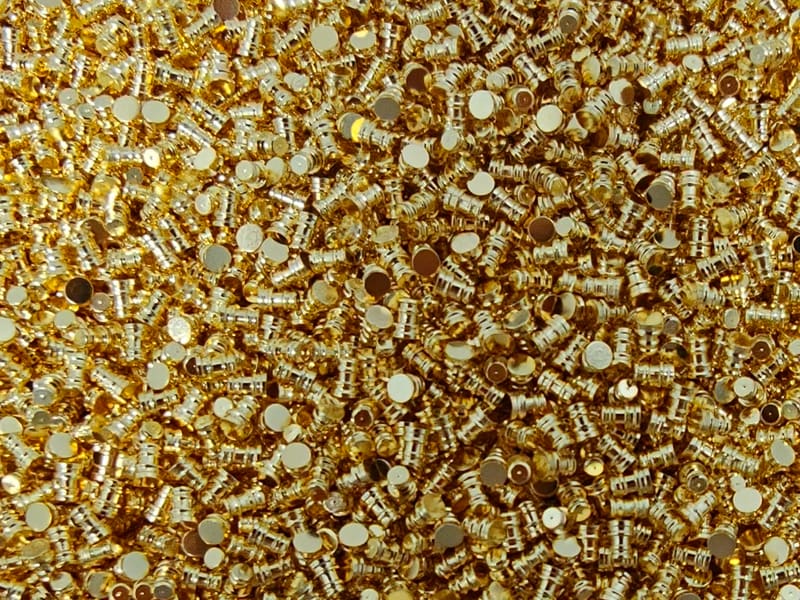
Copper pins from a batch, gold-plated by a partner 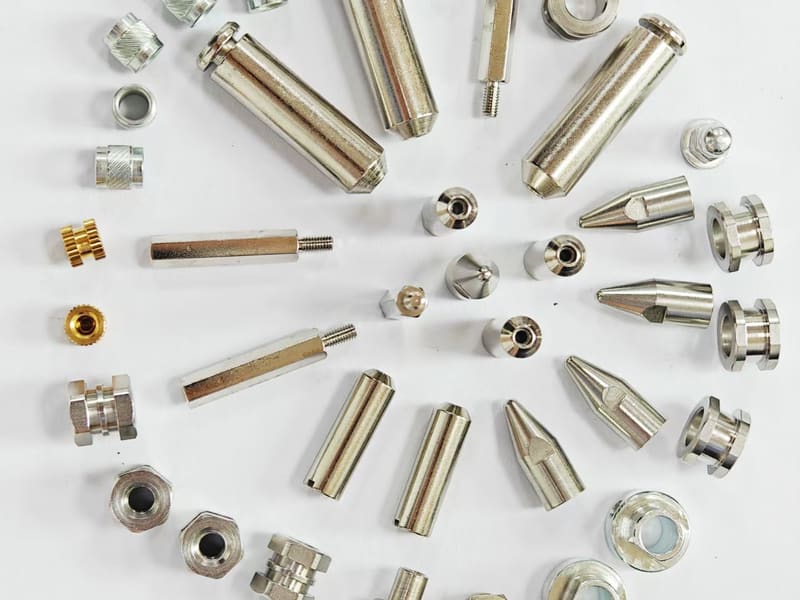
Hex standoffs, inserts, taper pins and flanged bushings 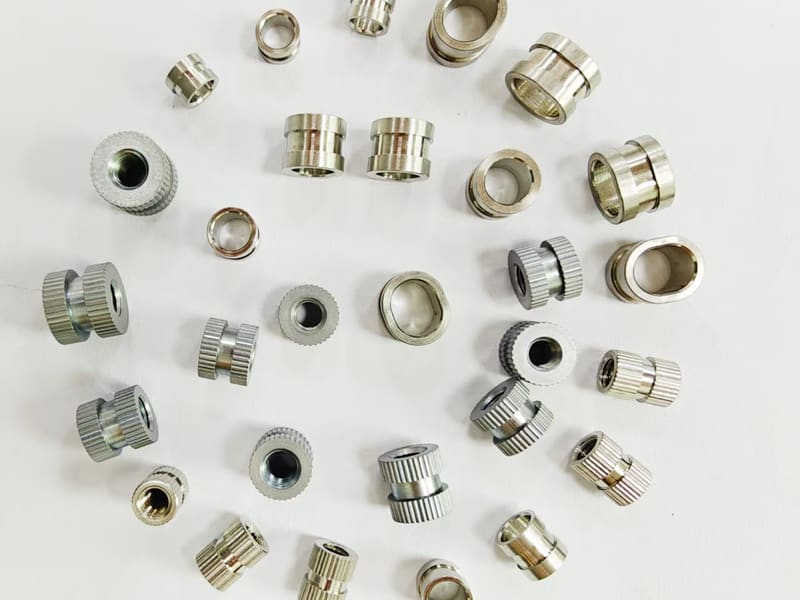
Knurled nuts and bushings 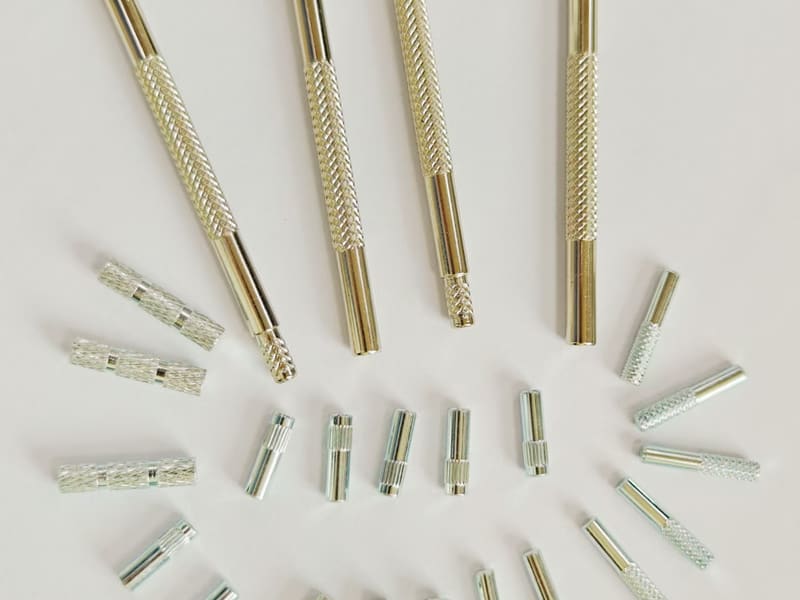
Knurled pins, long and short 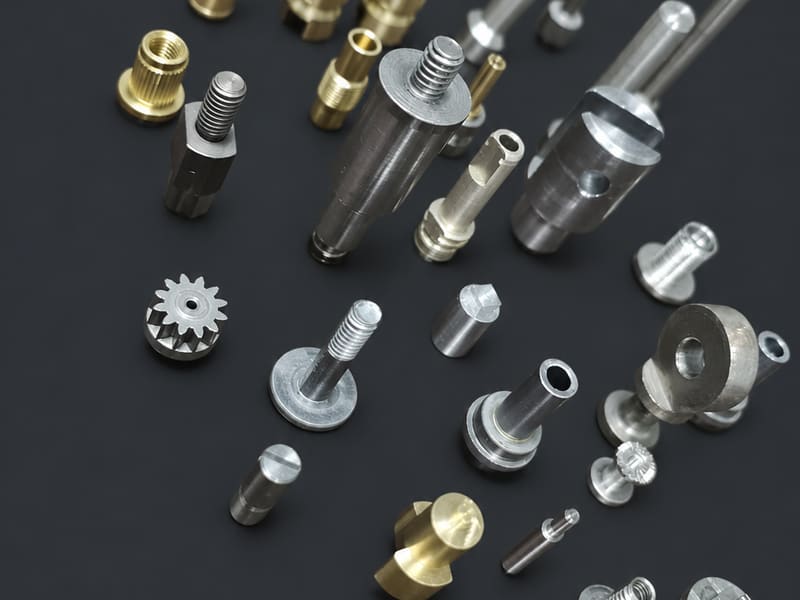
Small turned parts: shoulder screws, pins, a small gear and a threaded ring 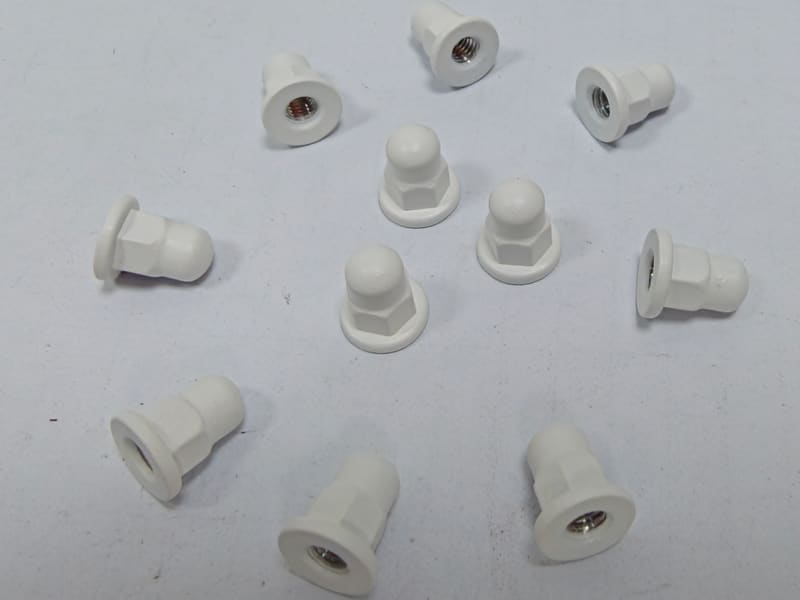
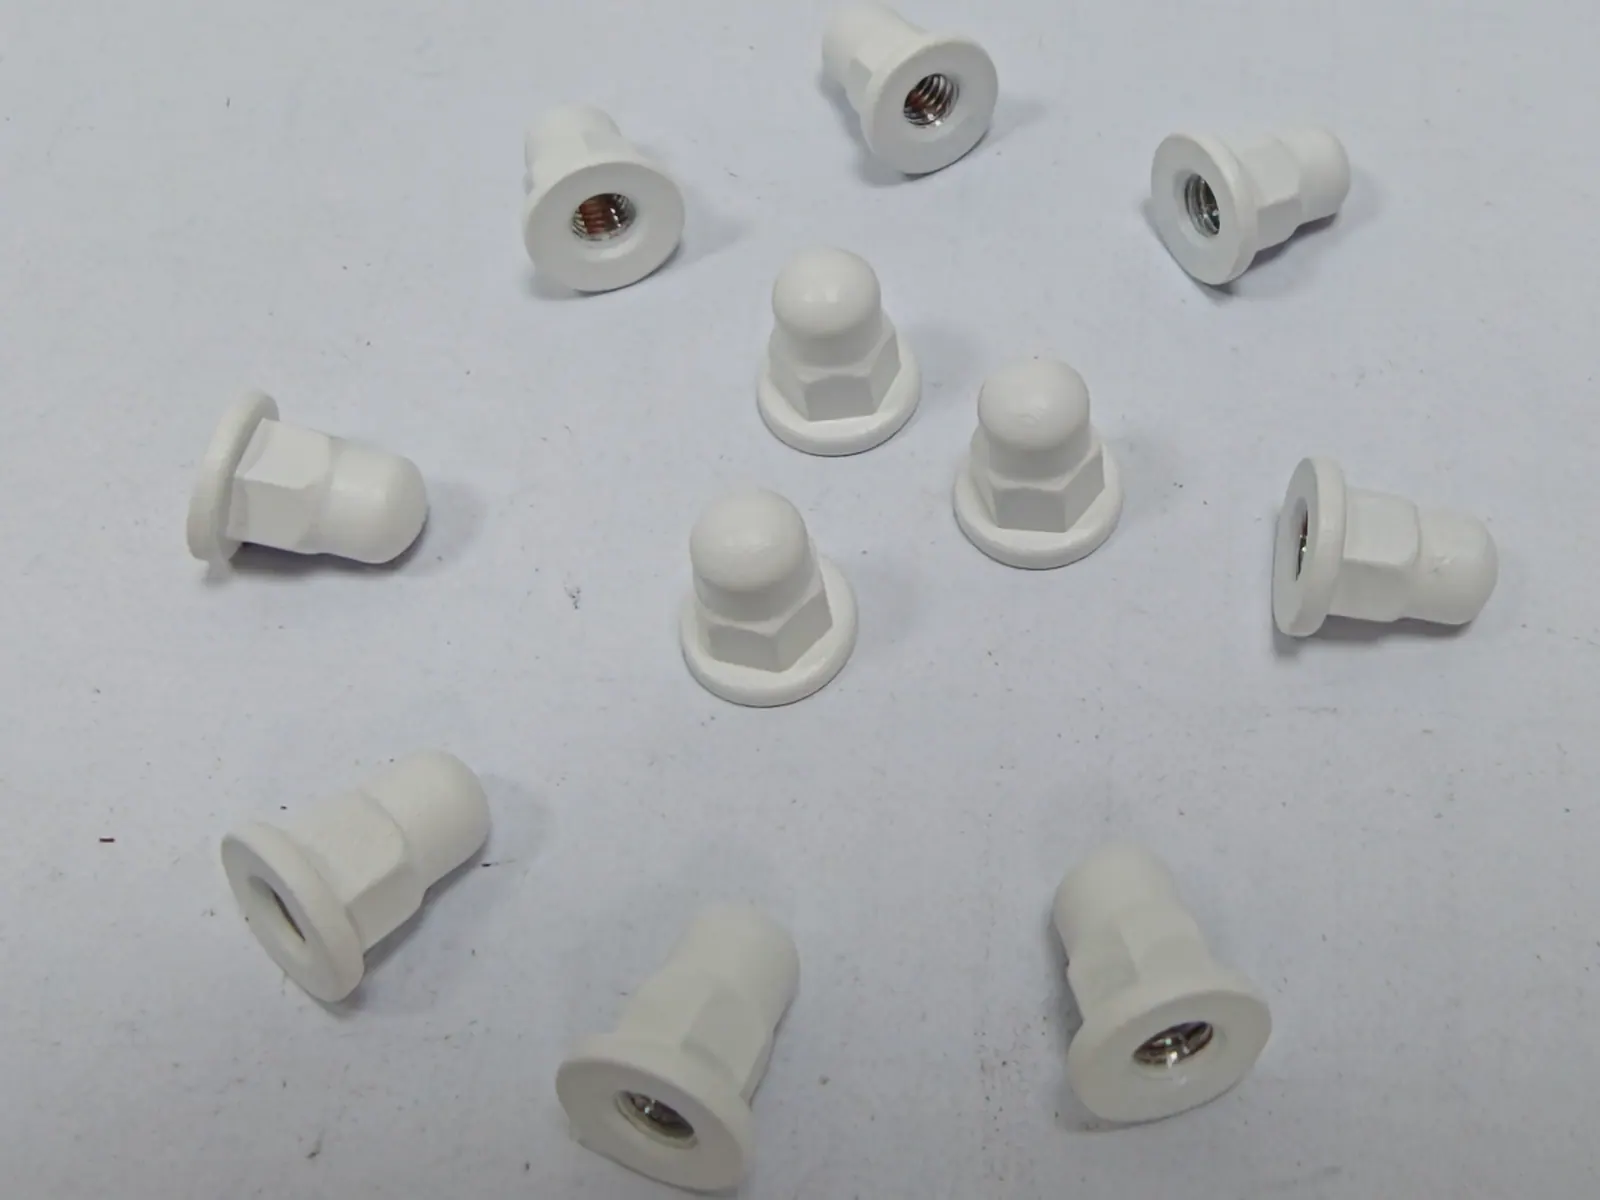
White flanged dome nuts 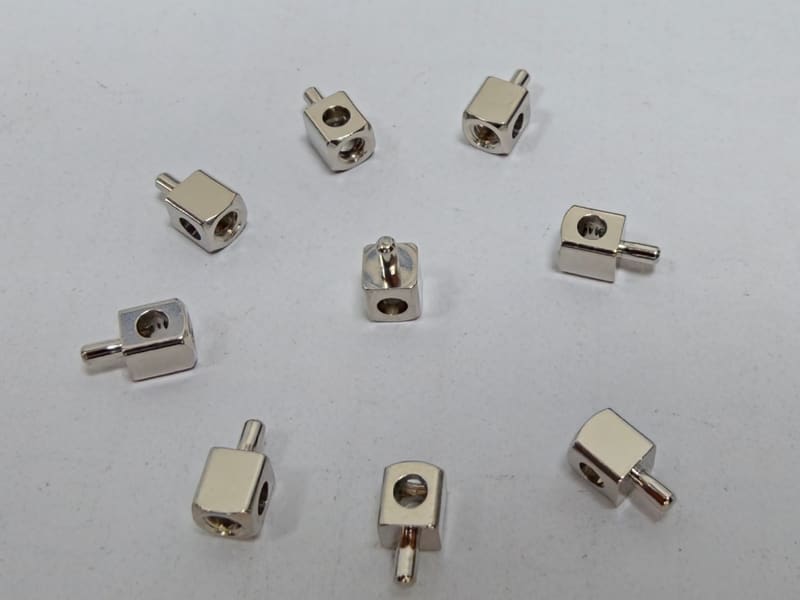
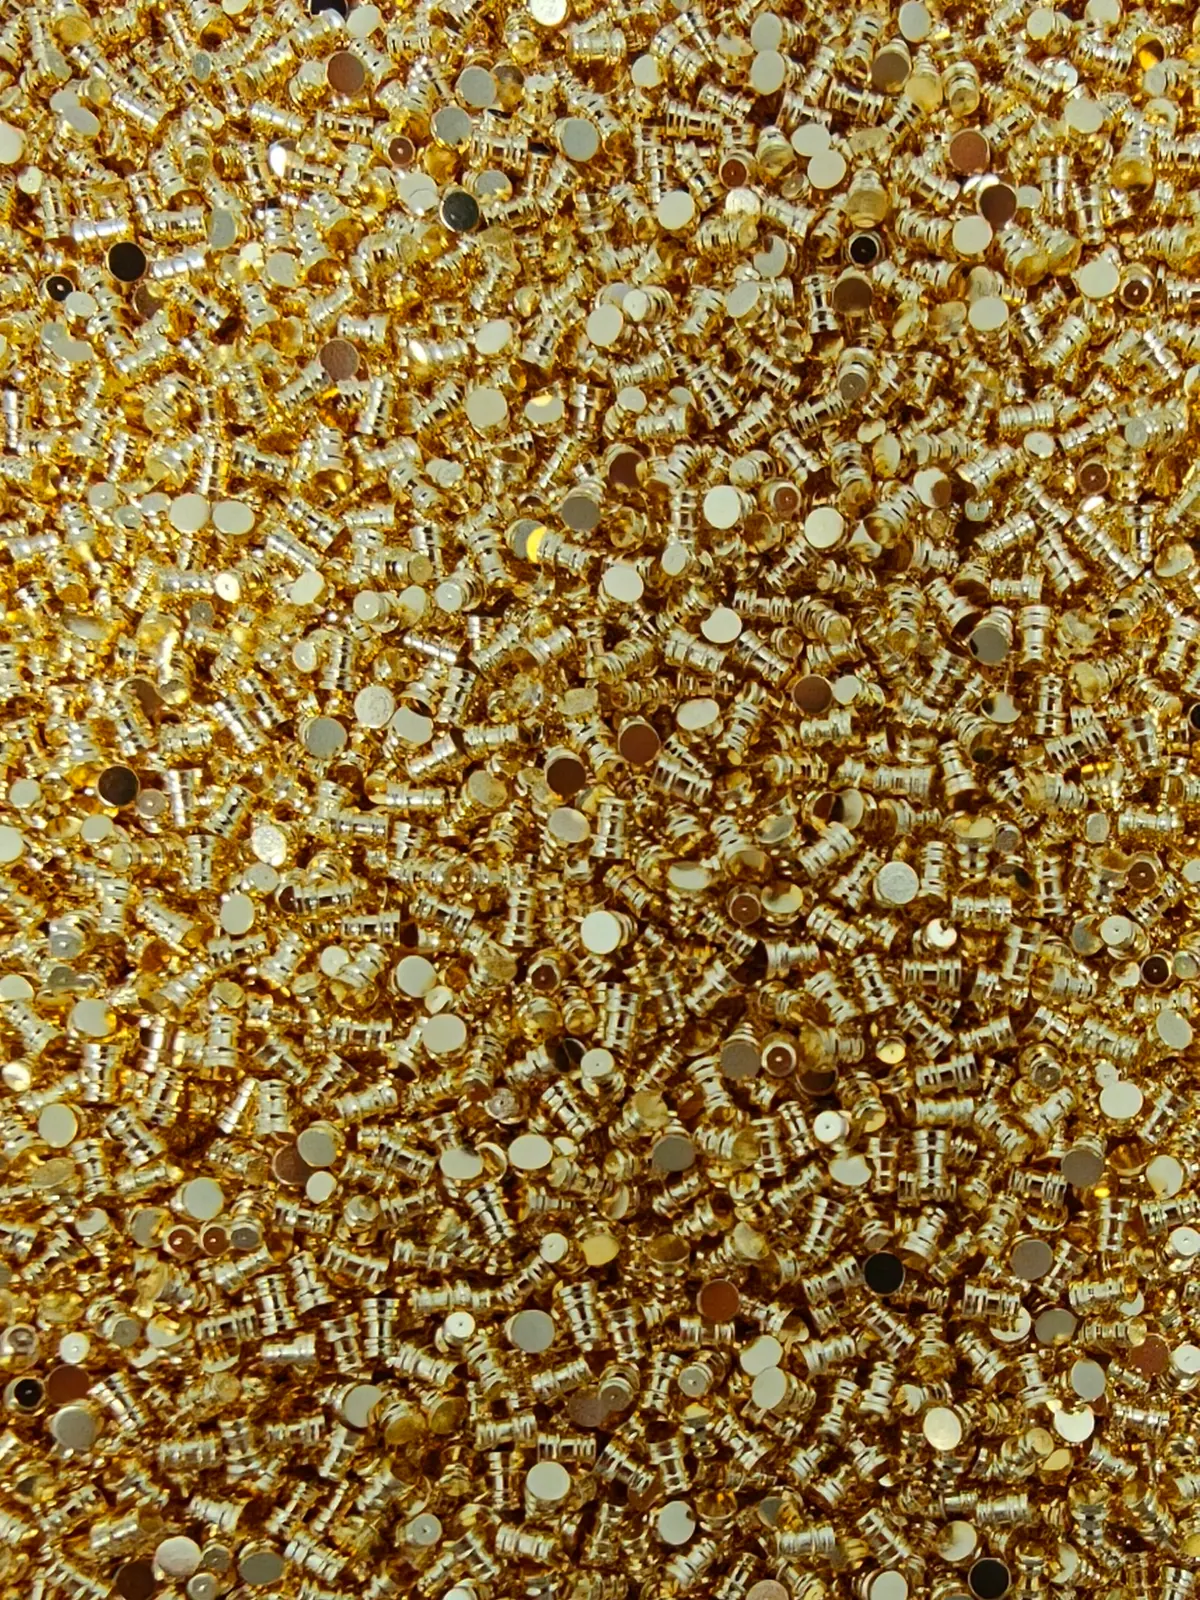
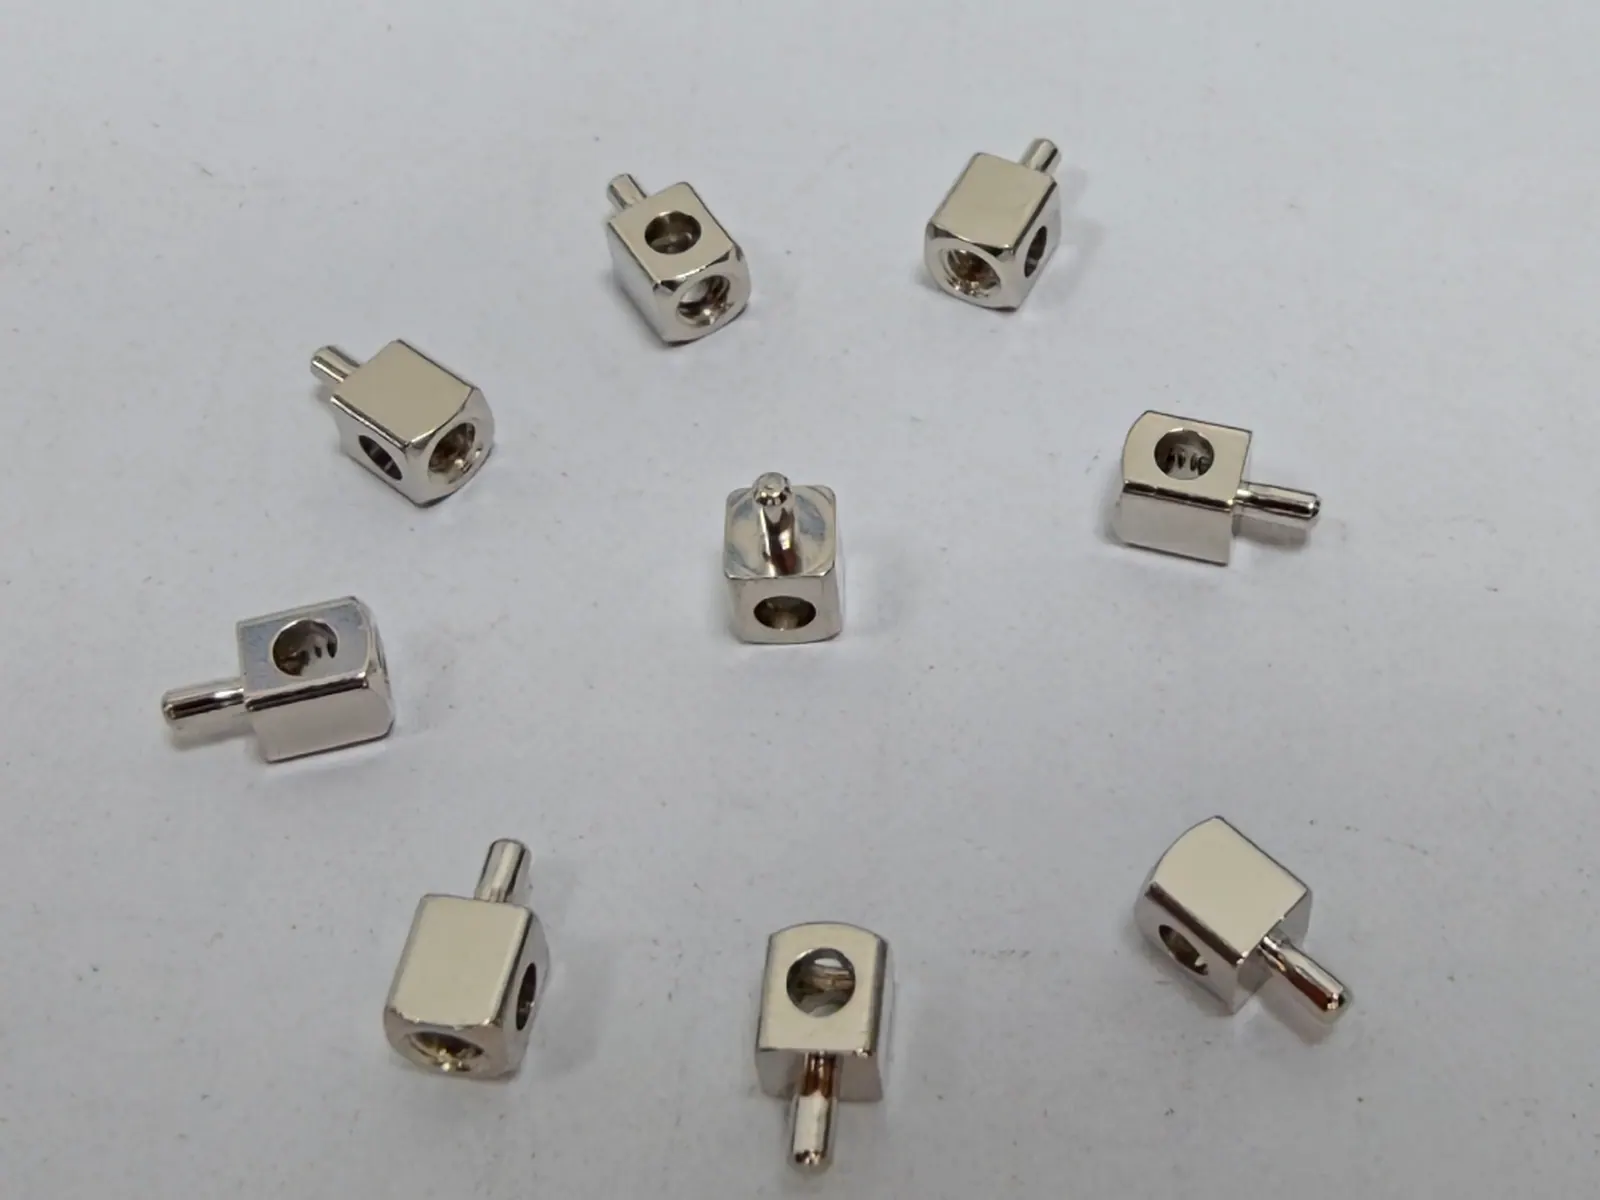
Small terminals with a cross hole
WILL IT FIT
Part envelope
Drawn to scale from the published maximum size.
Side view · L × Ø
Side view · L × Ø
Not suited for
- Parts larger than the work range of the machines
Check a part against these limits
Results
1 process with published size limits
- AUTO-TAutomatic lathe turning
Up to Ø20 × 100 mmSource: Max sizeMax sizeØ20 × 100 mmBasisDeclaredAs ofSourceSupplier information form (owner), 2026-11, automatic latheHow we label numbers
DRAWING RULES
Design rules
3 rules for automatic lathe turning drawings
- Design the largest diameter to a standard bar size: the part is turned from bar stock.
- Prefer standard thread sizes and leave a short thread run-out.
- Break sharp edges with a small chamfer, which the tools cut in the same pass.
DATASHEET
The full datasheet.
Specification, equipment, terms and questions, folded until you need them.
Specification5 materials · 8 finishes, 8 by partner suppliers
Materials and finishes
- Materials
- Stainless steel
- Copper and brass
- Aluminium
- Iron
- Steels of all kinds, incl. spring and alloy steel
- Finishes
- ElectroplatingPartner
- E-coatingPartner
- DacrometPartner
- Spray paintingPartner
- Powder coatingPartner
- AnodizingPartner
- PVDPartner
- Laser engravingPartner
Equipment1 models · 50 machines
| Type | Model | Qty | Key capacity |
|---|---|---|---|
| Automatic lathe | 1215 | 50 | Work range (Ø × L) 20 × 100 mm |
| Total: 50Note 2Machines for the process50BasisDocumentAs ofSourceSupplier information form: 50 machines listed for this processAsk for this recordHow we label numbers machines for this process | |||
Lead times and termsEvery part is quoted from its drawing
- Prototype lead time
- 10 daysNote 3Prototype lead time10 daysBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers
- Production lead time
- 15–20 daysNote 4Production lead time15–20 daysBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers
- Incoterms
- EXW Dongguan and FOB Shenzhen
Questions1 questions about automatic lathe turning and orders
How fast can I get prototypes?
The sample lead time is listed on the ordering page. It depends on the part and is confirmed in the quote.
Quote a automatic lathe turning part
Amy
International Sales Manager
Phone and email: English and Chinese
Lu Dadong
General Manager
Drawings and technical questions
Phone: Chinese · Email: English and Chinese
Sources
Every figure on this page, with its source and date.
- Max size: Ø20 × 100 mm. Source: Supplier information form (owner), 2026-11, automatic lathe; as of 6 November 2026.
- Machines for the process: 50. Source: Supplier information form: 50 machines listed for this process; as of 6 November 2026.
- Prototype lead time: 10 days. Source: Owner, 2026-11; as of 6 November 2026.
- Production lead time: 15–20 days. Source: Owner, 2026-11; as of 6 November 2026.
Data revised