- 600 × 600 mmLargest partSource: Max sizeMax size600 × 600 mmBasisDeclaredAs ofSourceSupplier information form (owner), 2026-11How we label numbers
- ±0.01 mmBest toleranceSource: Best toleranceConditionsmany features, not only hole positions; measured hole positions are typically 0.02 mmBest tolerance±0.01 mmBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers
- 15Machines for this processSource: Machines for the processMachines for the process15BasisDocumentAs ofSourceSupplier information form: 15 machines listed for this processAsk for this recordHow we label numbers
IN 3D
Turn the part. Check the dimensions.
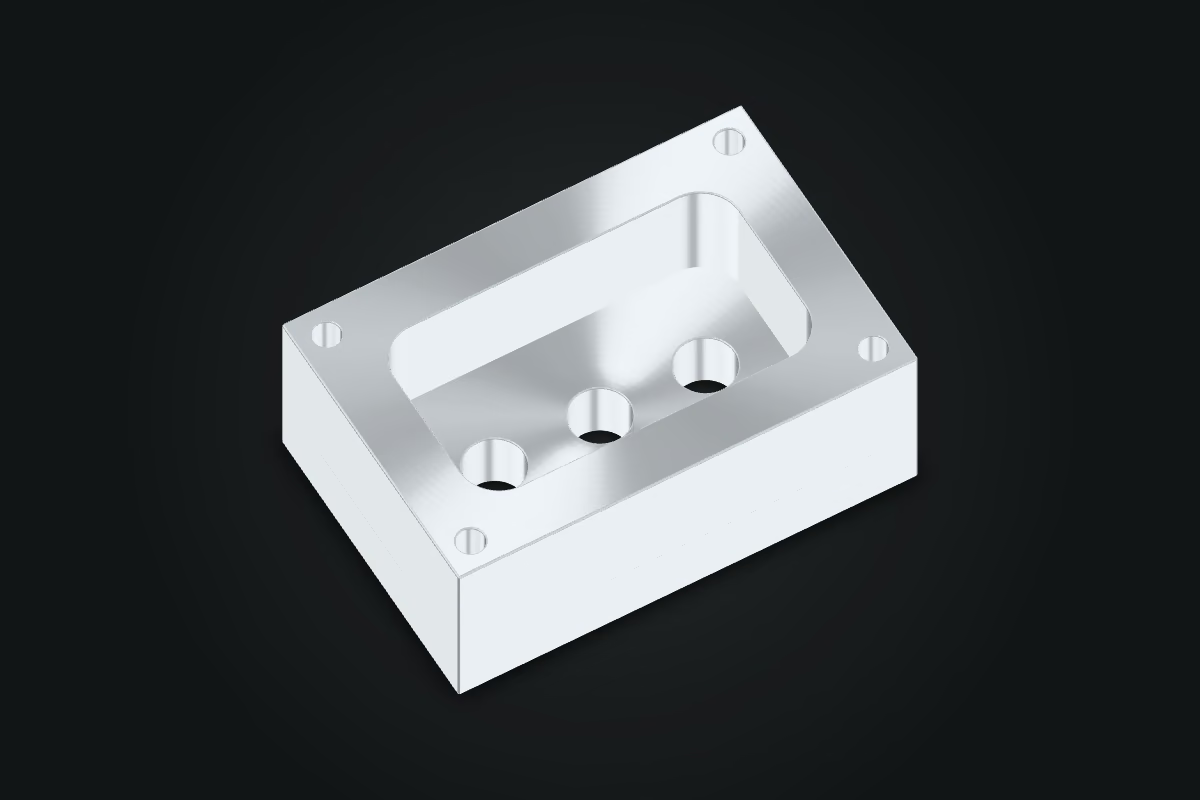
Machined flange: Aluminium 6061-T6, clear anodizing.Drag or use the arrow keys to turn a part; select a feature to see its dimension.Swipe sideways to turn a part; tap a feature to see its dimension.Load the 3D view to turn a part and select a feature on it.Select a part to see its drawing and key features.
Rendered illustration, not a photograph of a delivered part. Geometry from showcase data.
Machined flange
- Process
- CNC milling
- Material
- Aluminium 6061-T6
- Finish
- Clear anodizing
Key features
- Centre boreØ30 mm±0.01 mm
- Bolt circle, 4 holesPCD 60 mm±0.05 mm
- Flange thickness12 mm±0.02 mm
Values from the sample part drawing.
Arrow keys turn the part. Home resets the view. Number keys select a feature.
HOW IT IS MADE
How a milled part is made
An end mill clears the pocket in passes, a smaller one circles out the bores and a drill sinks the holes.
Illustration
THE PART
Sample parts
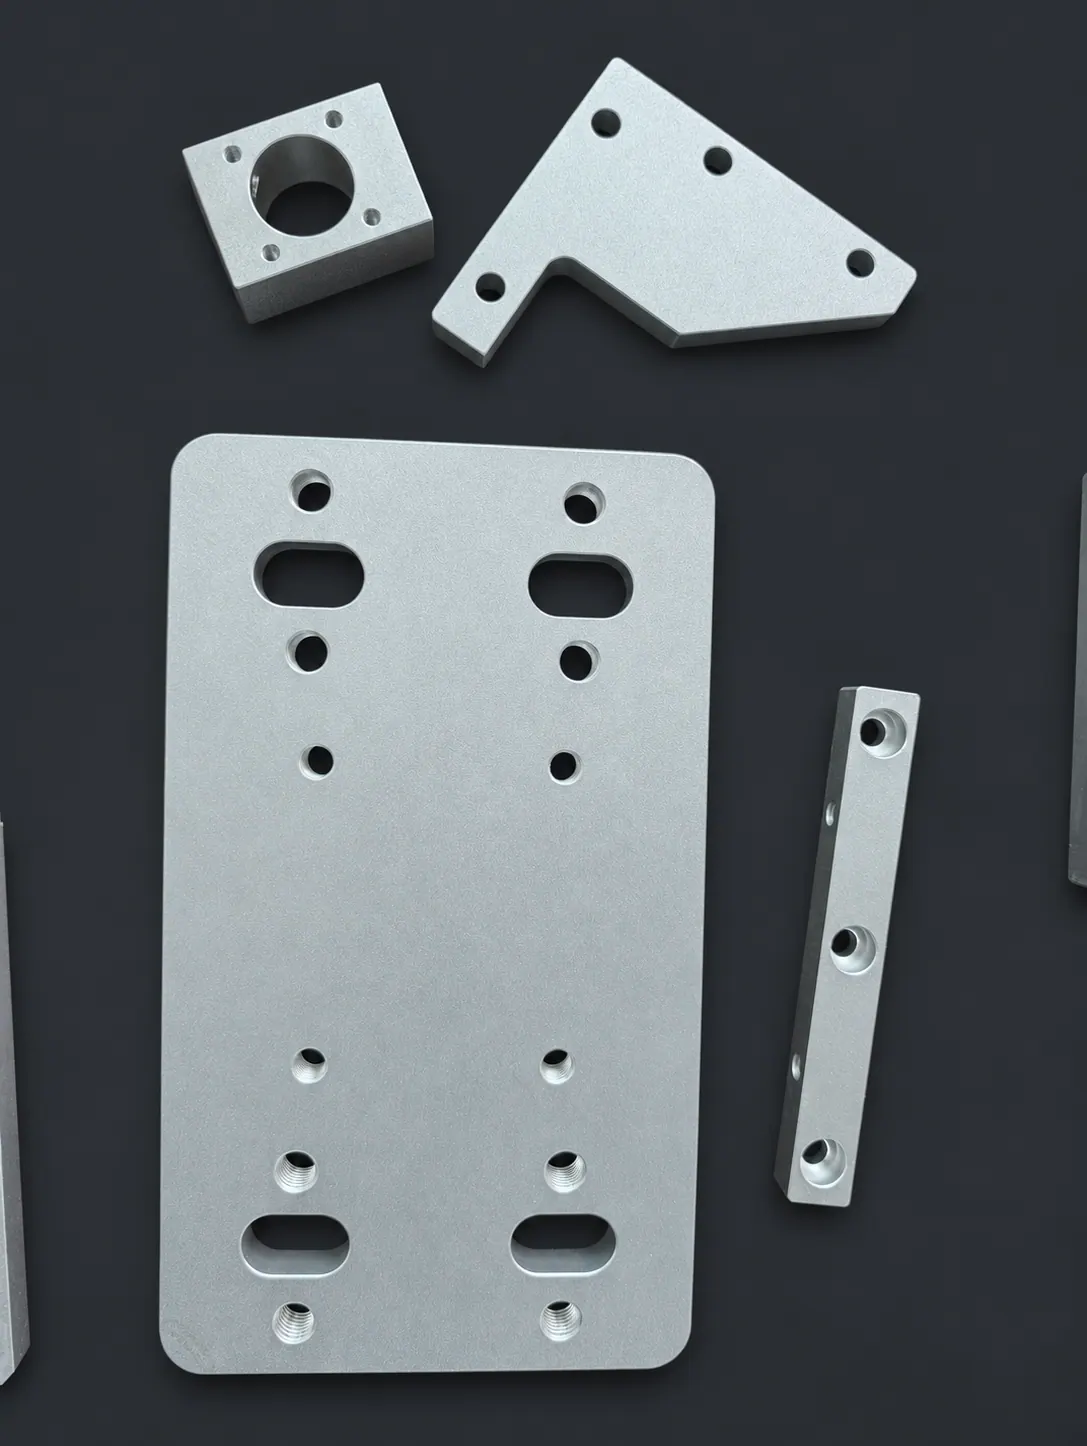
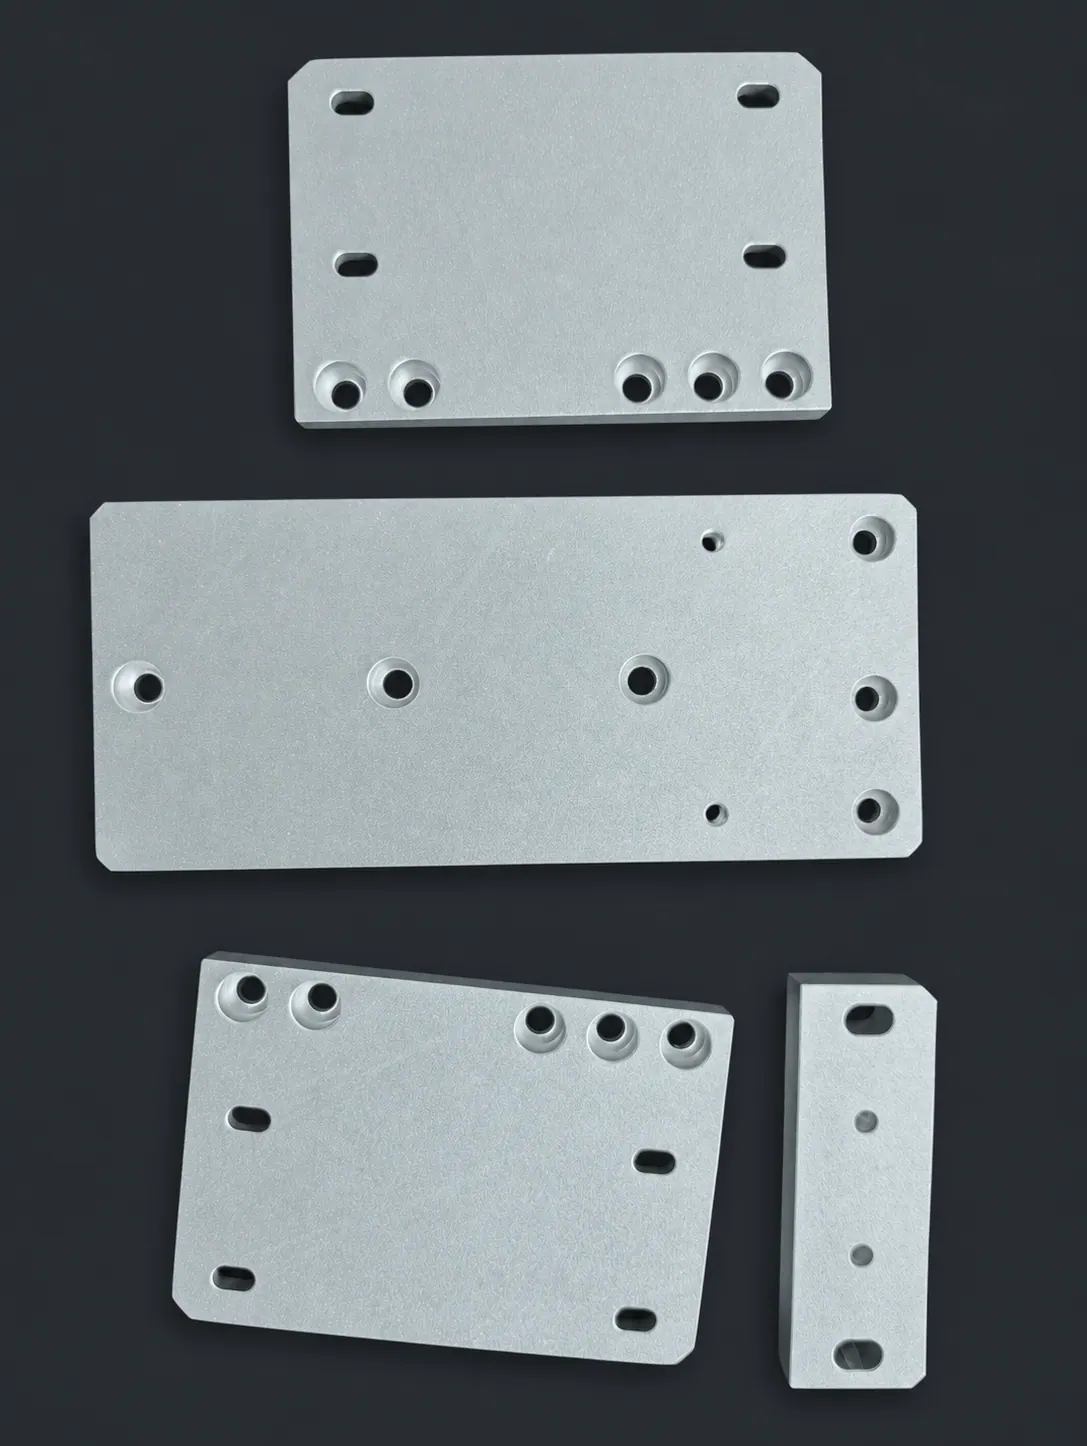
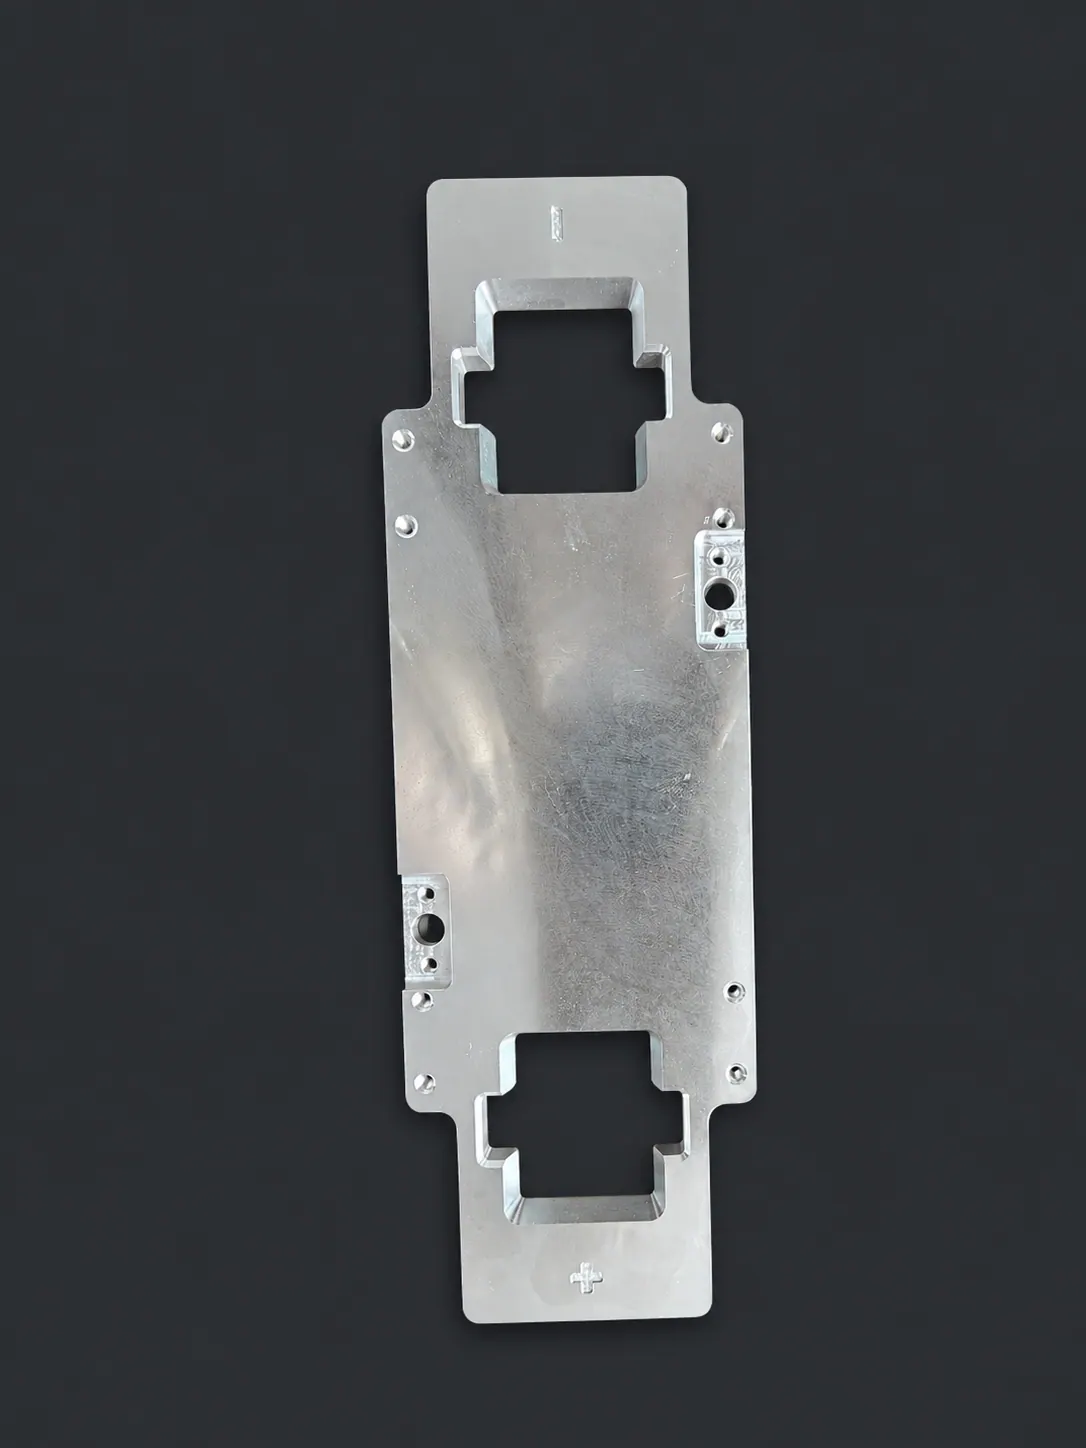
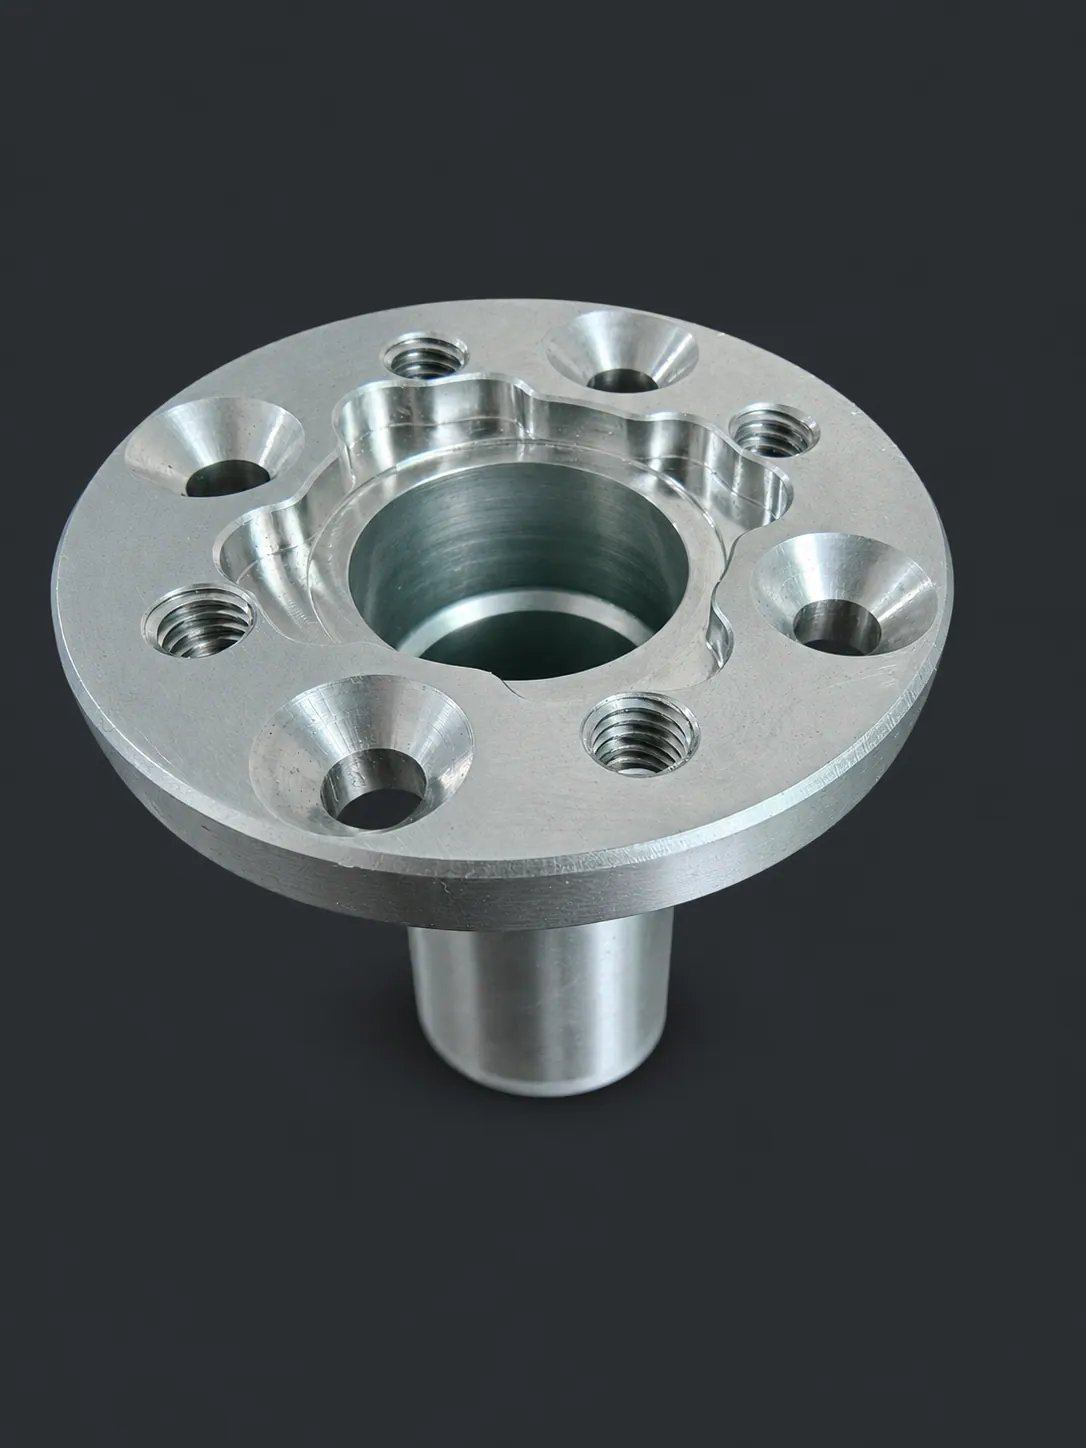
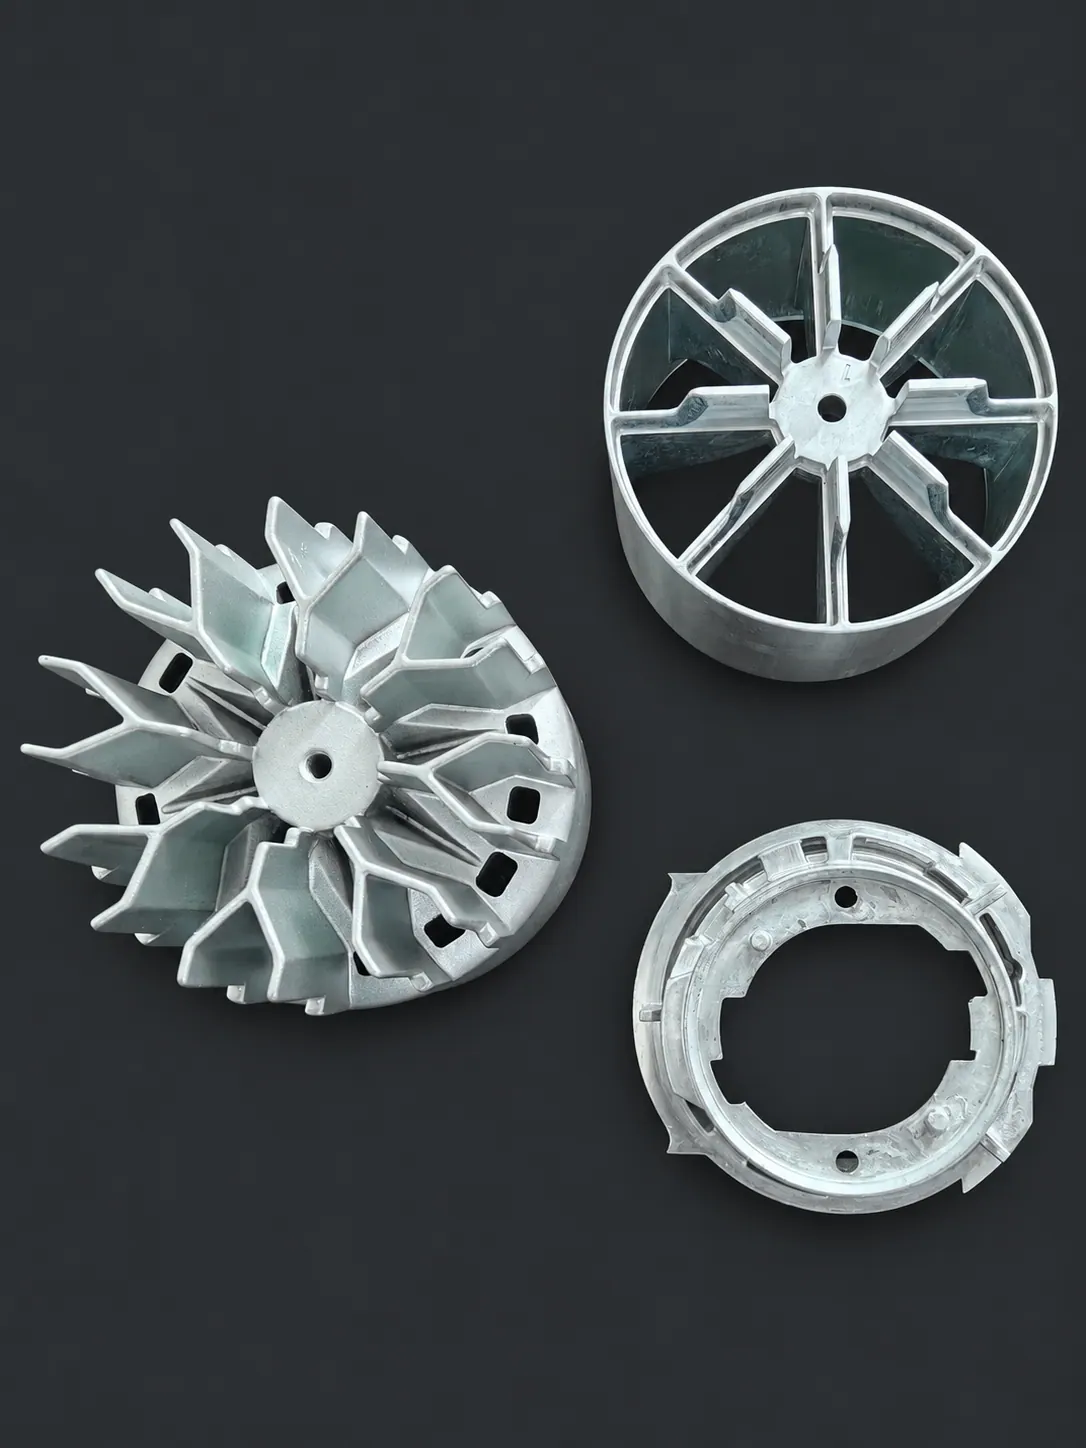
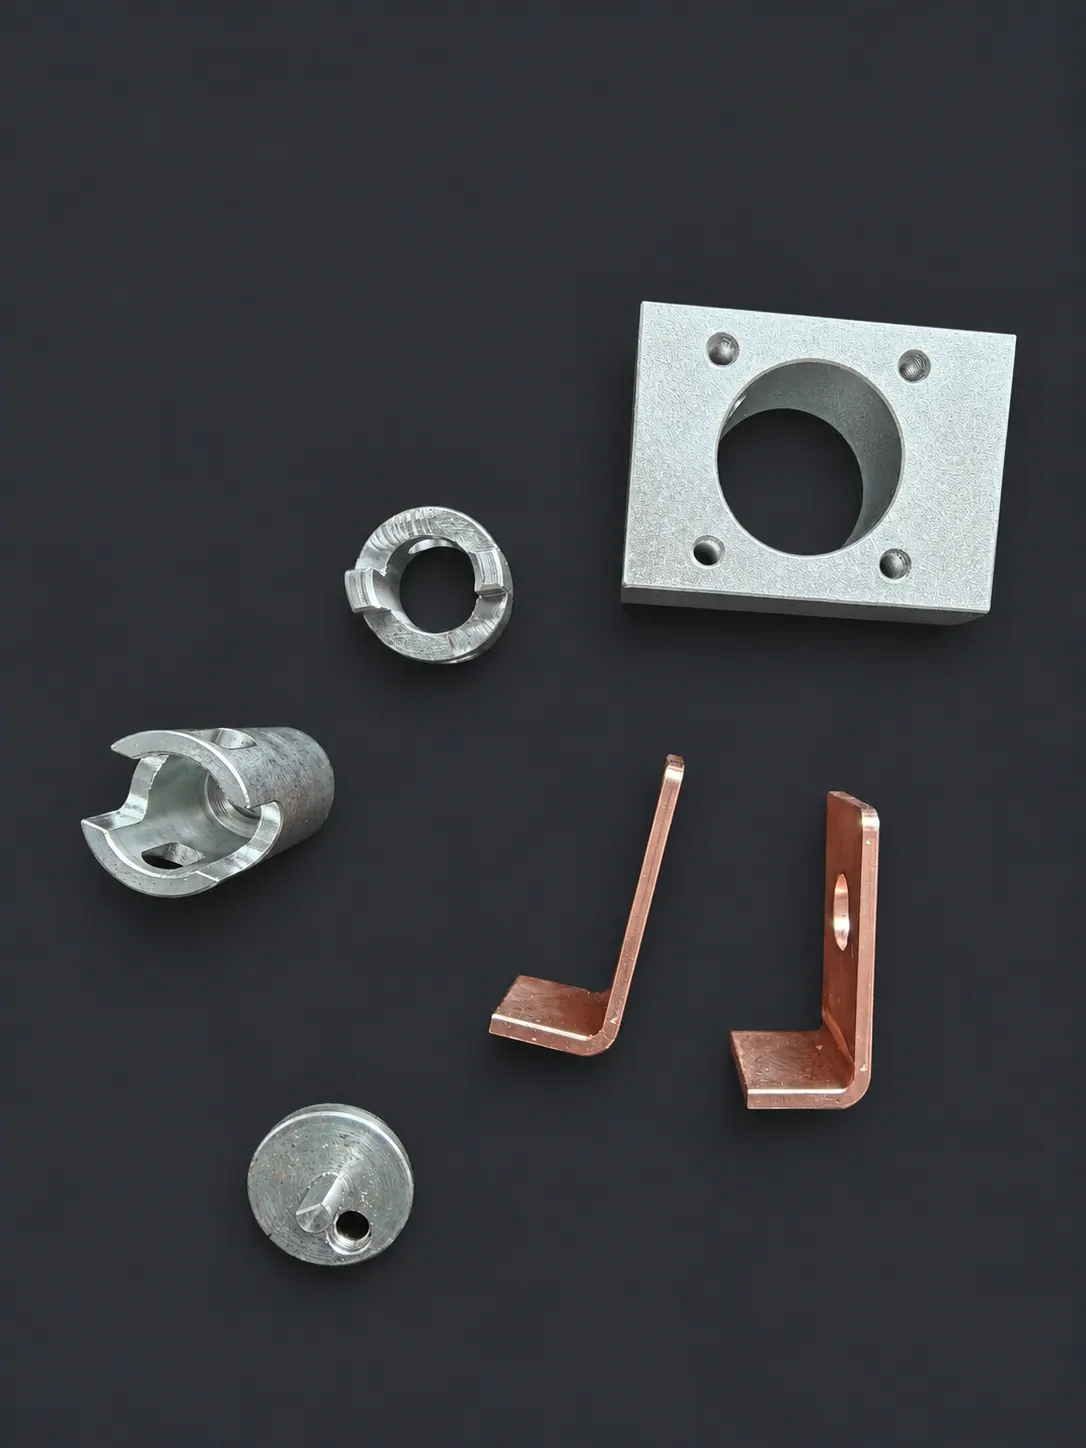
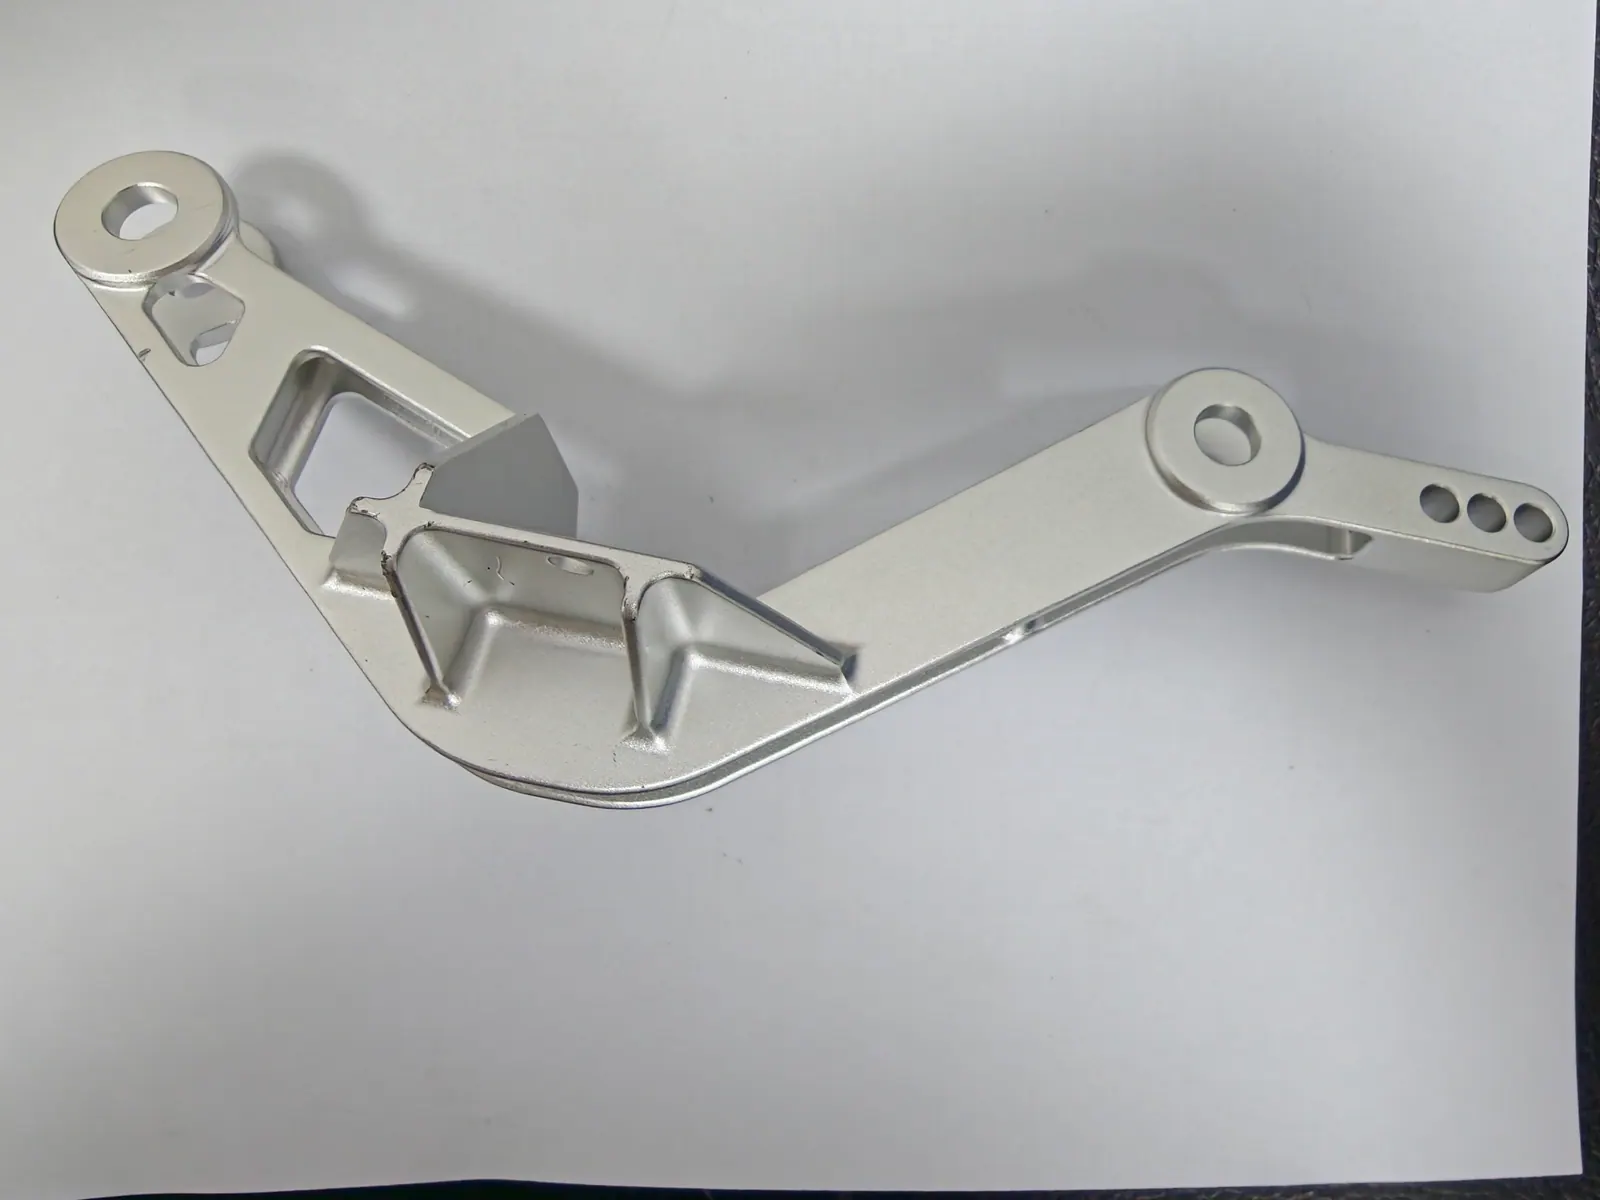
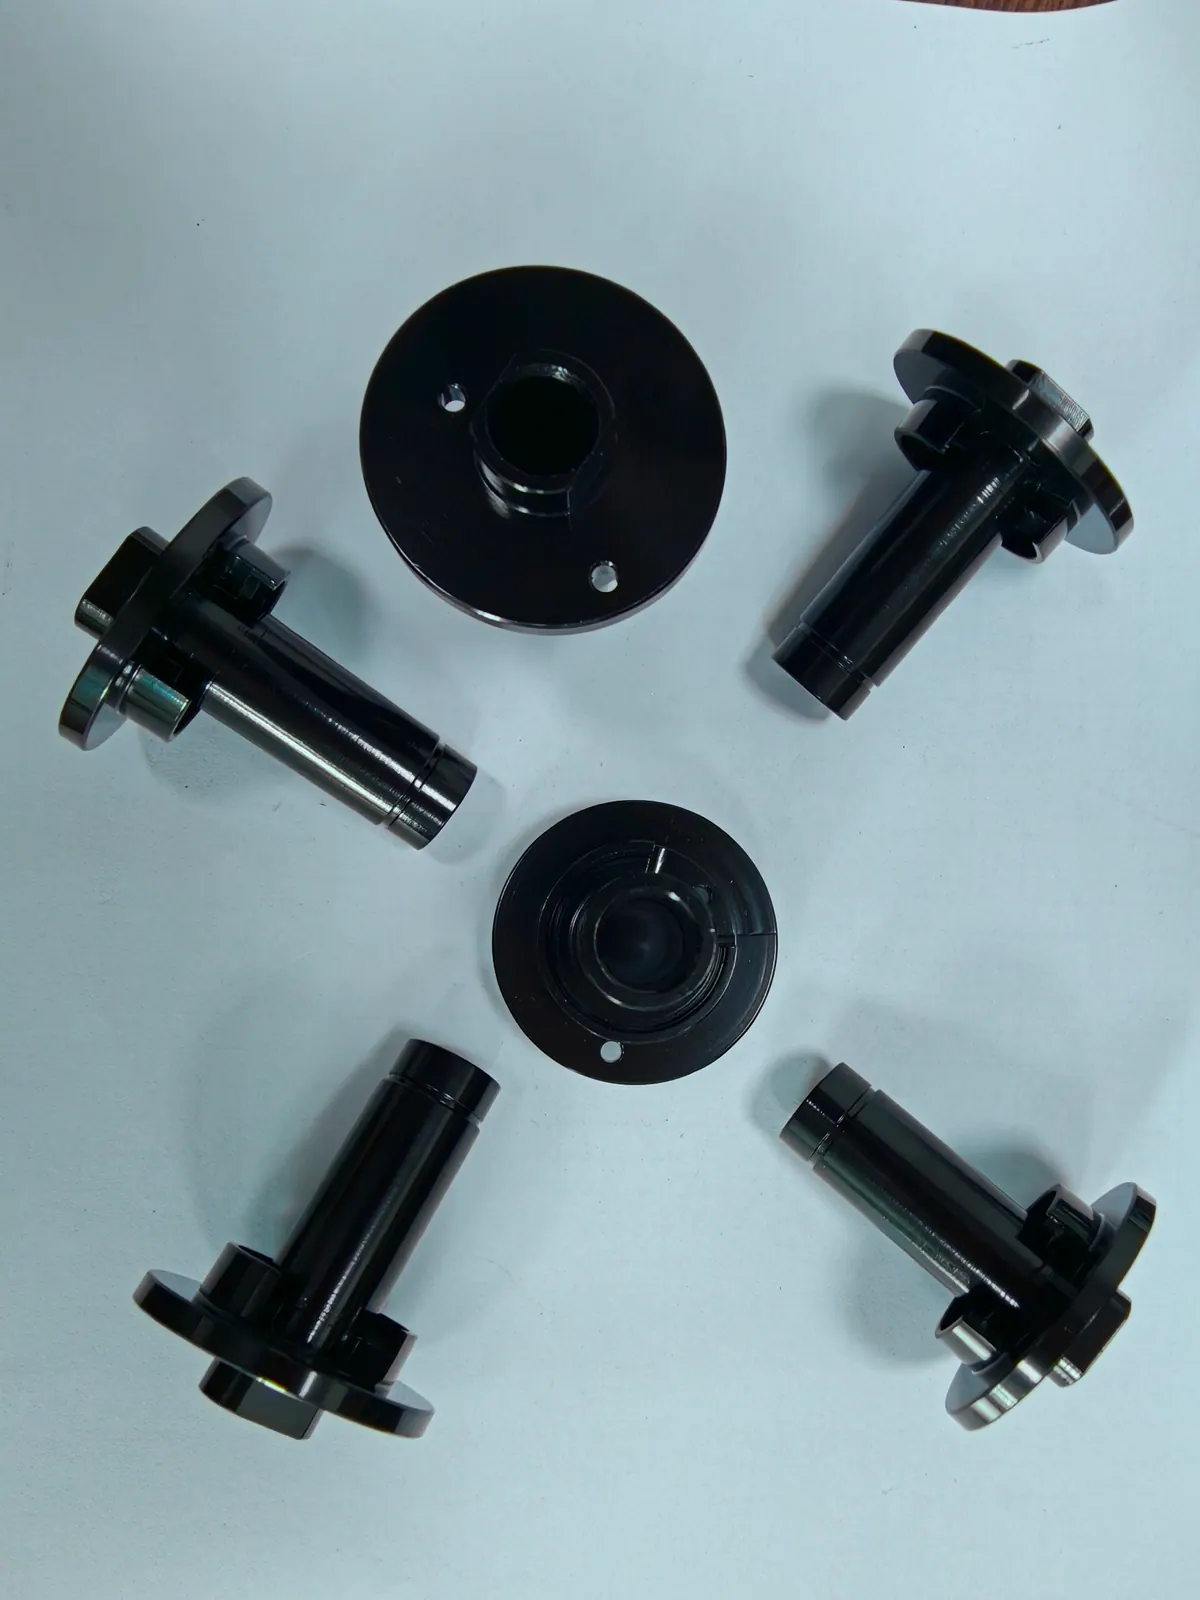
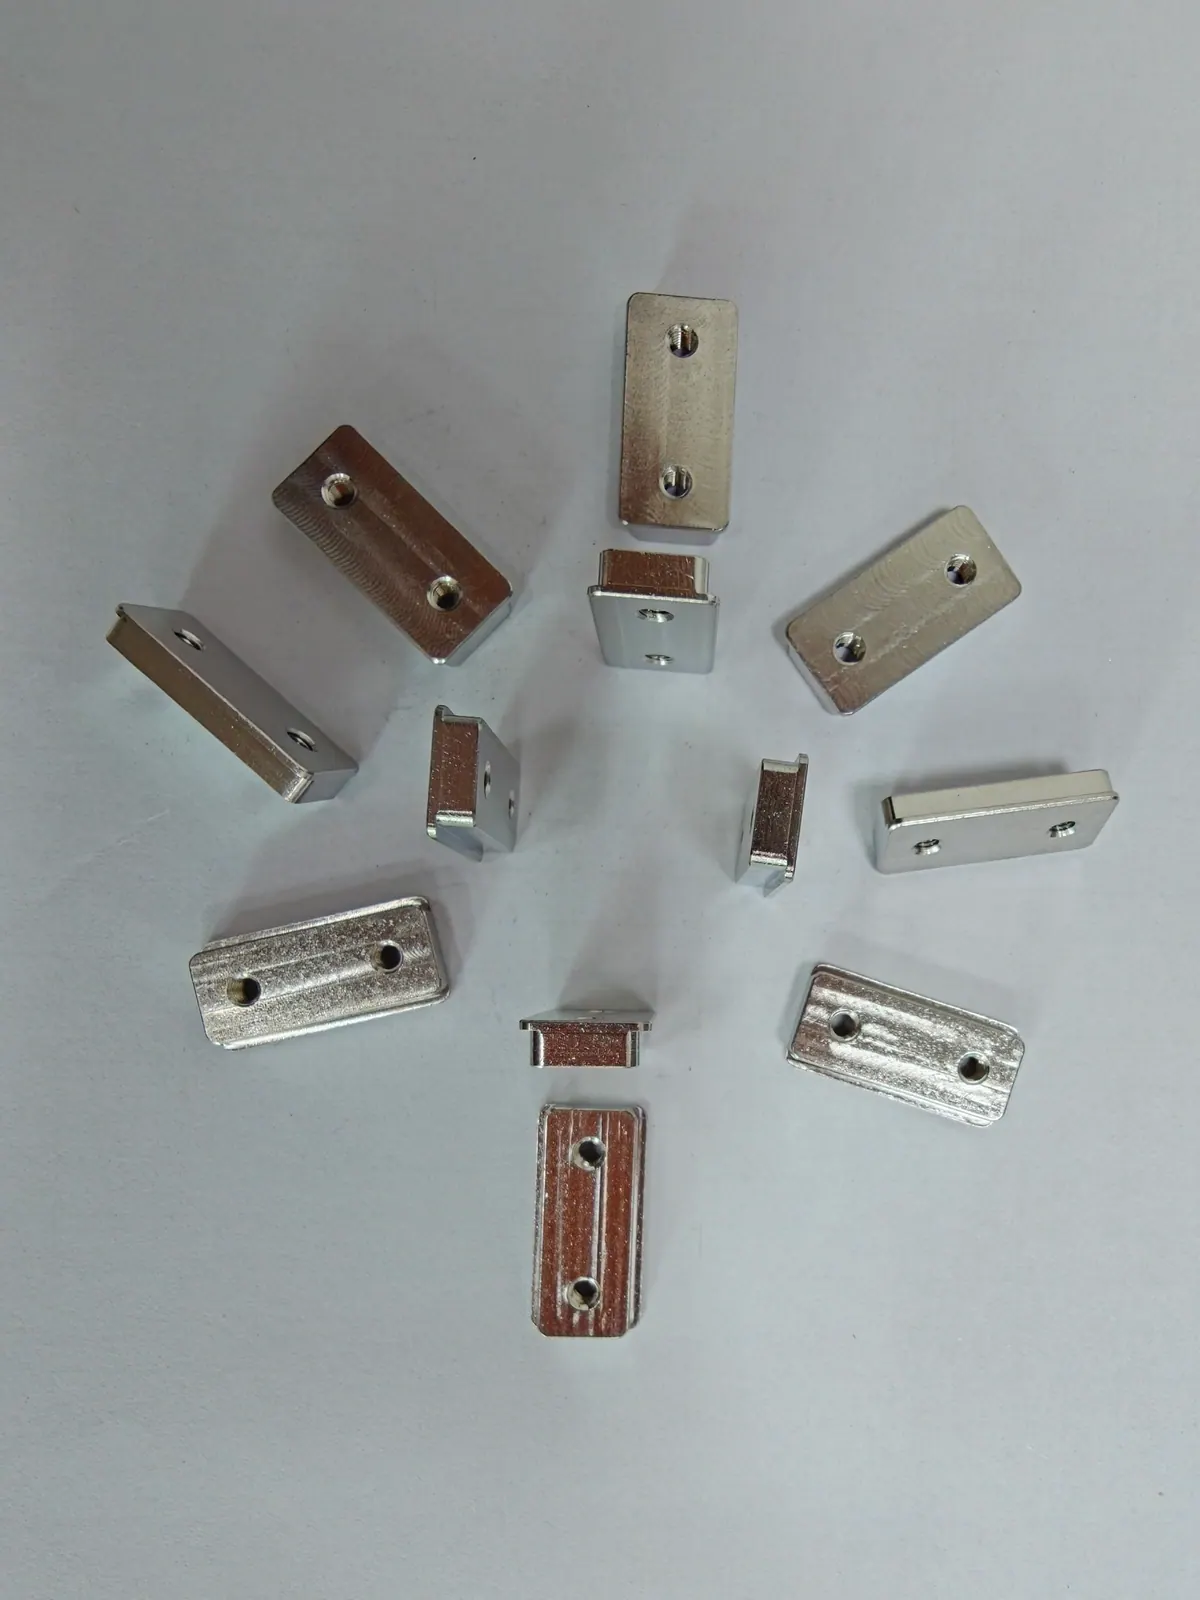
12 photographs
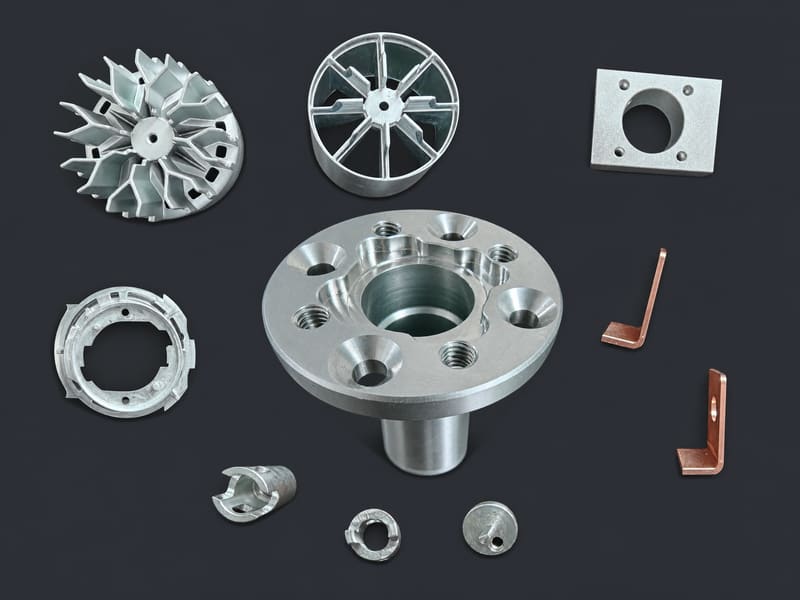
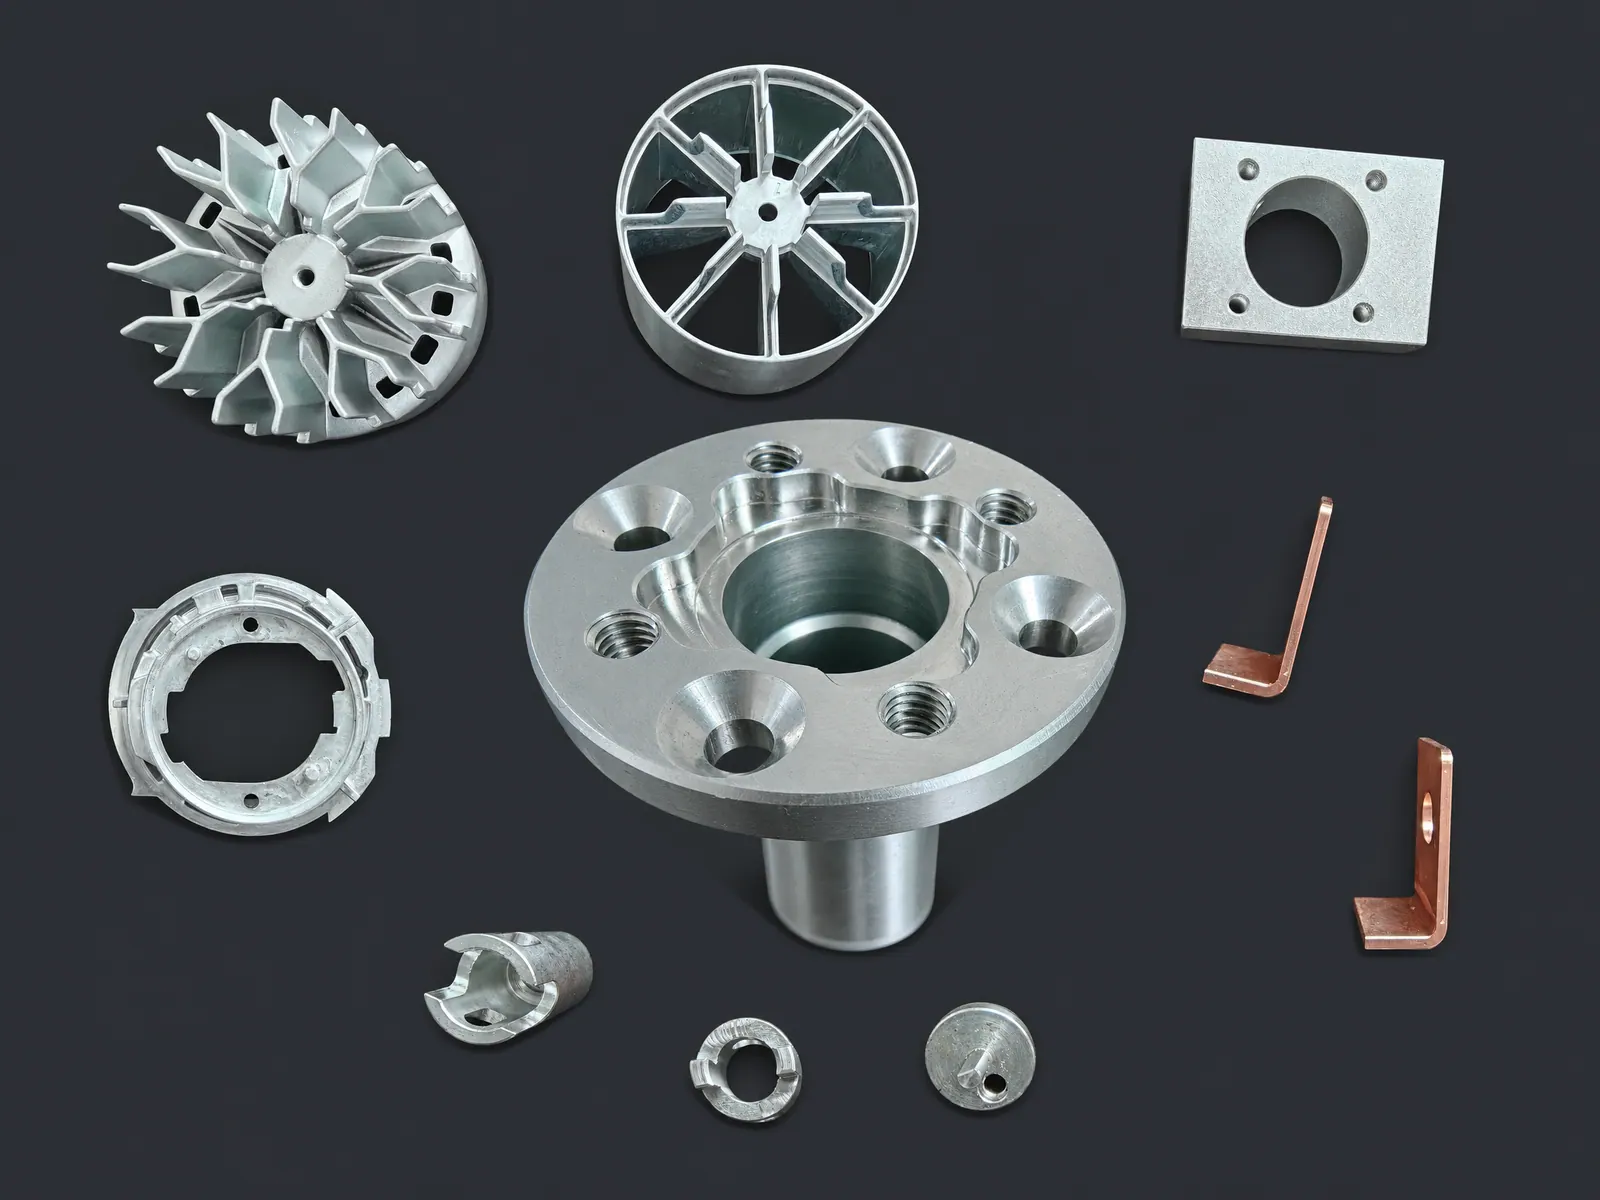
Flange, impeller, housings, block, small rings and bent copper brackets 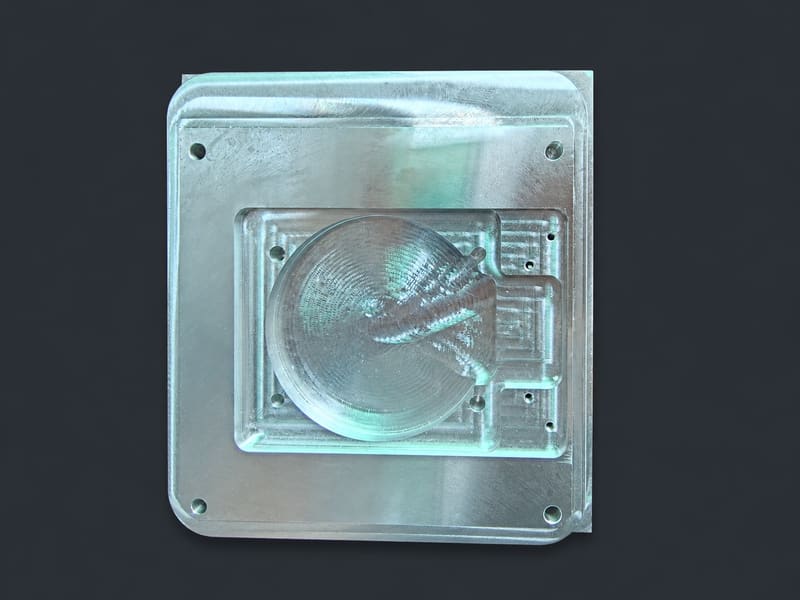
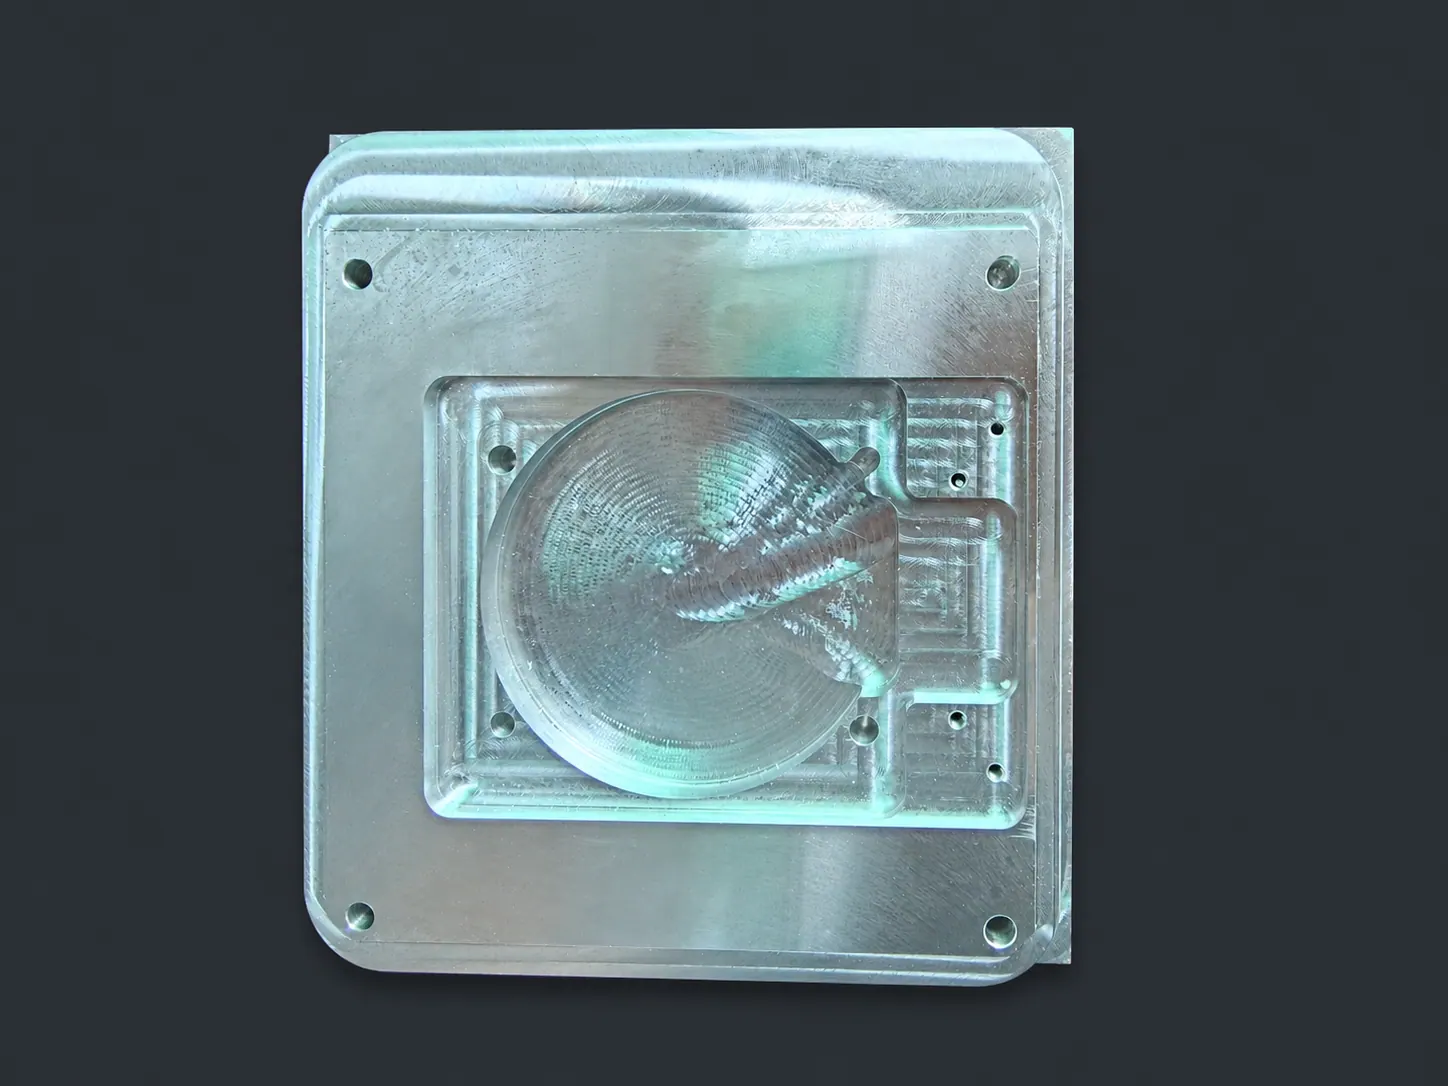
Plate with a stepped pocket and a dished surface 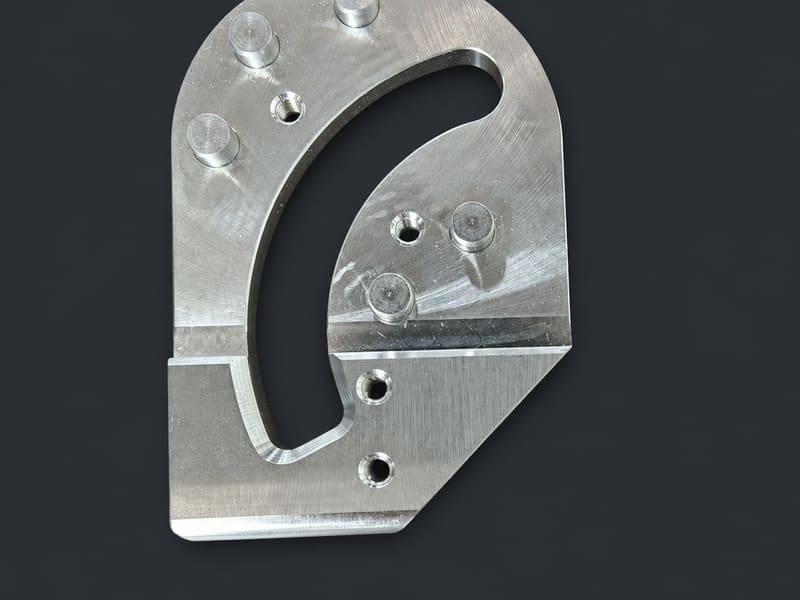
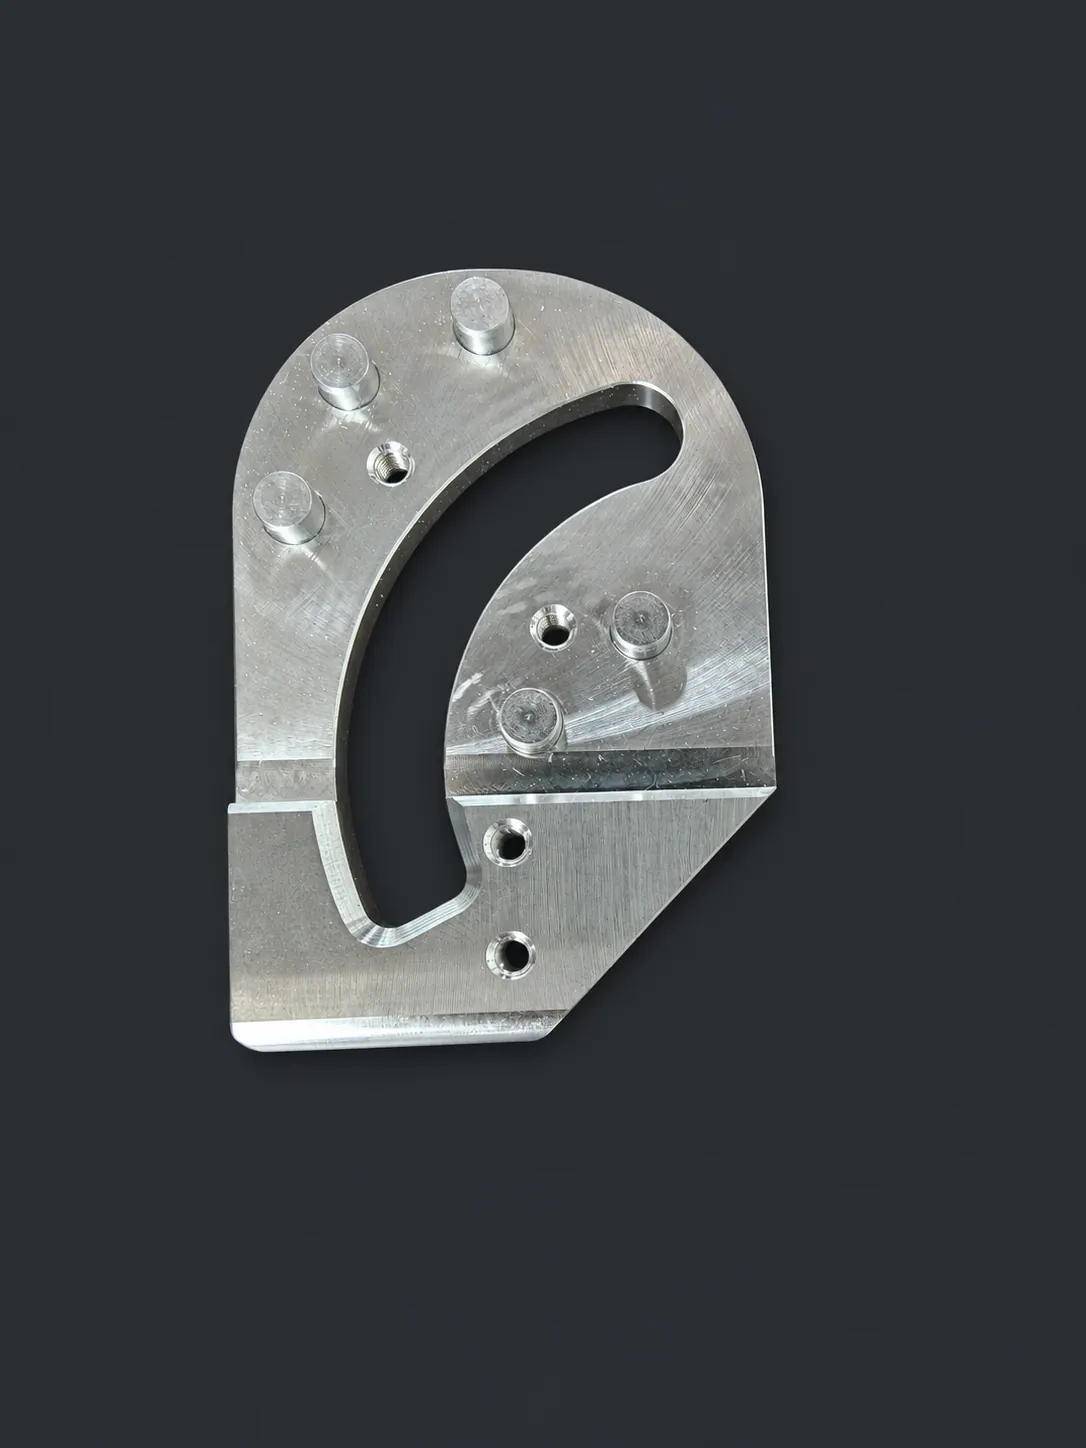
Locating plate with an arc slot and pressed-in dowel pins 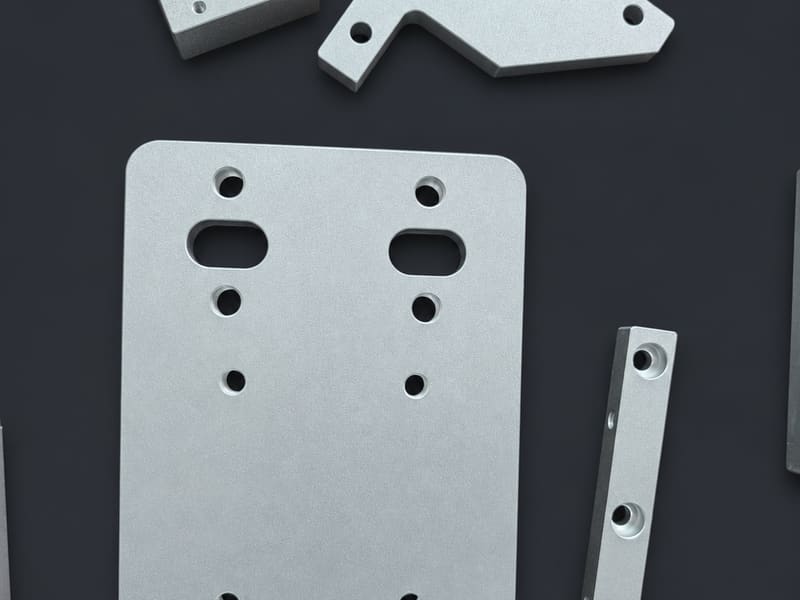
Plate, angle bracket, bar and a block with a bore and tapped holes 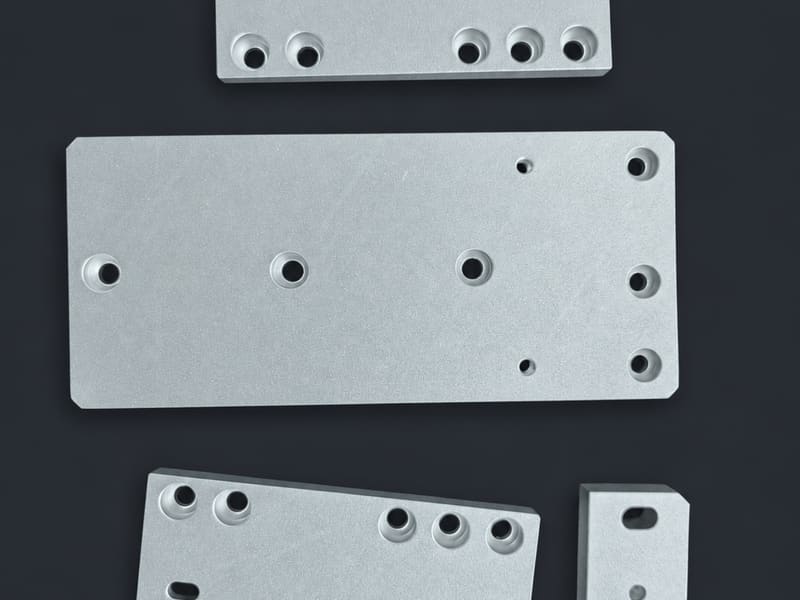
Four plates with slots, counterbored holes and chamfers 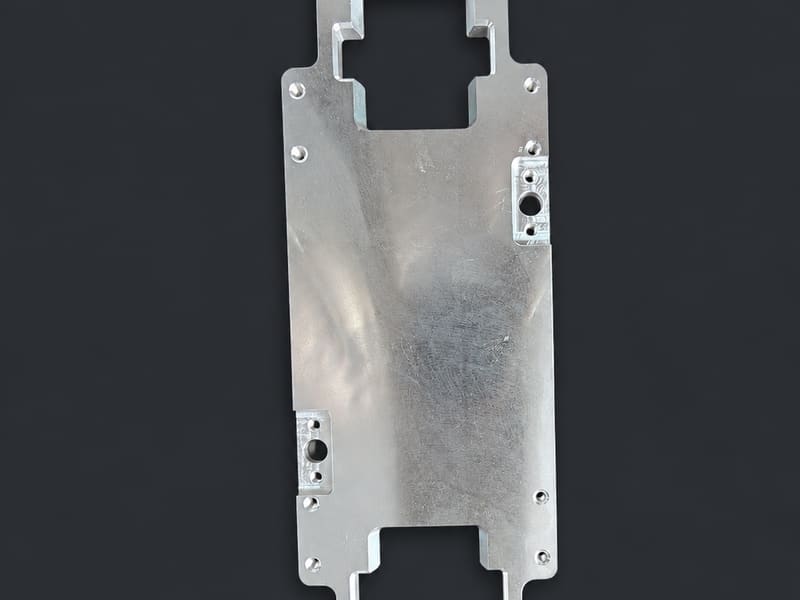
Long plate with two windows and counterbored bosses 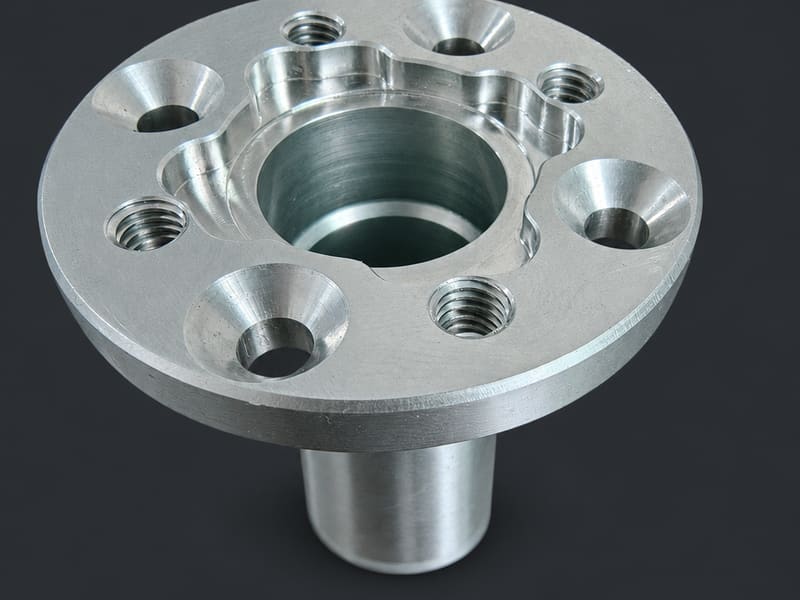
Stepped flange with counterbored and tapped holes 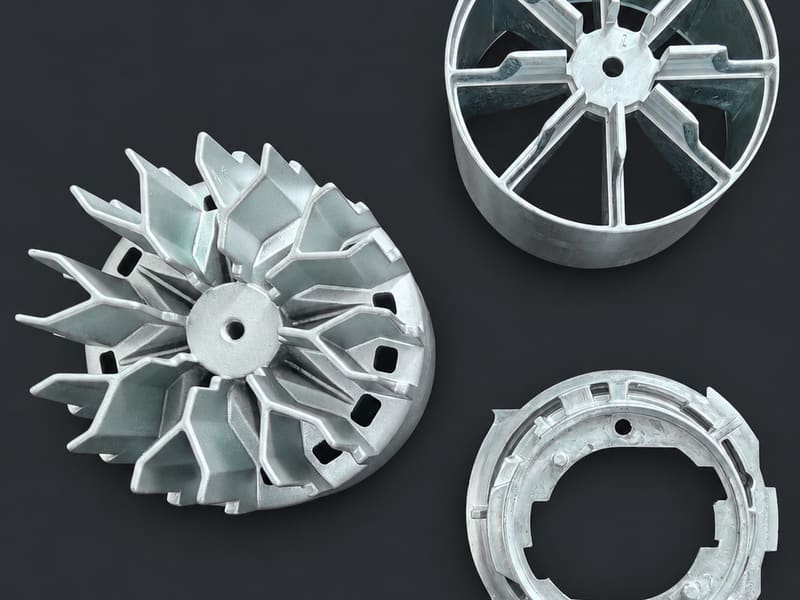
Impeller, ribbed sleeve and ring housing, machined from castings 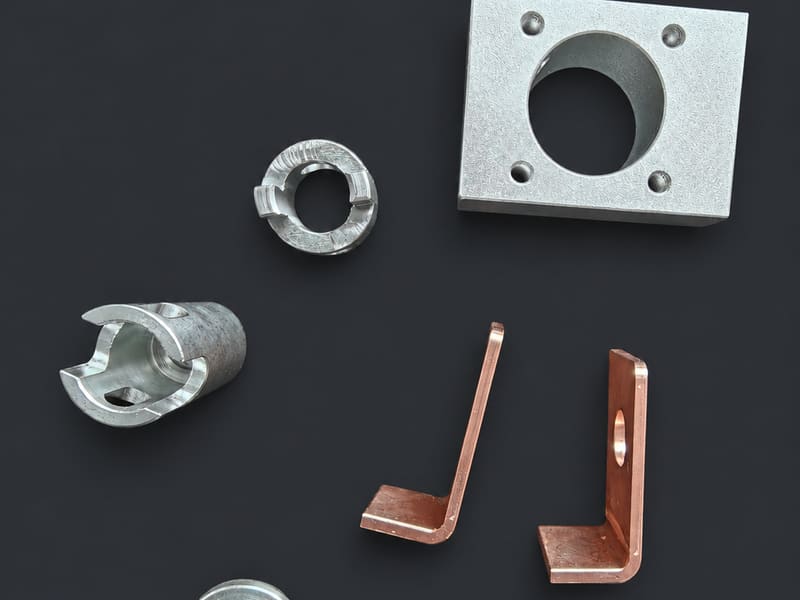
Block, slotted rings, cap and bent copper brackets 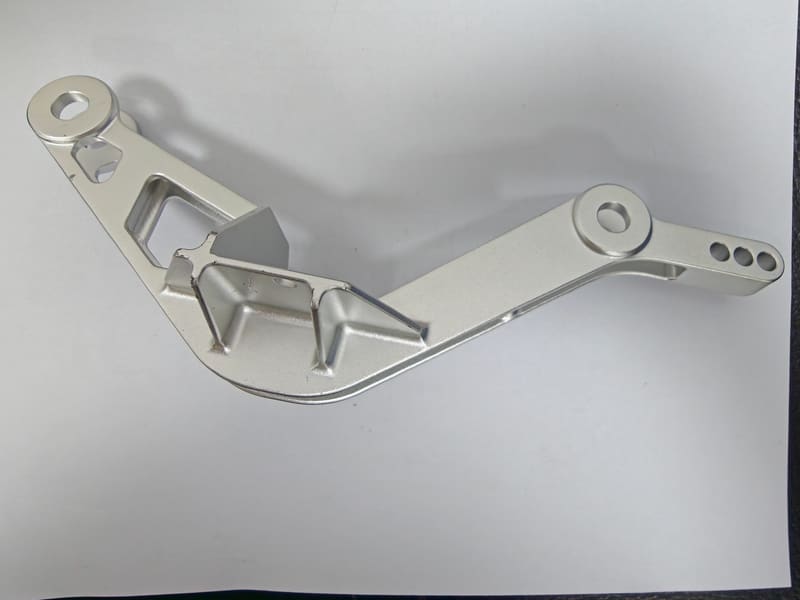
Arm with pockets, ribs and bores 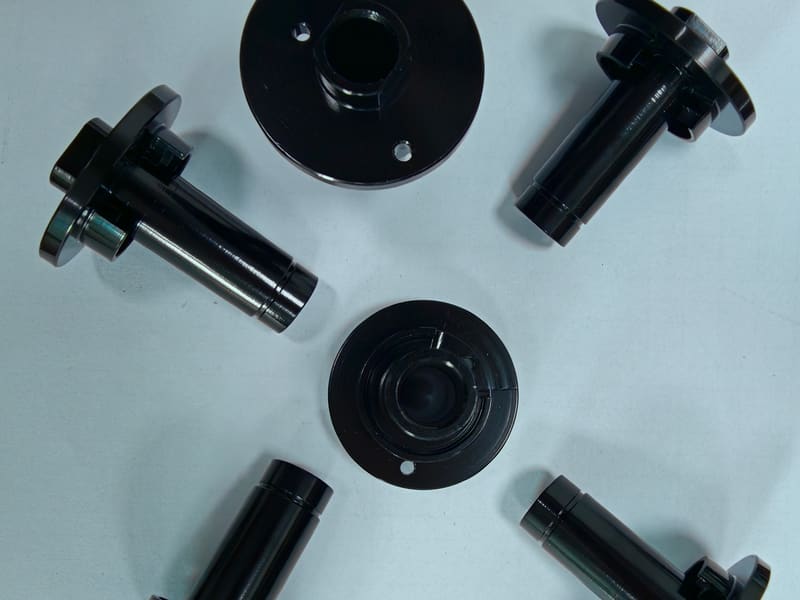
Flanged shafts and hubs 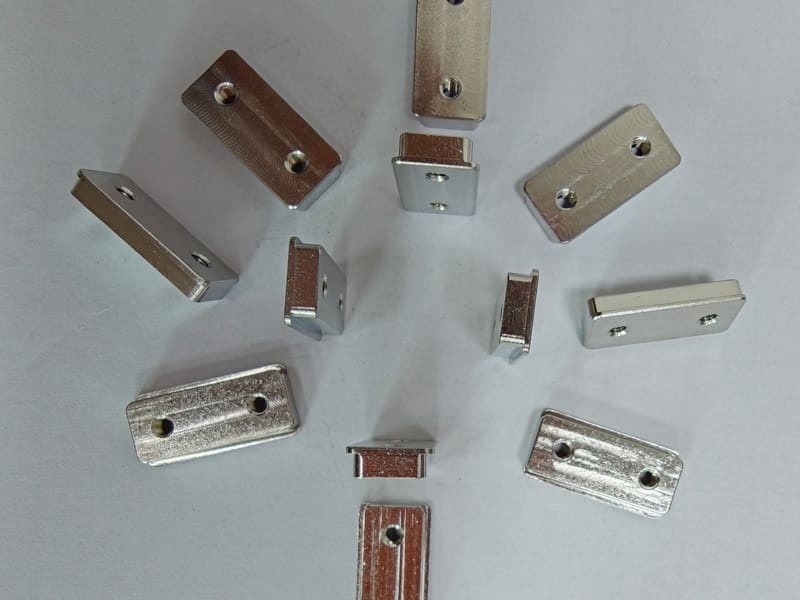
Small blocks and brackets with slots and holes
WILL IT FIT
Part envelope
Drawn to scale from the published maximum size.
View from above · X × Y
Not suited for
- Parts larger than the work range of the machines
Check a part against these limits
Results
1 process with published size limits
- CNC-MCNC milling
Up to 600 × 600 mmSource: Max sizeMax size600 × 600 mmBasisDeclaredAs ofSourceSupplier information form (owner), 2026-11How we label numbers
PRECISION
Tolerances
Tighter than the general tolerance adds inspection. Tighter than the best is not offered.
- Best ±0.01 mmSource: Best toleranceConditionsmany features, not only hole positions; measured hole positions are typically 0.02 mmBest tolerance±0.01 mmBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers, on requestmany features, not only hole positions; measured hole positions are typically 0.02 mm
- Tighter than ±0.01 mm: not offered
DRAWING RULES
Design rules
3 rules for CNC milling drawings
- Keep inside corner radii at least one third of the pocket depth.
- Avoid deep, narrow pockets: a depth of more than four times the width needs special tooling.
- Call out only the tolerances that matter. Everything else follows the general tolerance.
DATASHEET
The full datasheet.
Specification, equipment, terms and questions, folded until you need them.
Specification5 materials · 8 finishes, 8 by partner suppliers
CNC milling
CNC-M- Best tolerance
- ±0.01 mmNote 2Conditionsmany features, not only hole positions; measured hole positions are typically 0.02 mmBest tolerance±0.01 mmBasisDeclaredAs ofSourceOwner, 2026-11How we label numbersmany features, not only hole positions; measured hole positions are typically 0.02 mm
Materials and finishes
- Materials
- Stainless steel
- Copper and brass
- Aluminium
- Iron
- Steels of all kinds, incl. spring and alloy steel
- Finishes
- ElectroplatingPartner
- E-coatingPartner
- DacrometPartner
- Spray paintingPartner
- Powder coatingPartner
- AnodizingPartner
- PVDPartner
- Laser engravingPartner
Equipment1 models · 15 machines
| Type | Model | Qty | Key capacity |
|---|---|---|---|
| CNC milling machine | T6 | 15 | Work range (X × Y) 600 × 600 mm |
| Total: 15Note 3Machines for the process15BasisDocumentAs ofSourceSupplier information form: 15 machines listed for this processAsk for this recordHow we label numbers machines for this process | |||
Lead times and termsEvery part is quoted from its drawing
- Prototype lead time
- 10 daysNote 4Prototype lead time10 daysBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers
- Production lead time
- 15–20 daysNote 5Production lead time15–20 daysBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers
- Incoterms
- EXW Dongguan and FOB Shenzhen
Questions2 questions about CNC milling and orders
What tolerances can you hold?
Our best is ±0.01 mm in CNC milling (many features, not only hole positions; measured hole positions are typically 0.02 mm). Where the drawing gives no tolerance, the general tolerance of the process applies. Each capability page lists it.
How fast can I get prototypes?
The sample lead time is listed on the ordering page. It depends on the part and is confirmed in the quote.
Quote a CNC milling part
Amy
International Sales Manager
Phone and email: English and Chinese
Lu Dadong
General Manager
Drawings and technical questions
Phone: Chinese · Email: English and Chinese
Sources
Every figure on this page, with its source and date.
- Max size: 600 × 600 mm. Source: Supplier information form (owner), 2026-11; as of 6 November 2026.
- Best tolerance (many features, not only hole positions; measured hole positions are typically 0.02 mm): ±0.01 mm. Source: Owner, 2026-11; as of 6 November 2026.
- Machines for the process: 15. Source: Supplier information form: 15 machines listed for this process; as of 6 November 2026.
- Prototype lead time: 10 days. Source: Owner, 2026-11; as of 6 November 2026.
- Production lead time: 15–20 days. Source: Owner, 2026-11; as of 6 November 2026.
Data revised