PROCESS STP
Stamping and assembly
Stamping on presses from 45 to 600 tonnes and a 350-tonne hydraulic press; turned and stamped parts assembled in house.
- 38Machines for this processSource: Machines for the processMachines for the process38BasisDocumentAs ofSourceSupplier information form: 38 machines listed for this processAsk for this recordHow we label numbers
IN 3D
Turn the part. Check the dimensions.
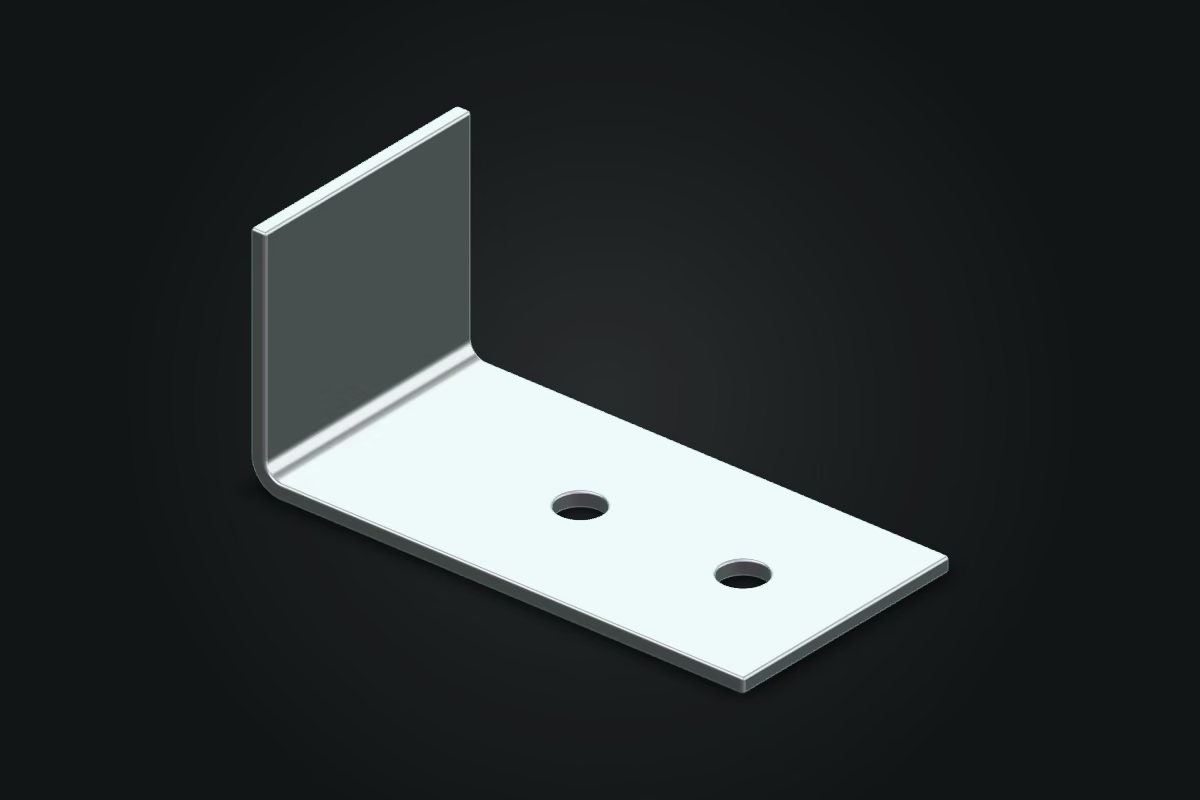
Stamped L-bracket: Cold-rolled steel, zinc plated.Drag or use the arrow keys to turn a part; select a feature to see its dimension.Swipe sideways to turn a part; tap a feature to see its dimension.Load the 3D view to turn a part and select a feature on it.Select a part to see its drawing and key features.
Rendered illustration, not a photograph of a delivered part. Geometry from showcase data.
Stamped L-bracket
- Process
- Metal stamping
- Material
- Cold-rolled steel
- Finish
- Zinc plated
Key features
- Mounting holeØ6.6 mm±0.05 mm
- Bend angle90°±0.5°
- Material thickness2.5 mm±0.05 mm
Values from the sample part drawing.
Arrow keys turn the part. Home resets the view. Number keys select a feature.
HOW IT IS MADE
How a stamped part is made
The strip moves one station per stroke: the die pierces the holes, bends the leg and cuts the finished bracket off.
Illustration
THE PART
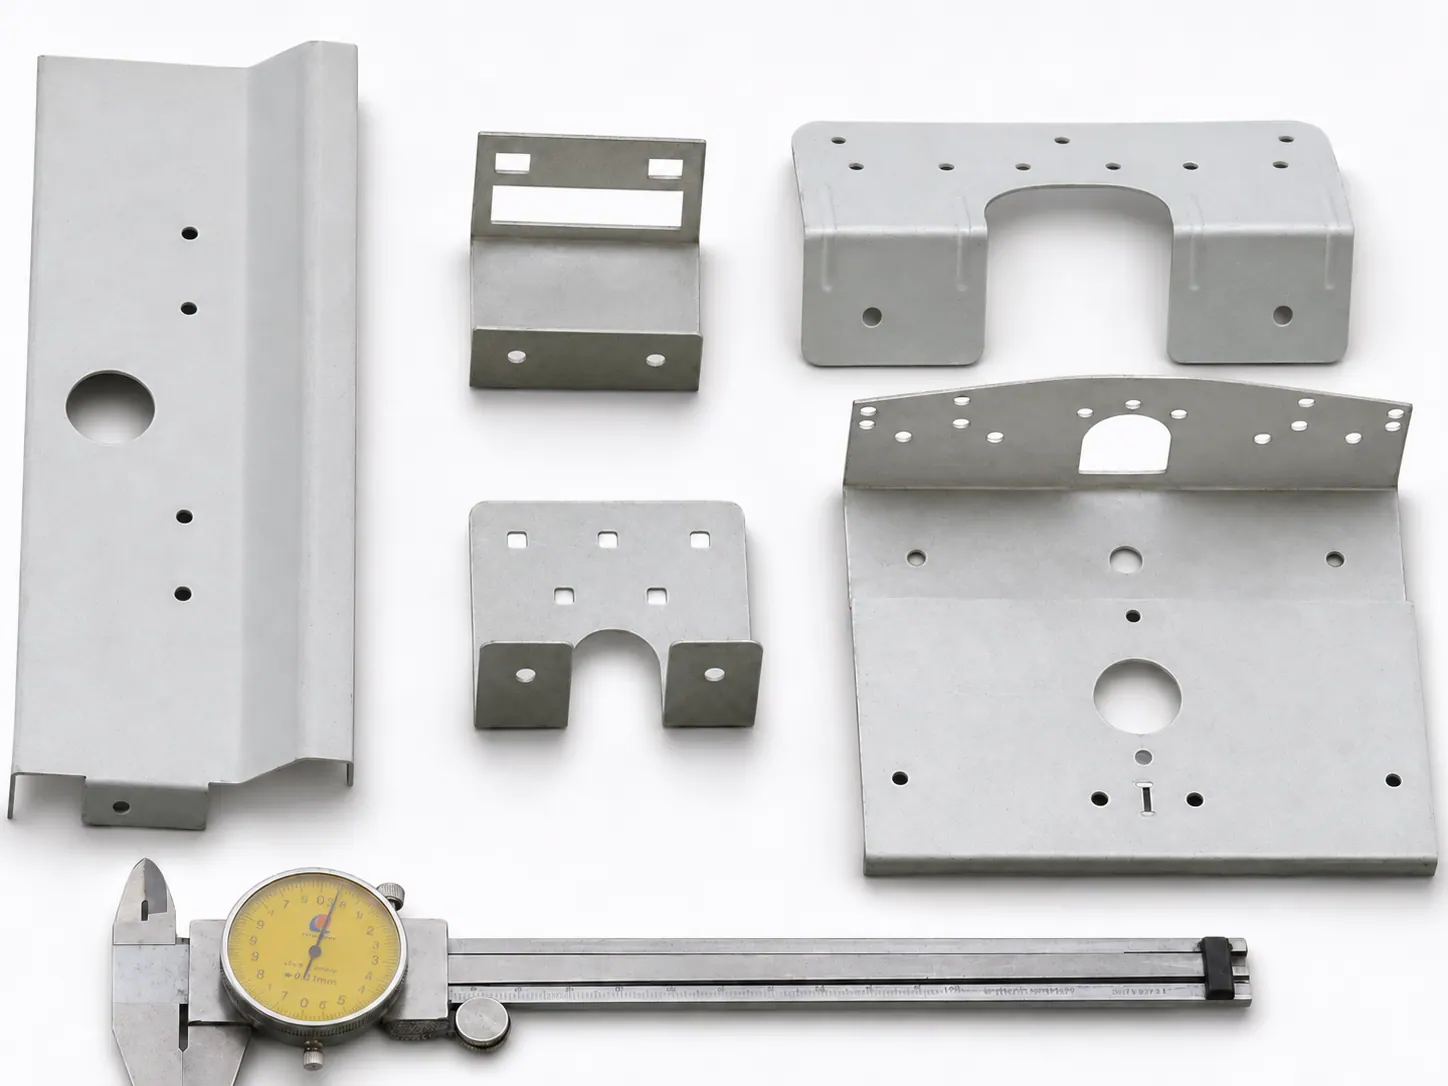
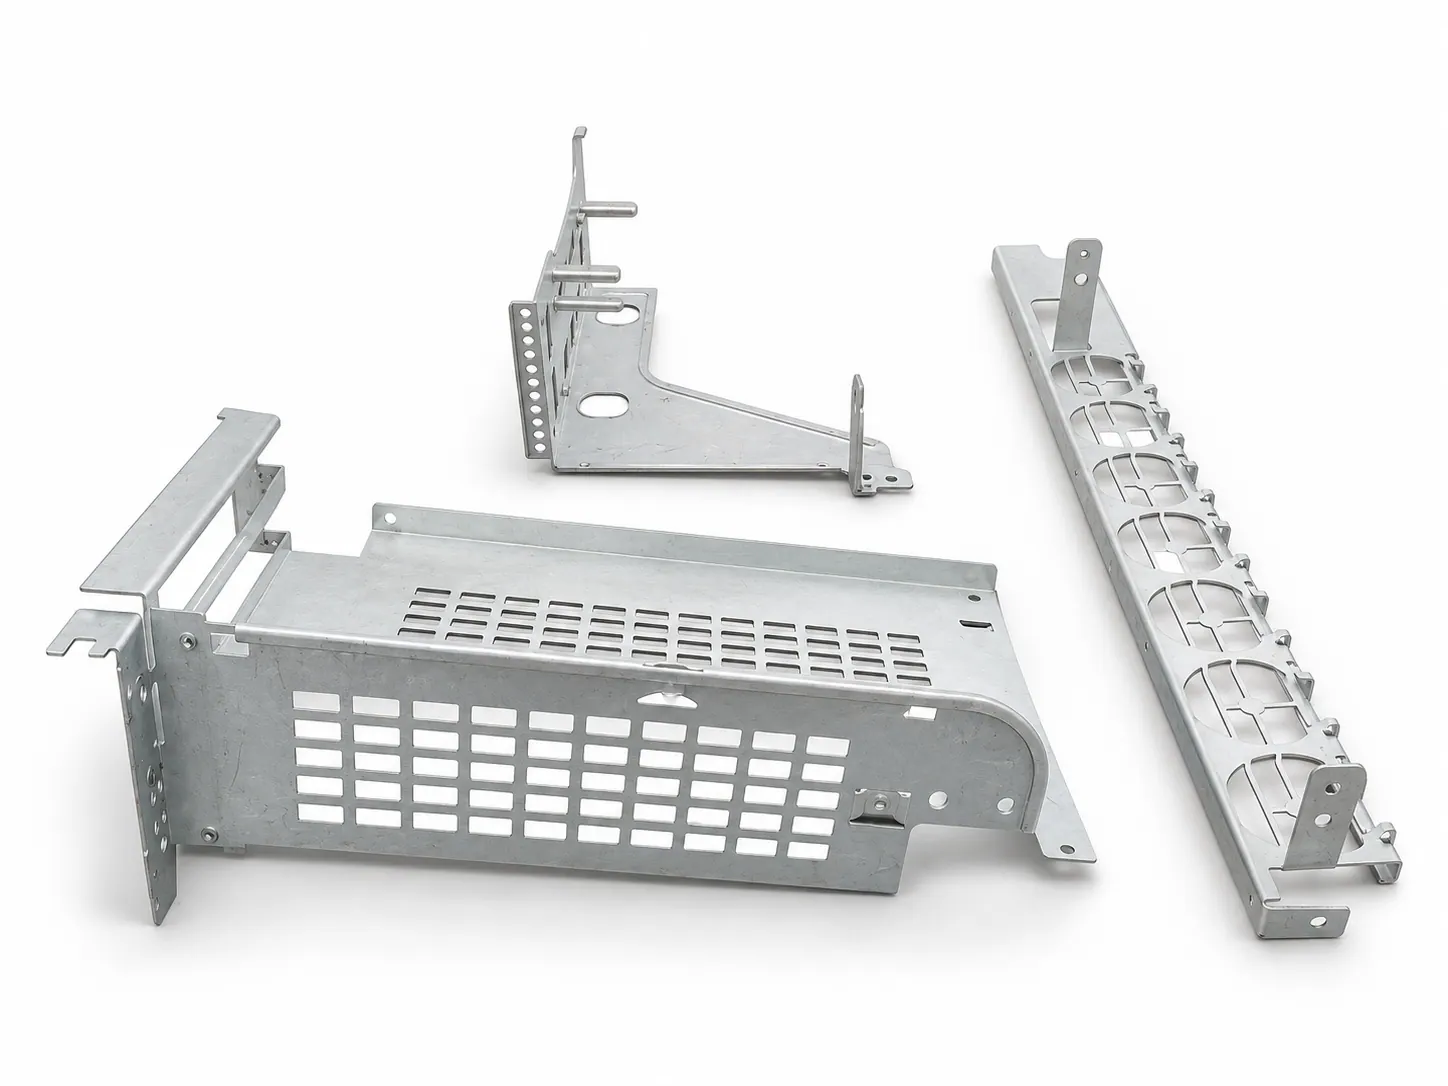
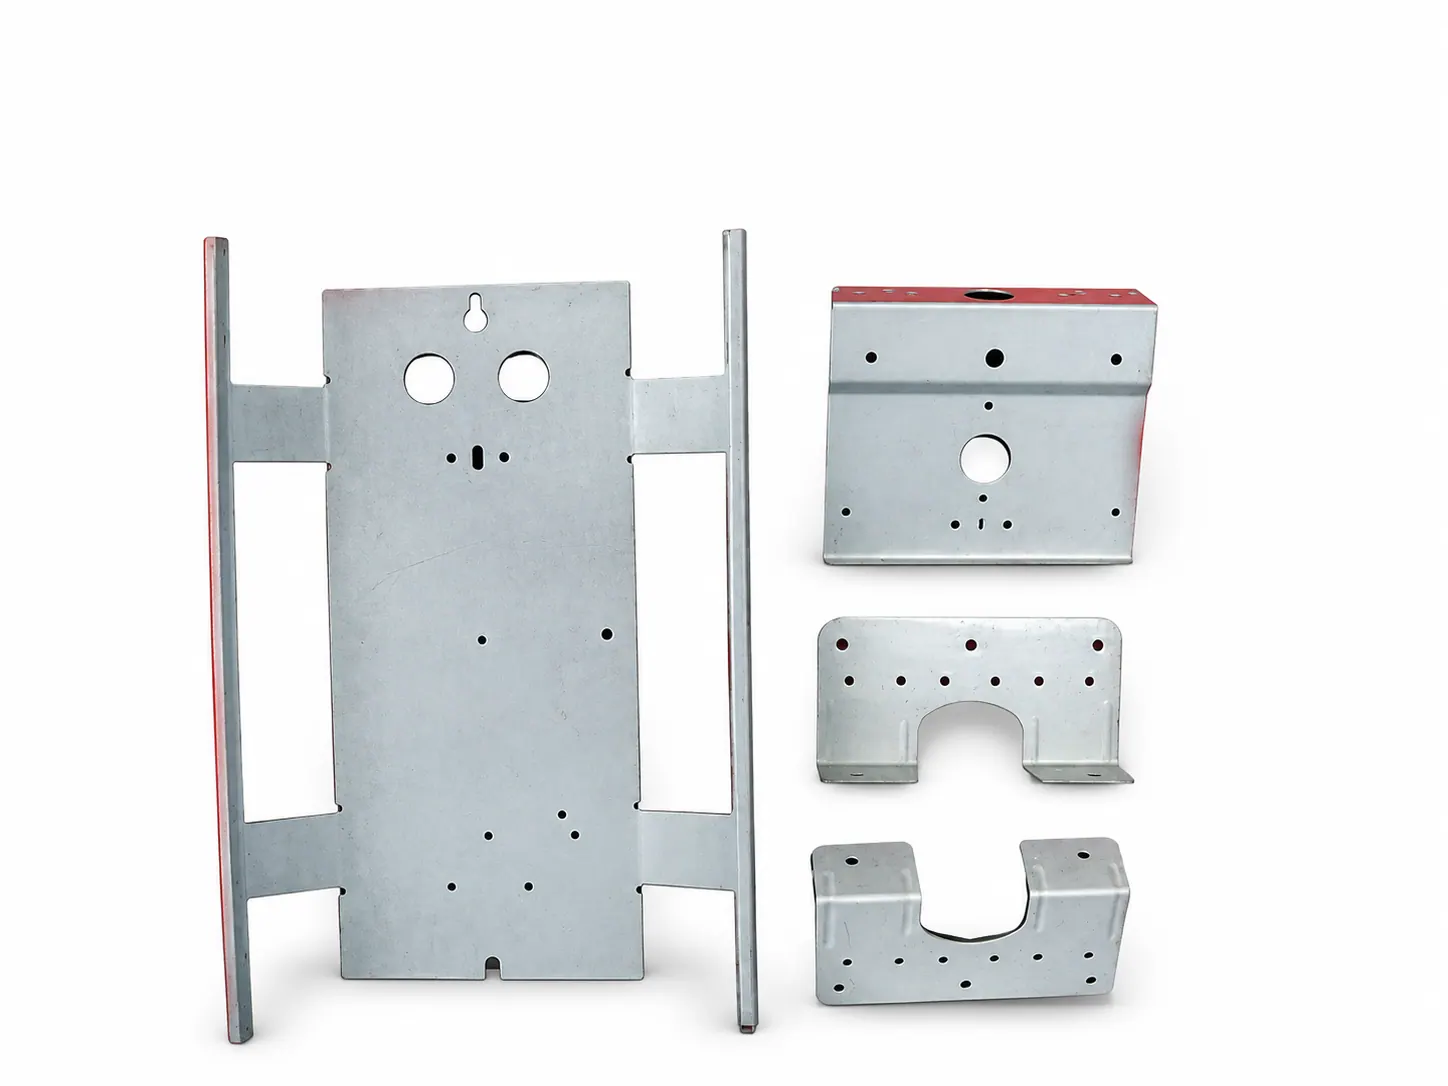
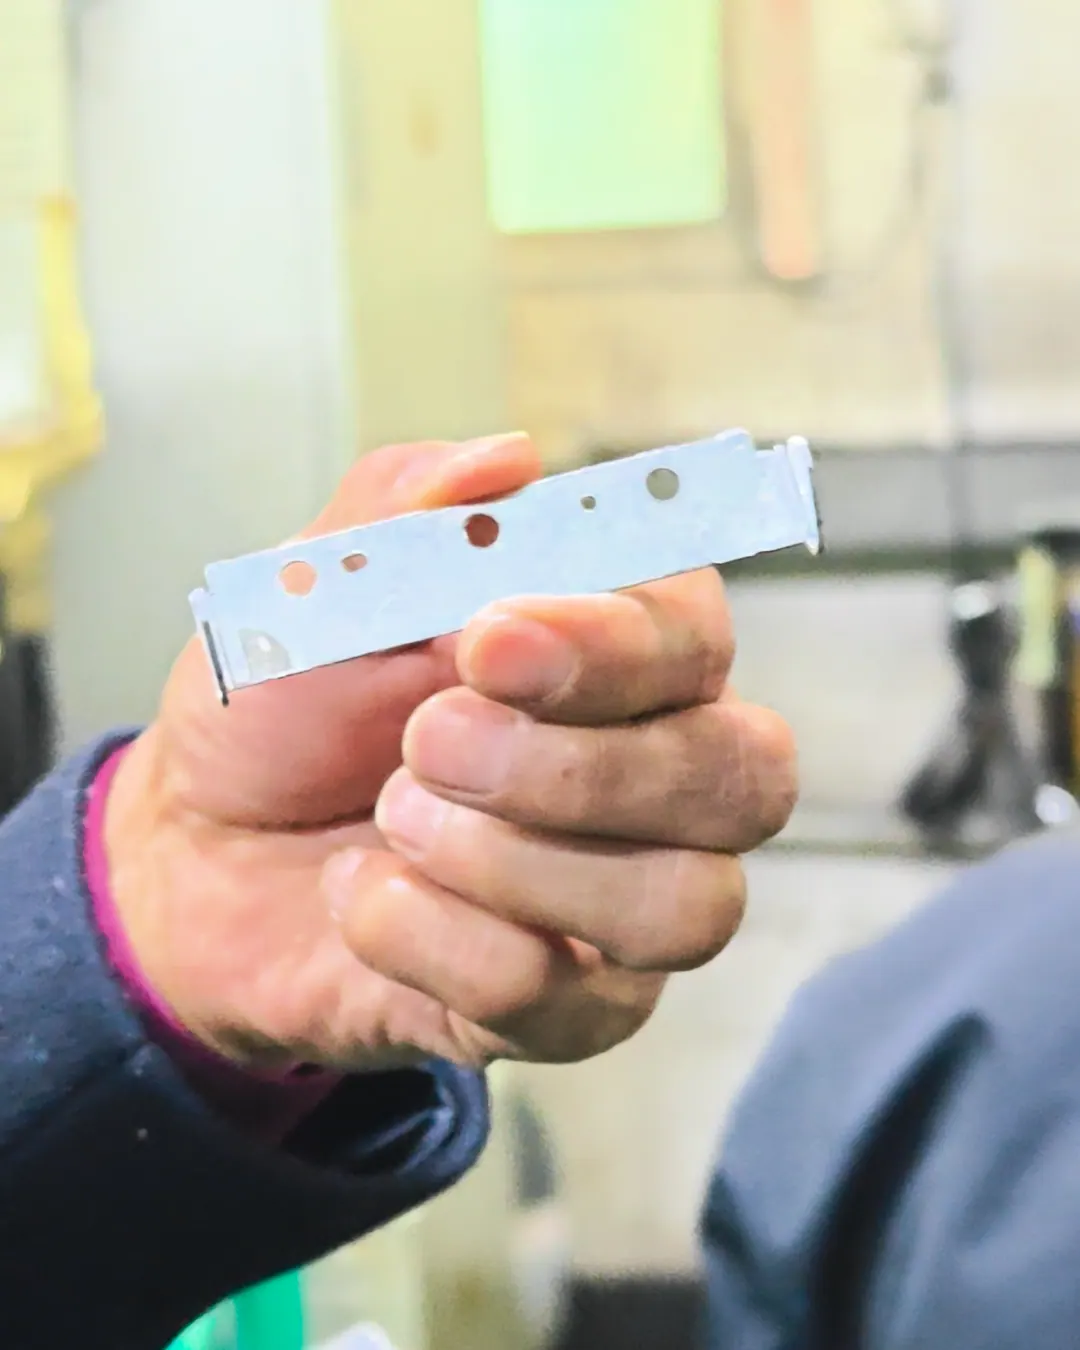
Sample parts
8 photographs
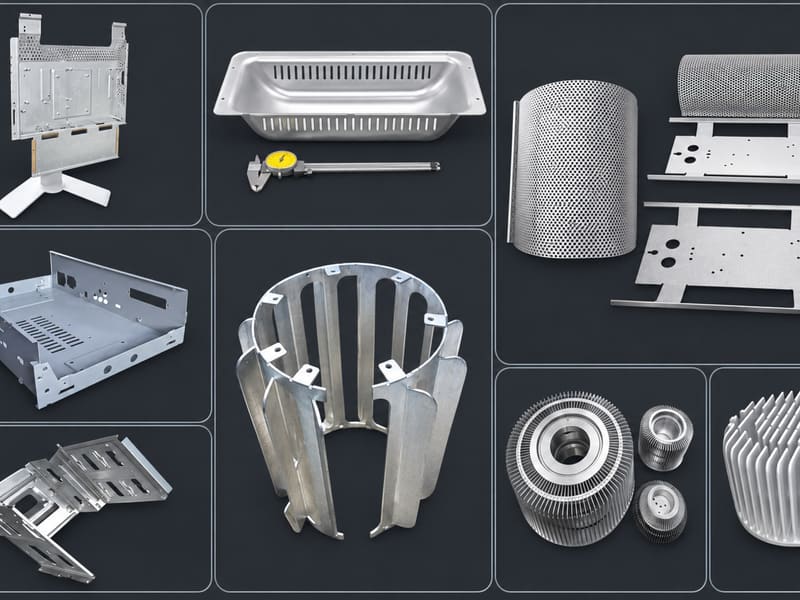
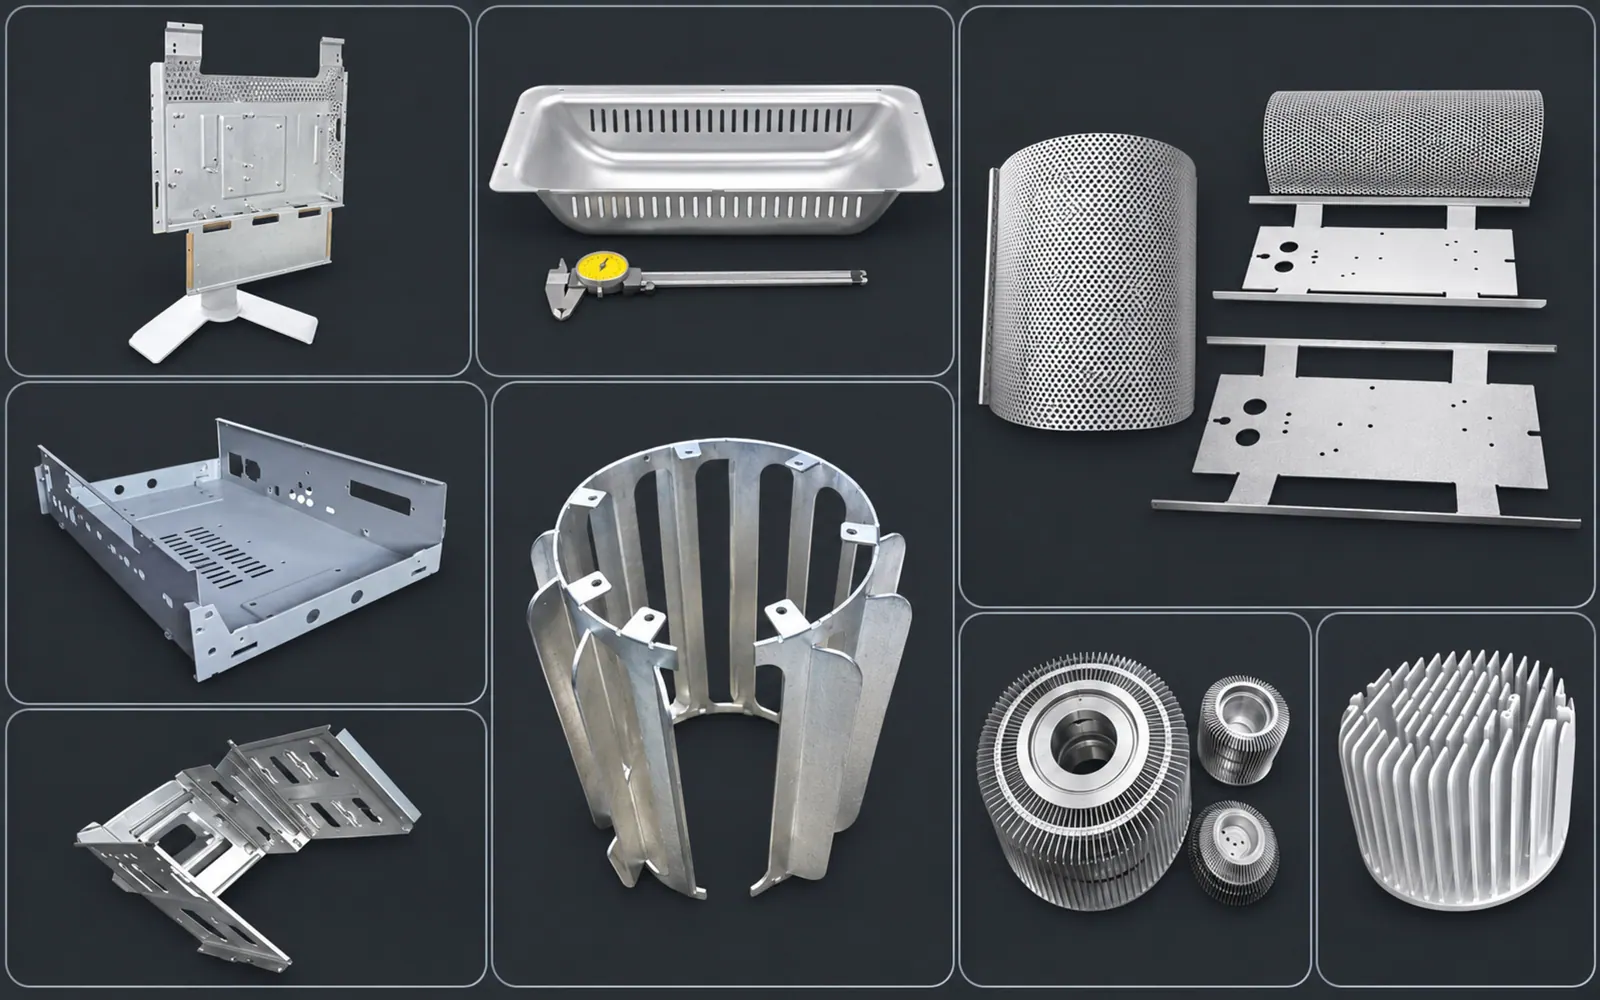
Sheet-metal enclosures, perforated parts, a bent bracket and heatsinks 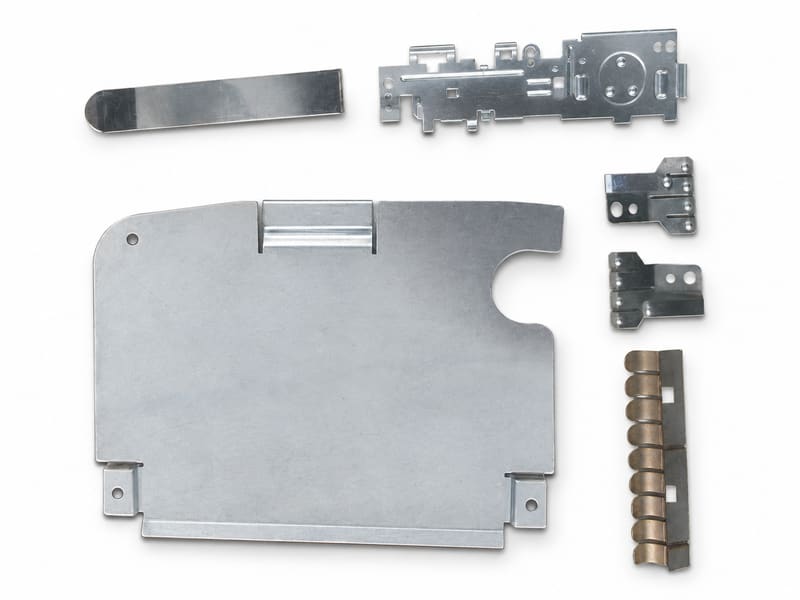
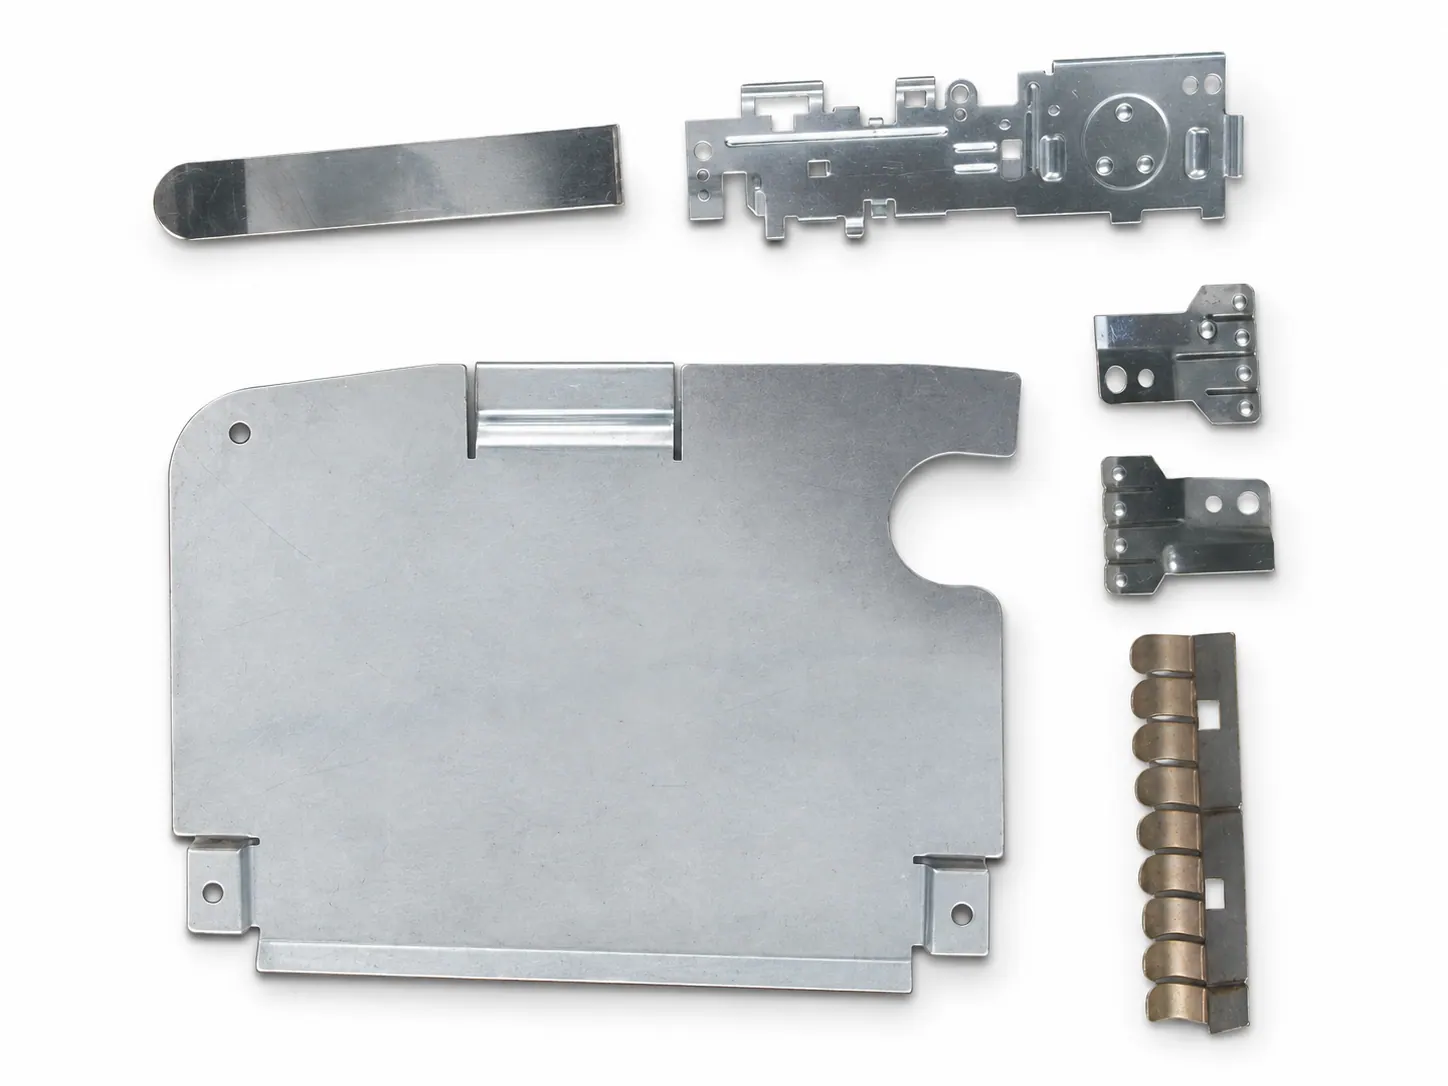
Six sheet-metal parts: a large plate, brackets and strips 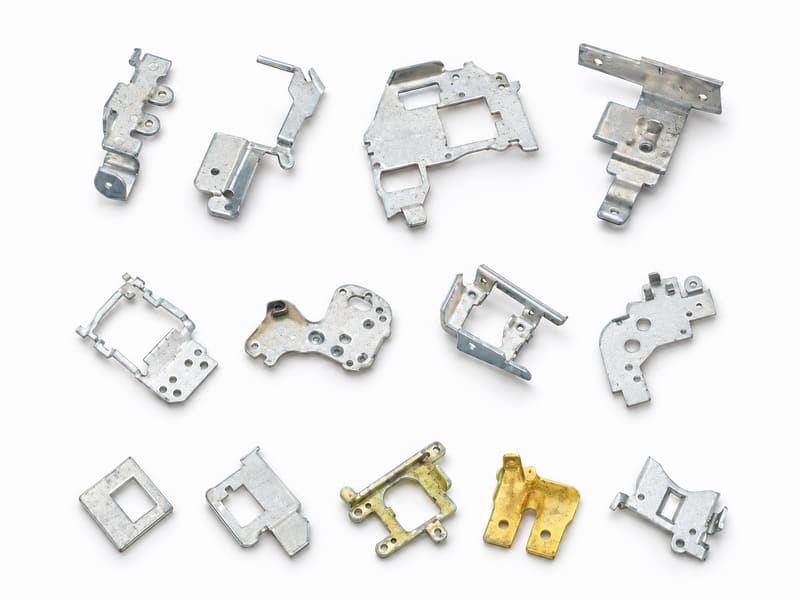
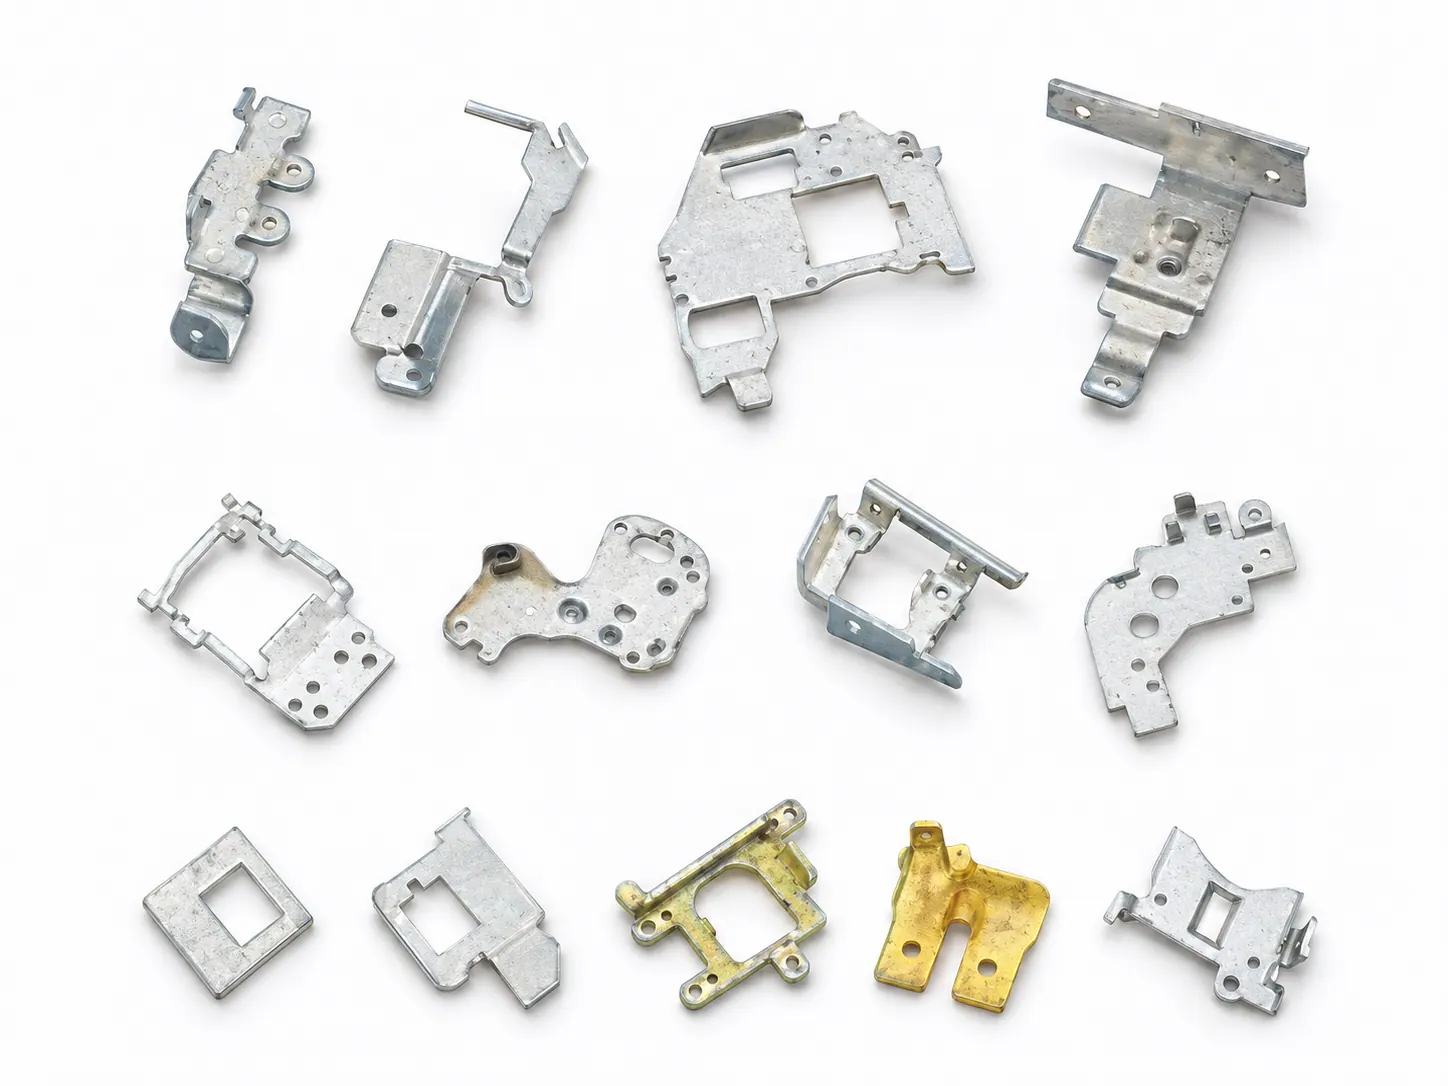
Thirteen small stamped parts: bent brackets and frames 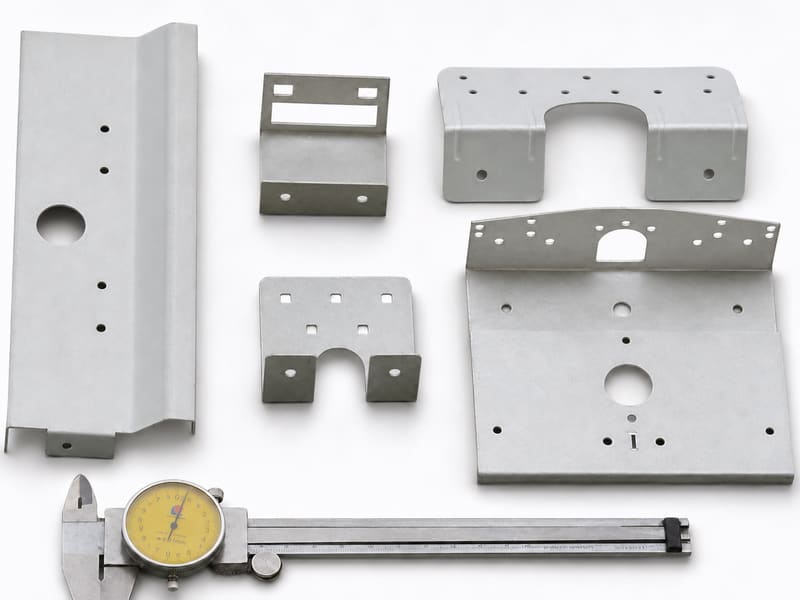
Bent sheet-metal parts with a dial caliper 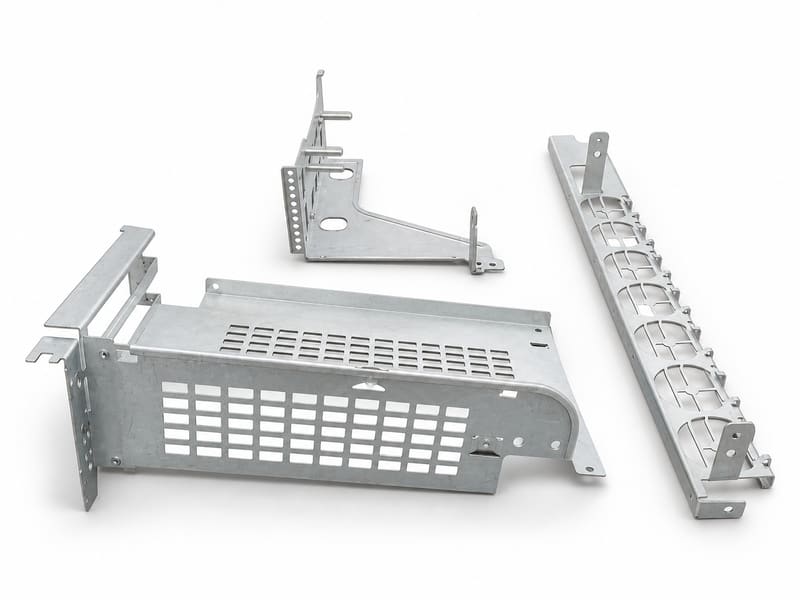
Three perforated sheet-metal chassis parts 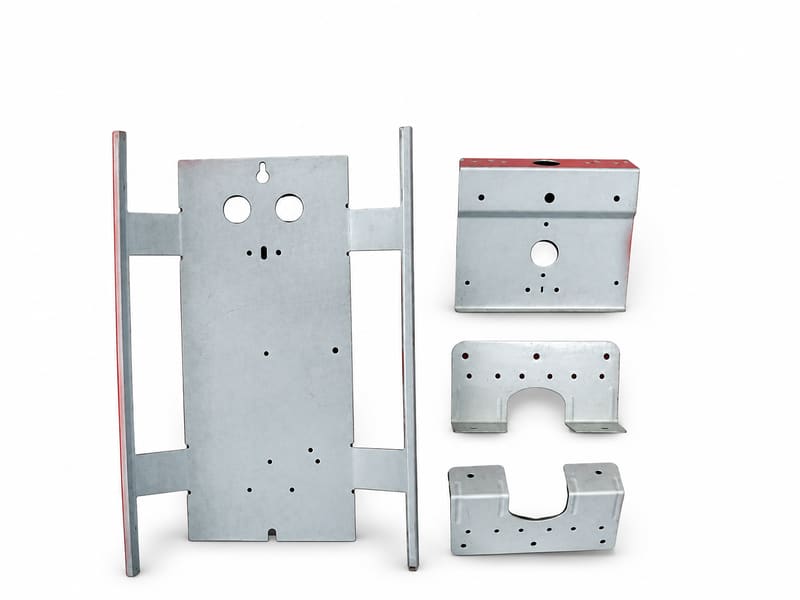
Four sheet-metal parts: a long plate with side rails and three brackets 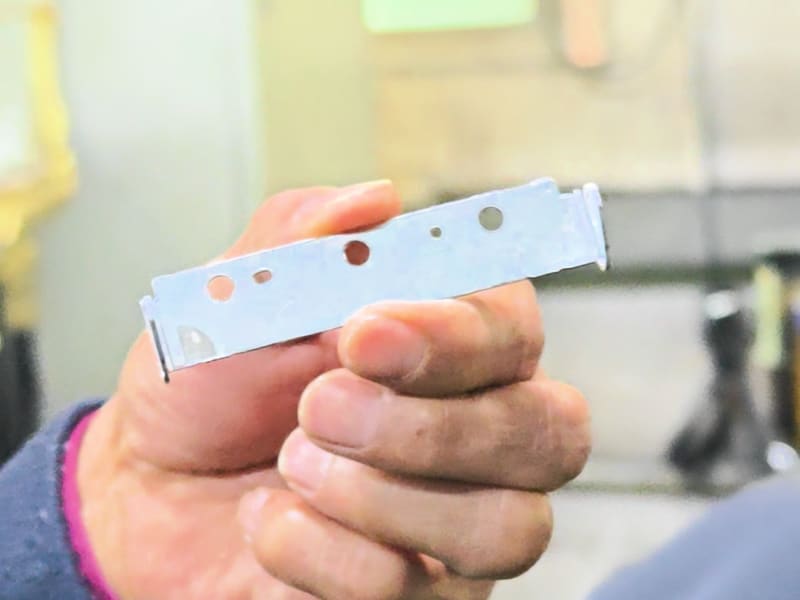
Stamped bracket with a row of holes and bent ends 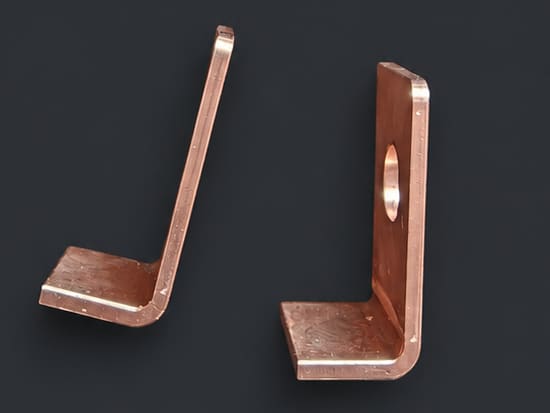
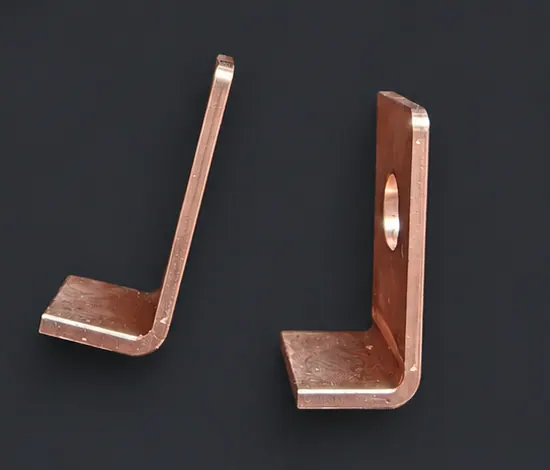
Bent copper brackets with holes
WILL IT FIT
Part envelope
Stamping and assembly has no envelope of its own: it applies to any part we make.
DRAWING RULES
Design rules
3 rules for stamping and assembly drawings
- Keep hole diameter at least equal to the material thickness.
- Place holes at least 1.5 times the thickness away from any bend line.
- Allow a bend relief wherever a bend meets a flat edge.
DATASHEET
The full datasheet.
Specification, equipment, terms and questions, folded until you need them.
Specification5 materials · 8 finishes, 8 by partner suppliers
Materials and finishes
- Materials
- Stainless steel
- Copper and brass
- Aluminium
- Iron
- Steels of all kinds, incl. spring and alloy steel
- Finishes
- ElectroplatingPartner
- E-coatingPartner
- DacrometPartner
- Spray paintingPartner
- Powder coatingPartner
- AnodizingPartner
- PVDPartner
- Laser engravingPartner
Equipment11 models · 38 machines
| Type | Model | Qty | Key capacity |
|---|---|---|---|
| Stamping press | 1 | Press force 600 t | |
| Hydraulic press | 1 | Press force 350 t | |
| Stamping press | 1 | Press force 315 t | |
| Stamping press | 2 | Press force 250 t | |
| Stamping press | 1 | Press force 200 t | |
| Stamping press | 3 | Press force 160 t | |
| Stamping press | 14 | Press force 110 t | |
| Stamping press | 3 | Press force 100 t | |
| Stamping press | 9 | Press force 80 t | |
| Stamping press | 3 | Press force 45 t | |
| Wire EDM machine | 10 | ||
| Total: 38Note 1Machines for the process38BasisDocumentAs ofSourceSupplier information form: 38 machines listed for this processAsk for this recordHow we label numbers machines for this processAlso 10 tool-room machines, not counted above. | |||
Lead times and termsEvery part is quoted from its drawing
- Prototype lead time
- 10 daysNote 2Prototype lead time10 daysBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers
- Production lead time
- 15–20 daysNote 3Production lead time15–20 daysBasisDeclaredAs ofSourceOwner, 2026-11How we label numbers
- Incoterms
- EXW Dongguan and FOB Shenzhen
Questions1 questions about stamping and assembly and orders
How fast can I get prototypes?
The sample lead time is listed on the ordering page. It depends on the part and is confirmed in the quote.
Quote a stamping and assembly part
Amy
International Sales Manager
Phone and email: English and Chinese
Lu Dadong
General Manager
Drawings and technical questions
Phone: Chinese · Email: English and Chinese
Sources
Every figure on this page, with its source and date.
- Machines for the process: 38. Source: Supplier information form: 38 machines listed for this process; as of 6 November 2026.
- Prototype lead time: 10 days. Source: Owner, 2026-11; as of 6 November 2026.
- Production lead time: 15–20 days. Source: Owner, 2026-11; as of 6 November 2026.
Data revised